Lead Time
From 48 hours for standard resin jobs

3Dプリント
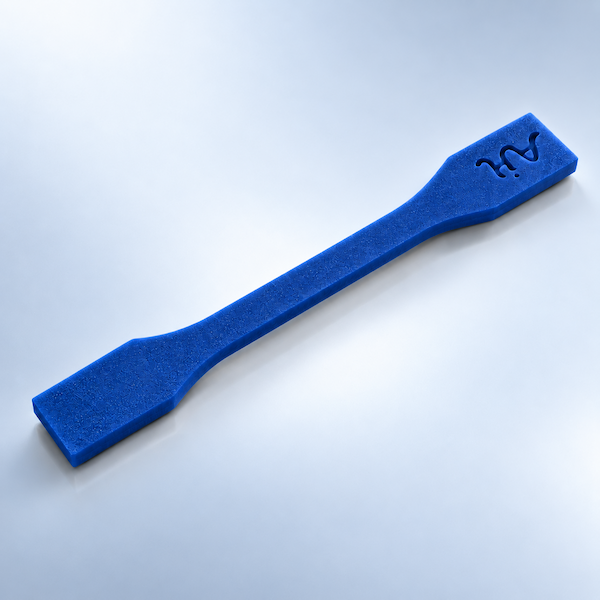
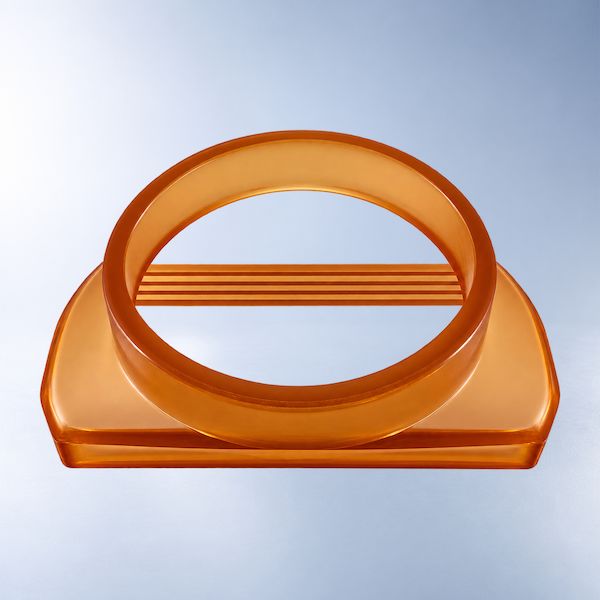
Ultra-smooth resin parts with fine feature resolution — show models, master patterns, and clear prototypes.
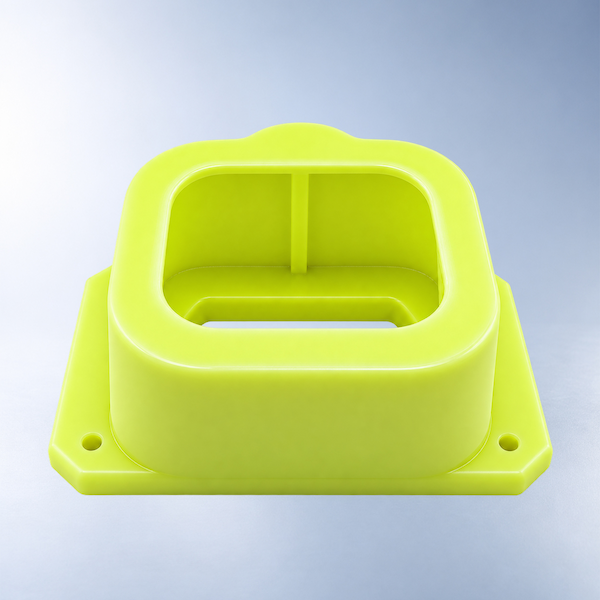
Stereolithography (SLA) cures liquid photopolymer with a precision UV laser, building parts layer by layer. SLA excels when surface quality, small features, and dimensional accuracy matter more than rugged thermoplastic performance. Plan around ±0.2 mm on well-supported features and from 48 hours on standard resin — the live quote after CAD upload is the source of truth.
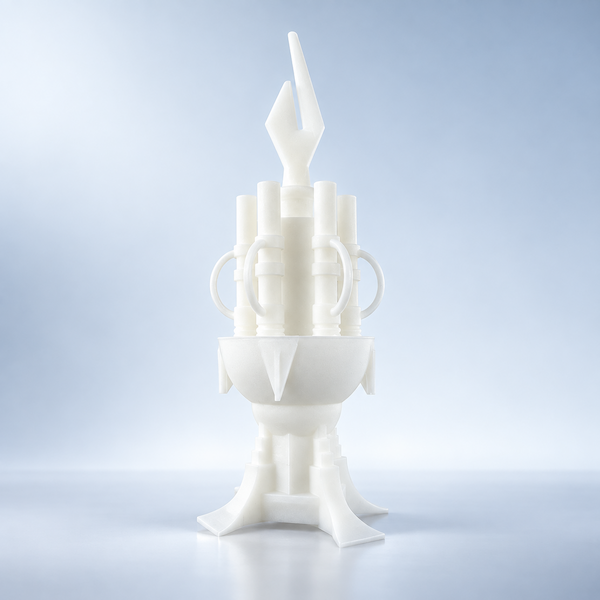
Check SLA capabilities, pick a resin, then upload STL or STEP. Compare DLP or LCD for faster full-layer resin, SLS nylon for shop handling, and 3D Plus finishing for paint or clear coat.
Stereolithography draws each slice with a UV laser in a vat of liquid resin. The cured layer bonds to the one below, which is why SLA parts look closer to a molded show model than to a filament print.
AIHFABS uses SLA when edges, lettering, and smooth skins matter more than rugged nylon toughness. Supports touch the part, so cosmetic faces should be called out before we orient the build.
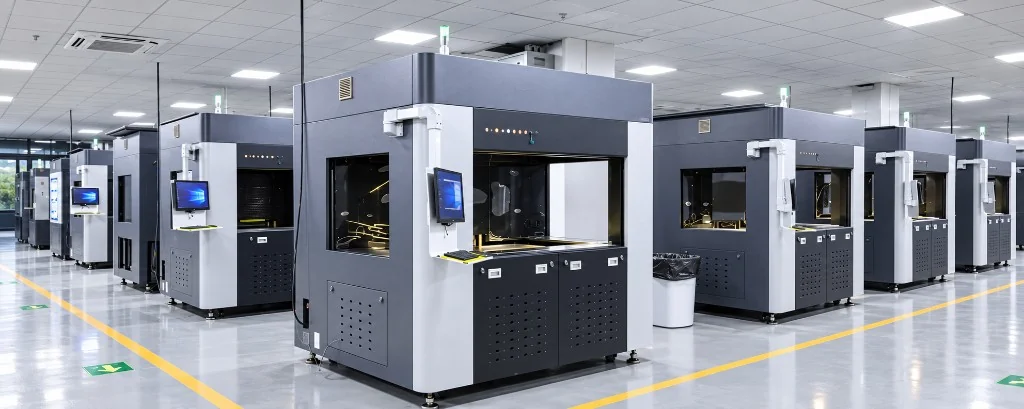
Fine layers and a large platform are available; the live quote still depends on orientation and resin.
From 48 hours for standard resin jobs
±0.2 mm on well-supported features
Platform up to 800 × 800 × 550 mm (job dependent)
Fine layers for smooth curvature; balanced modes for speed
Required; contact points can be placed on non-cosmetic faces
Standard, tough, high-temp, clear, flexible, and castable photopolymers. Catalog names open on the materials page.
Washed and UV post-cured is the default. Clear coat or paint is the usual visual upgrade.
Support nubs dressed off. Smooth, slightly glossy resin skin — the usual prototype deliverable.
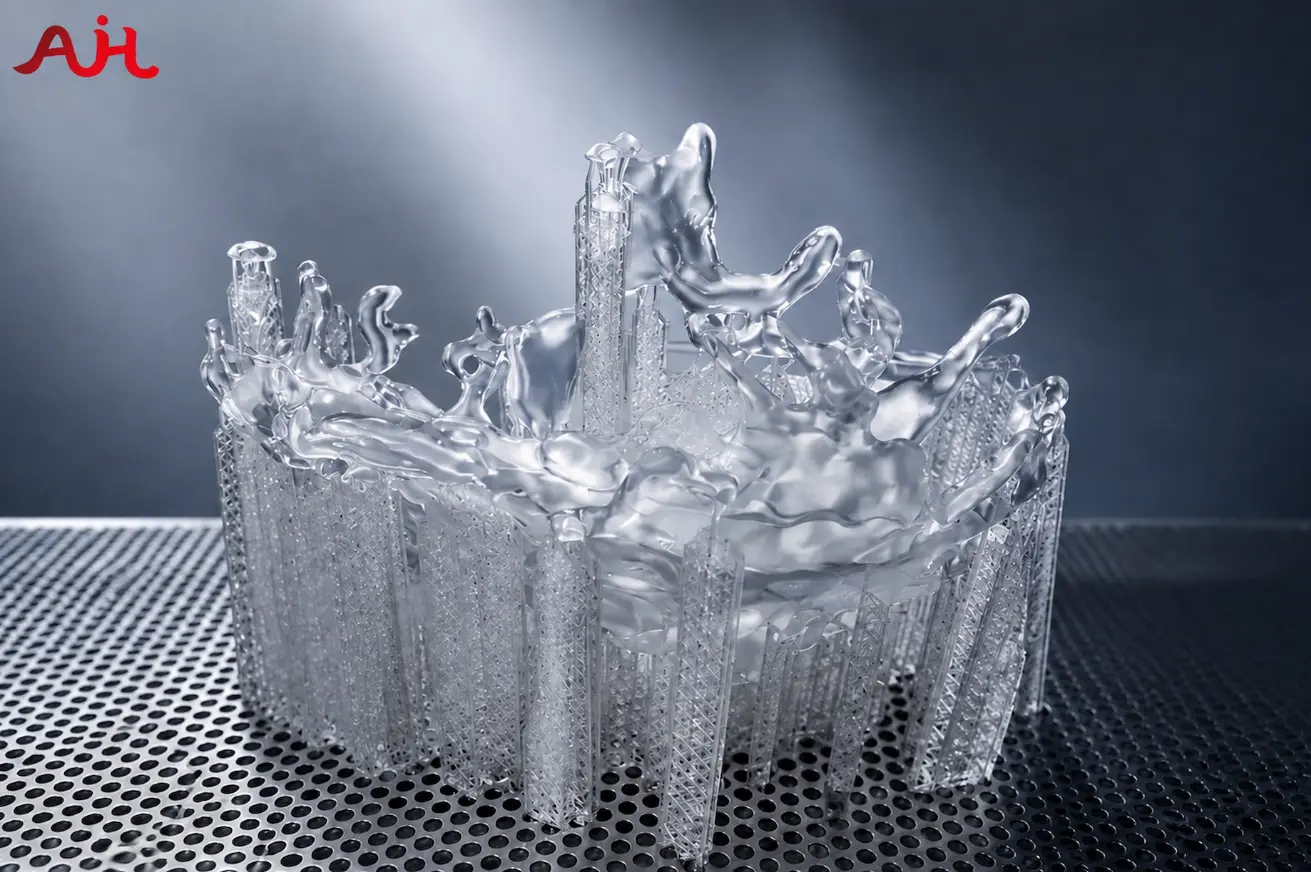
Clear or tinted coat on transparent grades to even the surface and protect edges.
Primed and painted show models, or dyed accents, when the review needs a product-like color.
SLA is the laser-resin option. DLP and LCD expose a full layer at once; SLS/MJF skip supports on nylon.
| プロセス | 納期 | 公差 | 料金 |
|---|---|---|---|
| 選択的レーザー溶融 (SLM)Metal | From 5 business days (express options where available) | ±0.3 mm or ±0.3% (whichever is greater), tighter after machining | Instant quote · typical metal part from $90 |
| 光造形 (SLA)Resin | Quoted with your CAD upload | Instant quote · typical resin part from $18 | |
| デジタルライトプロセッシング (DLP)Resin | From 48 hours | ±0.2 mm on supported geometry | Instant quote · typical resin batch from $20 |
| 液晶ディスプレイ光造形 (LCD)Resin | From 48 hours | ±0.2 mm on supported geometry | Instant quote · typical resin part from $16 |
| 選択的レーザー焼結 (SLS)Plastic powder | From 48 hours express; 72 hours / 5 days standard tiers | ±0.3 mm or ±0.3% | Instant quote · typical nylon part from $28 |
| マルチジェットフュージョン (MJF)Plastic powder | From 48 hours express; standard 72 hours / 5 days | ±0.3 mm or ±0.3% | Instant quote · typical PA12 part from $25 |
| 熱溶解積層法 (FDM)Thermoplastic filament | From 24–48 hours depending on size | ±0.5 mm or ±0.5% on FDM-appropriate geometry | Instant quote · typical prototype from $12 |
The model is sliced and oriented to minimize support contact on cosmetic surfaces.
A UV laser draws each layer on the resin surface, curing it to the previous layer.
Supports stabilize islands and overhangs during the build, preferably on B-side faces.
Parts are washed, UV post-cured, and supports removed before optional clear coat or painting.
Orientation hides supports on B-side faces when you mark cosmetics. Drain holes are added or requested on hollow show parts.
Parts are washed, UV post-cured, and support-removed before any coat. Resin choice follows heat, clarity, and handling notes on the RFQ.
Resin has a minimum wall. Hollow parts need a way for liquid to leave.
| Feature | Recommended practice |
|---|---|
| Walls | Stay above the resin’s minimum wall so shells do not print incomplete or brittle. |
| Drain Holes | Add drains on hollow cosmetic parts so uncured resin can escape. |
| Cosmetic Faces | Mark A-sides so supports can sit on the back of the model. |
| Fine Text | Raised or engraved text should stay above the layer and laser spot size. |
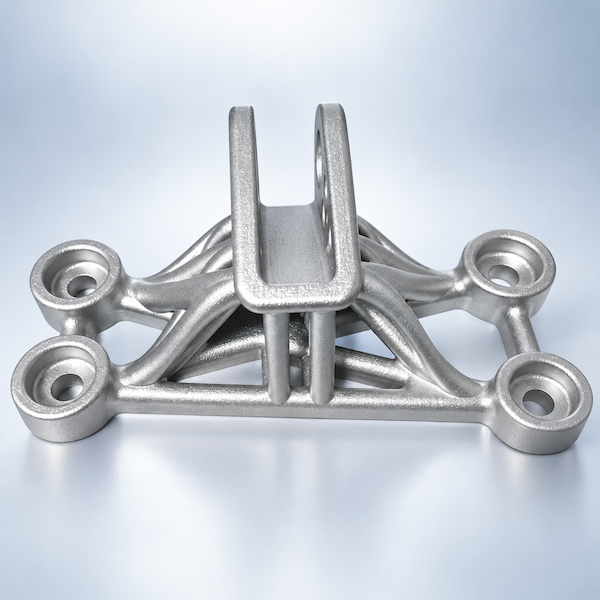
Selective Laser Melting (SLM) is a powder-bed metal additive process. A high-power laser scans each cross-section of your CAD model, melting metal powder that solidifies into a dense part.
プロセス詳細を見る
Digital Light Processing (DLP) solidifies an entire layer of photopolymer at once using a projected image.
プロセス詳細を見る
Liquid Crystal Display (LCD) printing — also called MSLA — cures a full layer of photopolymer at once.
プロセス詳細を見るWhen surface quality, small text, or a show-model finish matters more than impact toughness or raw cost.
Yes, on clear and translucent resins. A clear coat is usually needed for a lens-like look.
About ±0.2 mm on well-supported features. Large spans and thin unsupported walls wander more.
Yes. We place them on non-cosmetic faces when you mark the show side.
Standard resin jobs often leave from 48 hours after the file is approved.
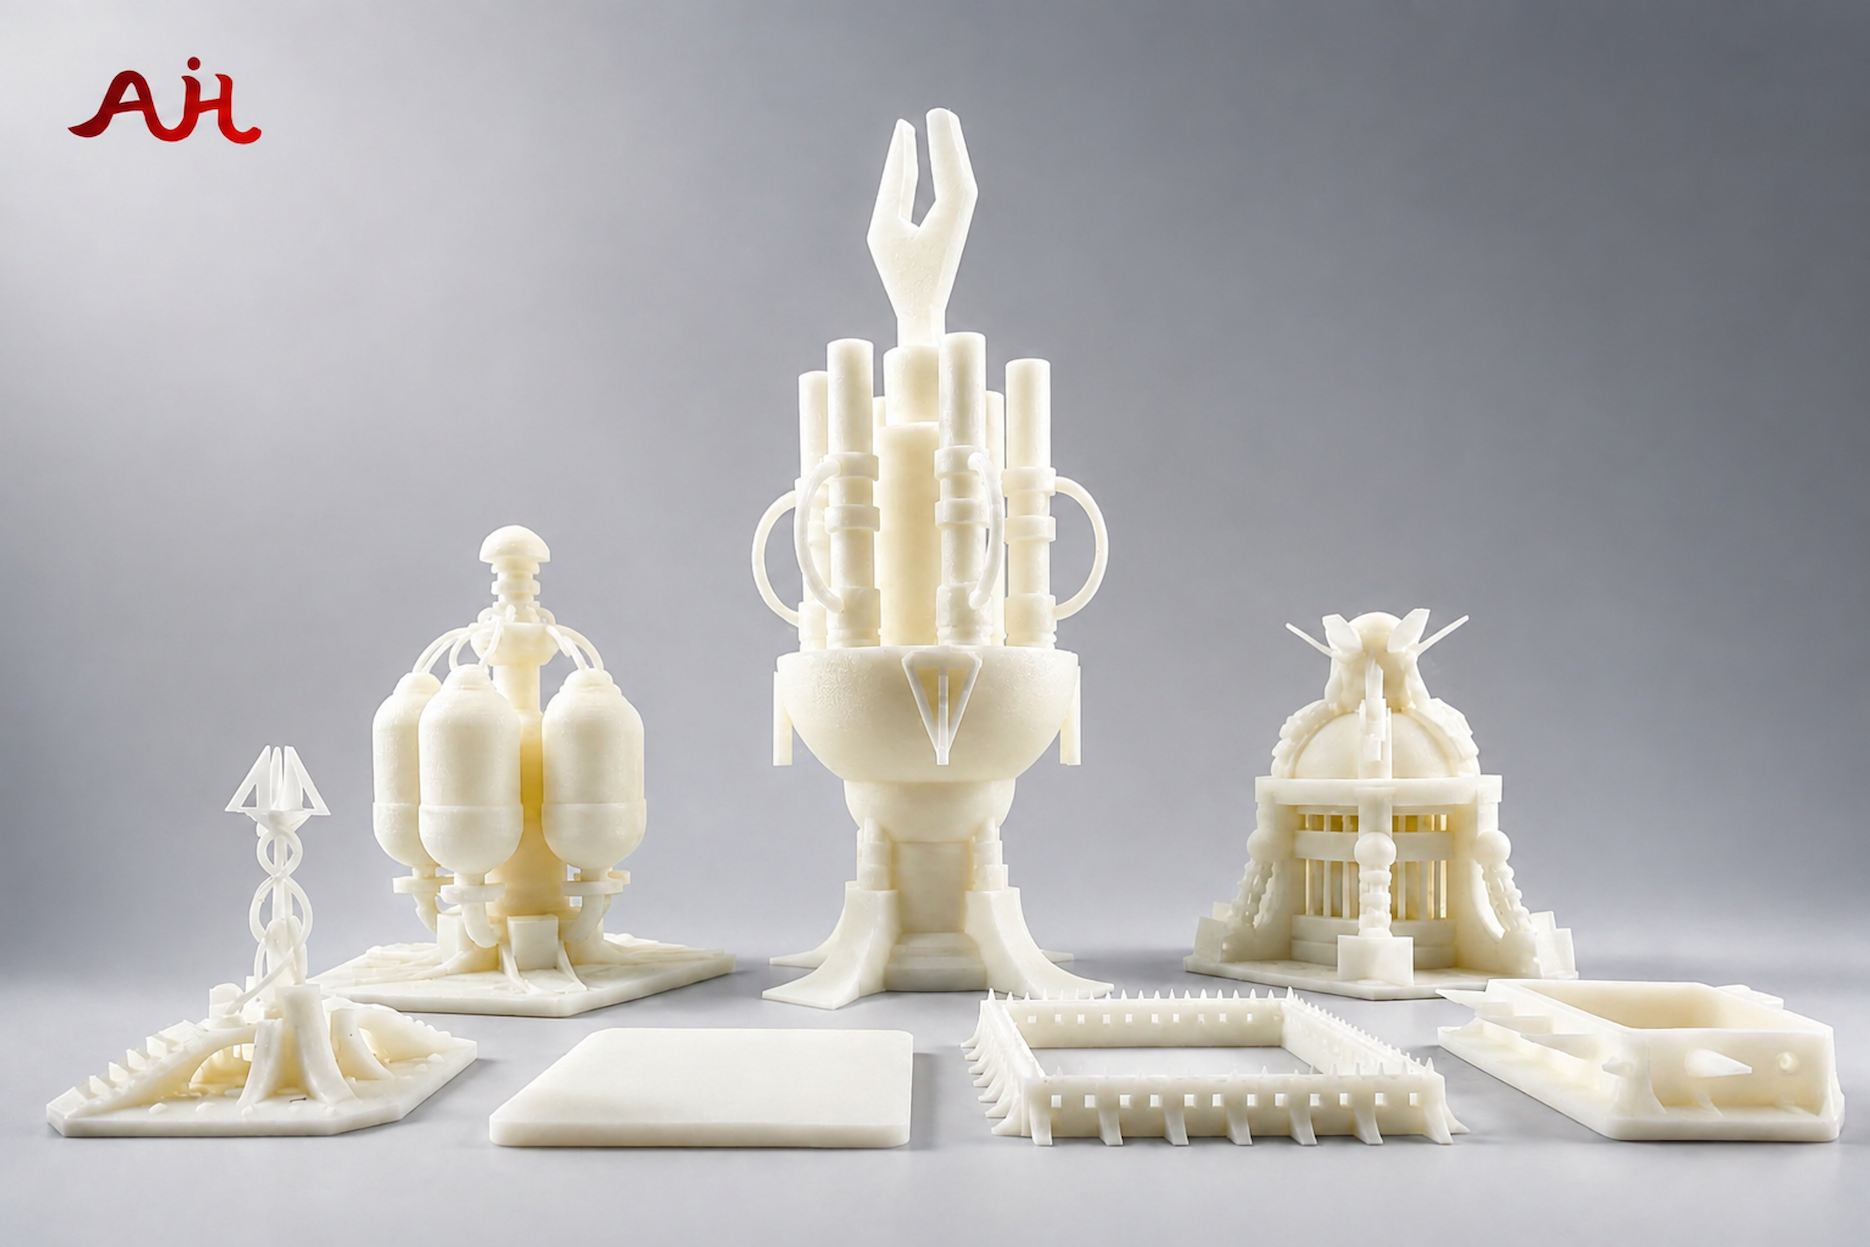
This in-depth technical comparison examines the two dominant resin-based 3D printing technologies — Stereolithography (SLA) and Digital Light Processing (DLP) — to help industry pr
プロセス詳細を見る
Learn how SLA resin printing supports B2B product development—from visual models, fit checks, and ergonomic studies to master patterns for silicone molding and investment casting.
プロセス詳細を見る
Compare SLA resin types, material properties, and real grade data to choose the right resin for detailed models, functional prototypes, and production parts.
プロセス詳細を見る
Compare DLP and SLA resin 3D printing for small, detailed prototypes. See how exposure methods, batch layouts, and finishing affect process selection.
プロセス詳細を見る
Learn how to order SLA parts, prepare CAD files, compare quotes, approve production, and check finished parts from supplier selection through delivery.
プロセス詳細を見る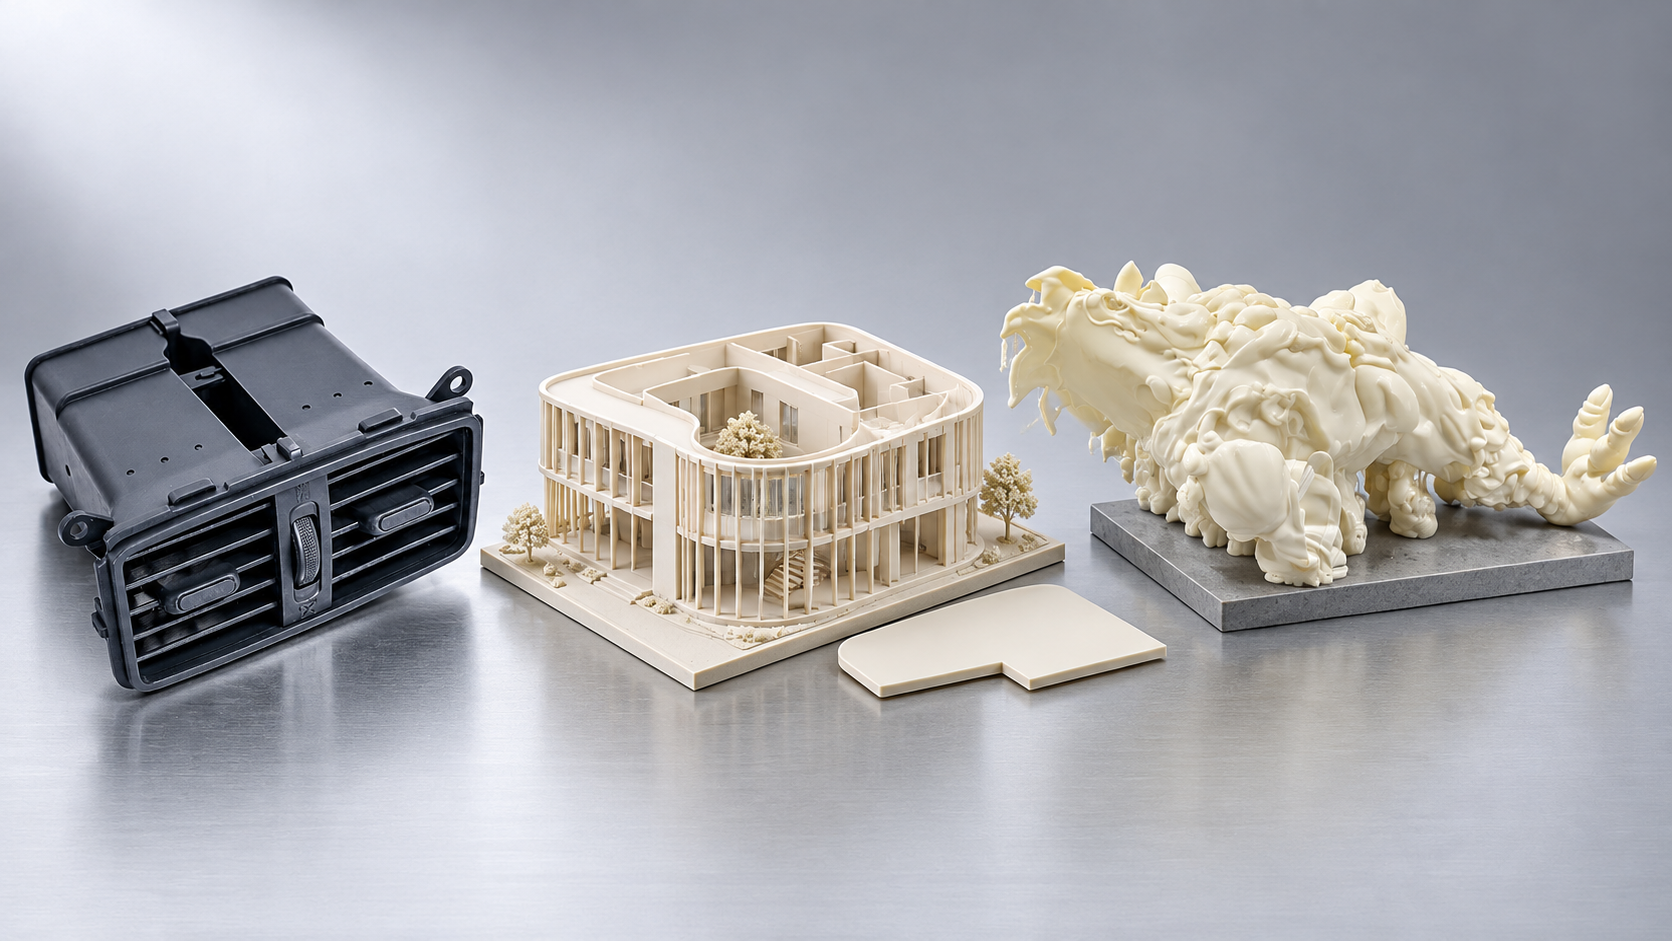
Explore SLA 3D printing applications in manufacturing, automotive, architecture, education, toys, and medical development, from models to casting patterns.
プロセス詳細を見るUse these process-specific checks when preparing your model, drawing and quote request. The confirmed quotation and approved drawing define the requirements for your part.
Specify visual, fit-check or functional use. Standard, tough, clear and heat-resistant resins are distinct grades. For sustained loads, sunlight or elevated temperature, review the selected resin data and test the application rather than treating a detailed resin model as a production thermoplastic.
Mark the presentation face and mating surfaces. Support contacts may need sanding; polishing a clear part affects both appearance and dimensions. Hollow geometry needs drainage and access for cleaning and curing. Define which holes or fits need a secondary operation.
Confirm resin grade, color or transparency target, support-mark locations and whether dimensions are checked after curing and finishing. Use a sample when optical appearance or a sensitive fit determines acceptance.
AIHFABSはCADアップロードからカスタム3DプリントとCNCの見積を出します。SLA、SLS、MJF、SLM、FDM、DLP、フライス、旋削を比較し、同じ注文でベイパースムージング、染色、陽極酸化、研磨、粉体塗装を追加できます。
インスタント見積は試作、治具、ハウジング、小ロット向けです。材料、プロセス、数量、納期が揃って表示されます。
材料、プロセス、数量、納期が揃って表示され、仕様変更が新たな問い合わせにならないようにします。
STL、STEPなど一般的なCADをアップロードしてオンライン見積。
同じ部品で3Dプリント技術とCNCを比較。
ポリマーまたは金属を選び、必要なら3D Plusハードウェア仕上げを追加。
決済前に価格と納期を確認。特殊仕様は手動見積。
このページのプロセス、業界、サンプルを再現したい場合は、アップロードから技術と仕上げを図面に合わせてください。
当サイトでは Cookie を使用して体験をパーソナライズしています。本サイトを利用することで、以下に同意したものとみなされます: プライバシーポリシー
同意する