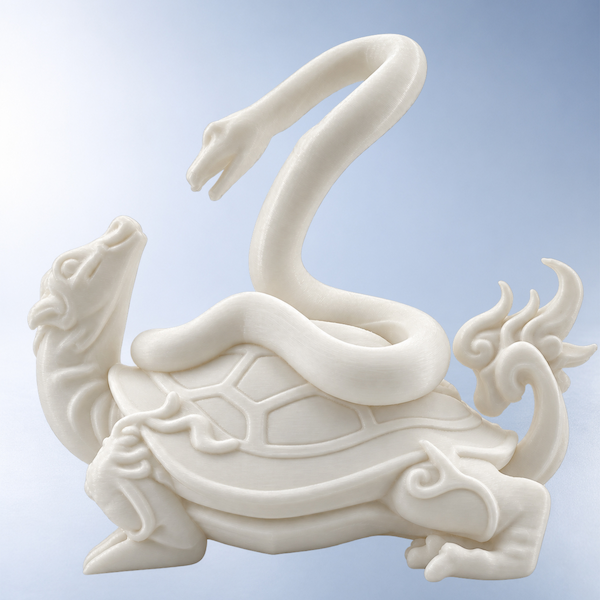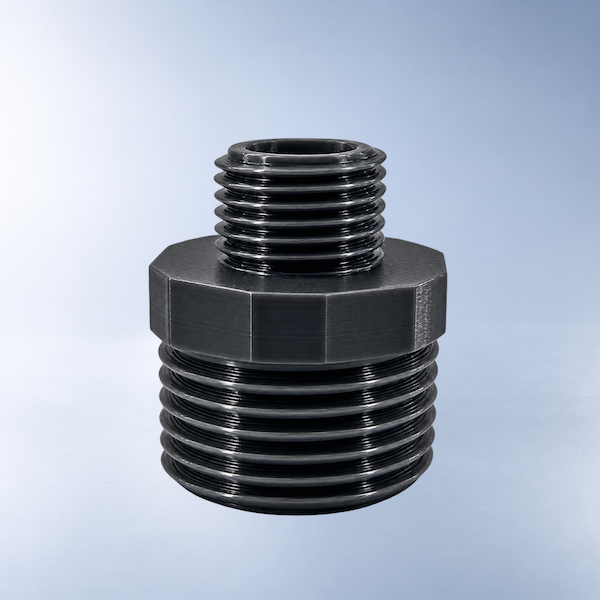
Lead time
From 24–48 hours depending on size

3Dプリント
Extruded thermoplastic layers for rapid, economical prototypes.
Fused Deposition Modeling (FDM) extrudes heated thermoplastic filament in thin beads, stacking layers to form a part. FDM is economical for early prototypes, large bulky geometry, and fixtures where surface cosmetics are secondary to speed and cost.
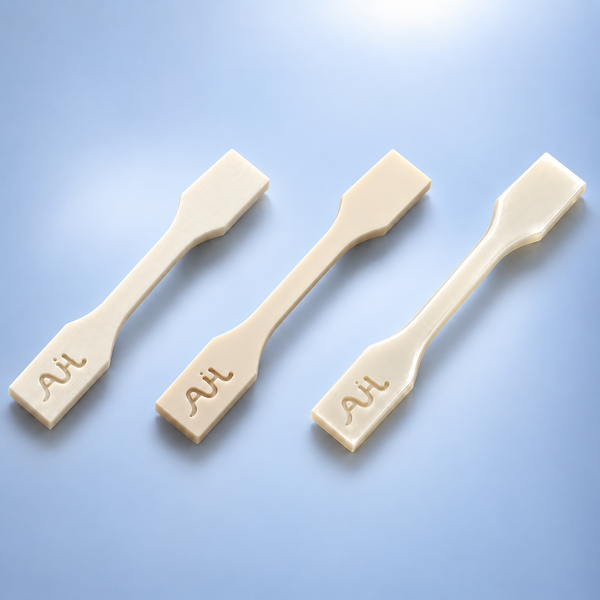
Fused Deposition Modeling pushes a thermoplastic filament through a hot nozzle and stacks beads into a part. It is the fastest way to get a large, cheap shape on the table when layer lines are acceptable.
AIHFABS quotes FDM for jigs, early form-and-fit, and bulky exhibition models. If you need a smooth show face or nylon-level isotropy, move the same file to SLA or SLS instead of sanding for days.
Layer height and envelope vary by cell. Large-format jobs are reviewed before a date is promised.
From 24–48 hours depending on size
±0.5 mm or ±0.5% on FDM-appropriate geometry
Varies by machine; large-format options on request
Visible layer lines; sanding and coating improve appearance
Breakaway or soluble supports on overhangs
Layer lines are part of the process. Sand, fill, or coat only the faces that will be seen.
Visible beads. Correct for shop aids, fixtures, and most internal mock-ups.
Layer lines knocked down and filled on show faces before paint.
Paint, primer, or tapped inserts after support removal.
FDM is the cost and size lever. Resin and powder beds take over when finish or isotropy matters more than price.
| プロセス | 納期 | 公差 | 料金 |
|---|---|---|---|
| 選択的レーザー溶融 (SLM)Metal | From 5 business days (express options where available) | ±0.3 mm or ±0.3% (whichever is greater), tighter after machining | Instant quote · typical metal part from $90 |
| 光造形 (SLA)Resin | Quoted with your CAD upload | Instant quote · typical resin part from $18 | |
| デジタルライトプロセッシング (DLP)Resin | From 48 hours | ±0.2 mm on supported geometry | Instant quote · typical resin batch from $20 |
| 液晶ディスプレイ光造形 (LCD)Resin | From 48 hours | ±0.2 mm on supported geometry | Instant quote · typical resin part from $16 |
| 選択的レーザー焼結 (SLS)Plastic powder | From 48 hours express; 72 hours / 5 days standard tiers | ±0.3 mm or ±0.3% | Instant quote · typical nylon part from $28 |
| マルチジェットフュージョン (MJF)Plastic powder | From 48 hours express; standard 72 hours / 5 days | ±0.3 mm or ±0.3% | Instant quote · typical PA12 part from $25 |
| 熱溶解積層法 (FDM)Thermoplastic filament | From 24–48 hours depending on size | ±0.5 mm or ±0.5% on FDM-appropriate geometry | Instant quote · typical prototype from $12 |
Filament is fed through a heated nozzle that deposits beads along slice paths.
The build plate or toolpath strategy supports overhangs with soluble or breakaway structures.
Layers fuse together as they cool; chamber heating improves ABS and nylon performance.
Supports are removed and parts can be sanded, tapped, or bonded.
Orientation, infill, and wall count are set from how the part will be loaded — not from a default slicer profile. Tell us if it is a visual mock or a fixture that will see clamp force.
Supports come off before tap, sand, or coat. Soluble supports are used when the overhang would scar a show face.
Orient for strength and for the faces you refuse to sand.
| Feature | Recommended practice |
|---|---|
| Orientation | Keep cosmetic faces off support interfaces when you can. |
| Fillets | Add fillets on load-bearing corners; sharp notches crack along layers. |
| Infill & walls | Say if the part is loaded — we will raise walls and infill instead of guessing. |
| Overhangs | Expect breakaway or soluble supports below about 45°. |
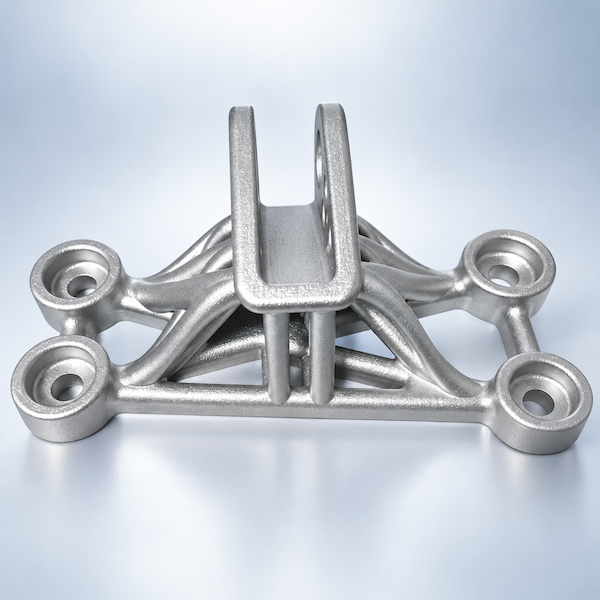
Selective Laser Melting (SLM) is a powder-bed metal additive process. A high-power laser scans each cross-section of your CAD model, melting metal powder that solidifies into a dense part.
プロセス詳細を見る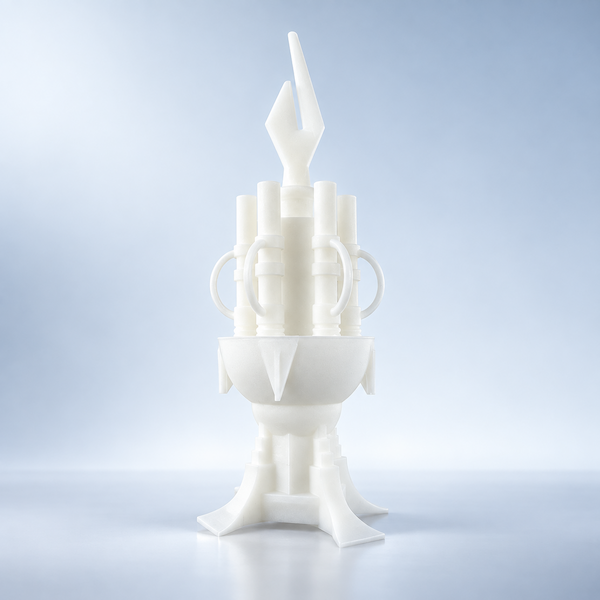
Stereolithography (SLA) cures liquid photopolymer with a precision UV laser, building parts layer by layer.
プロセス詳細を見る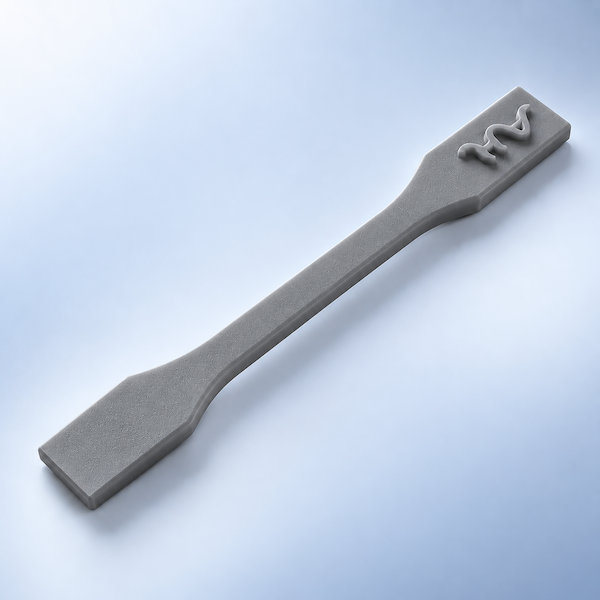
Digital Light Processing (DLP) solidifies an entire layer of photopolymer at once using a projected image.
プロセス詳細を見るEarly form-and-fit, large bulky geometry, and shop aids where layer lines are acceptable and cost matters.
About ±0.5 mm or ±0.5% on FDM-appropriate geometry. Fine fits belong on CNC or powder-bed nylon.
PLA, ABS, PETG, ASA, nylon, and carbon-filled blends. Tell us about heat, UV, and outdoors.
Yes — large-format cells are available. Envelope is confirmed after we open the file.
Many jobs leave in 24–48 hours depending on size and finish.
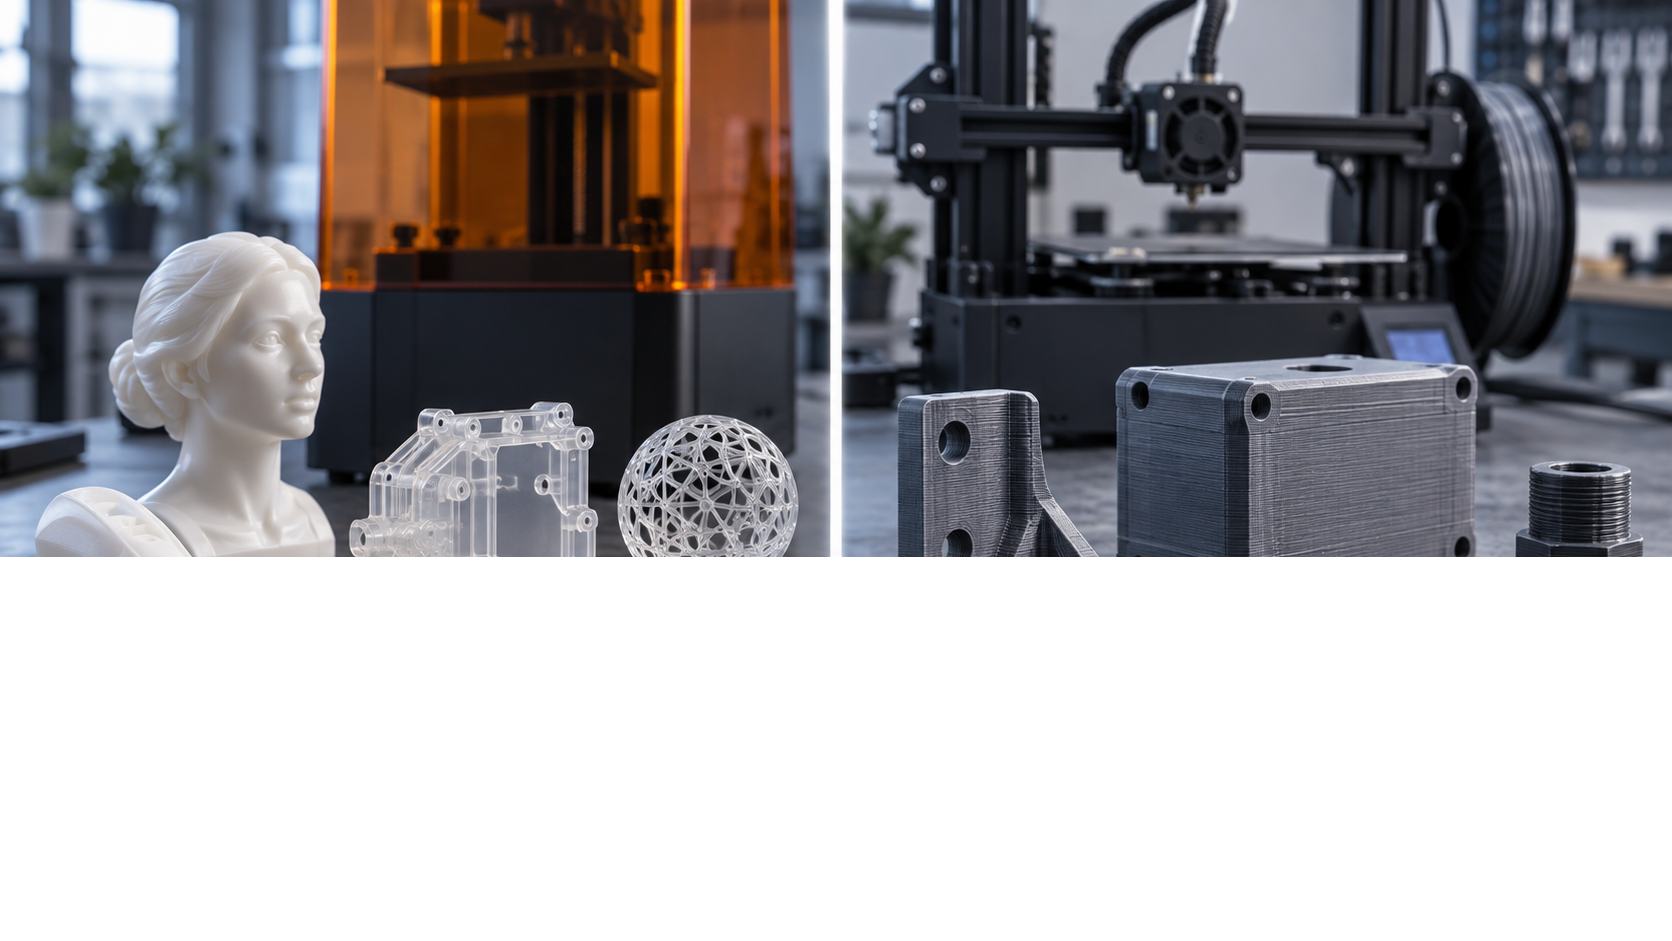
Compare SLA and FDM 3D printing for surface quality and fine details. Learn which technology suits smooth finishes, tight tolerances, and intricate geometries in prototyping and en
プロセス詳細を見る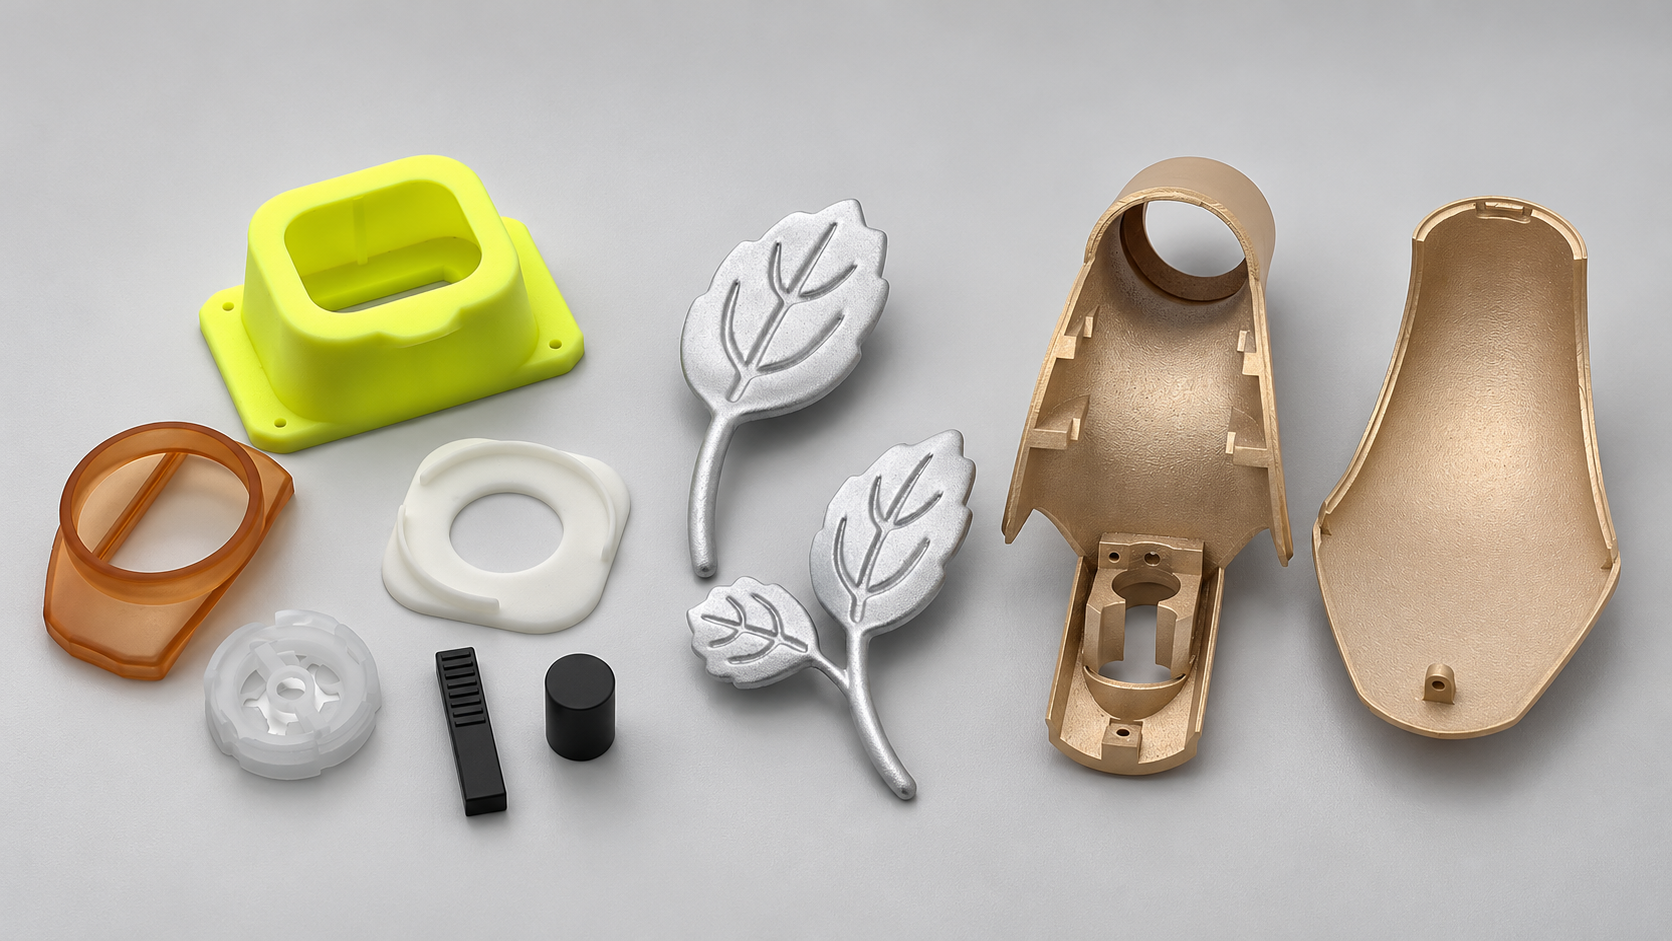
Compare SLA with DLP, LCD, FDM, SLS, MJF, SLM, and CNC machining. Shortlist processes by material, geometry, finish, cost, and your part's intended use.
プロセス詳細を見る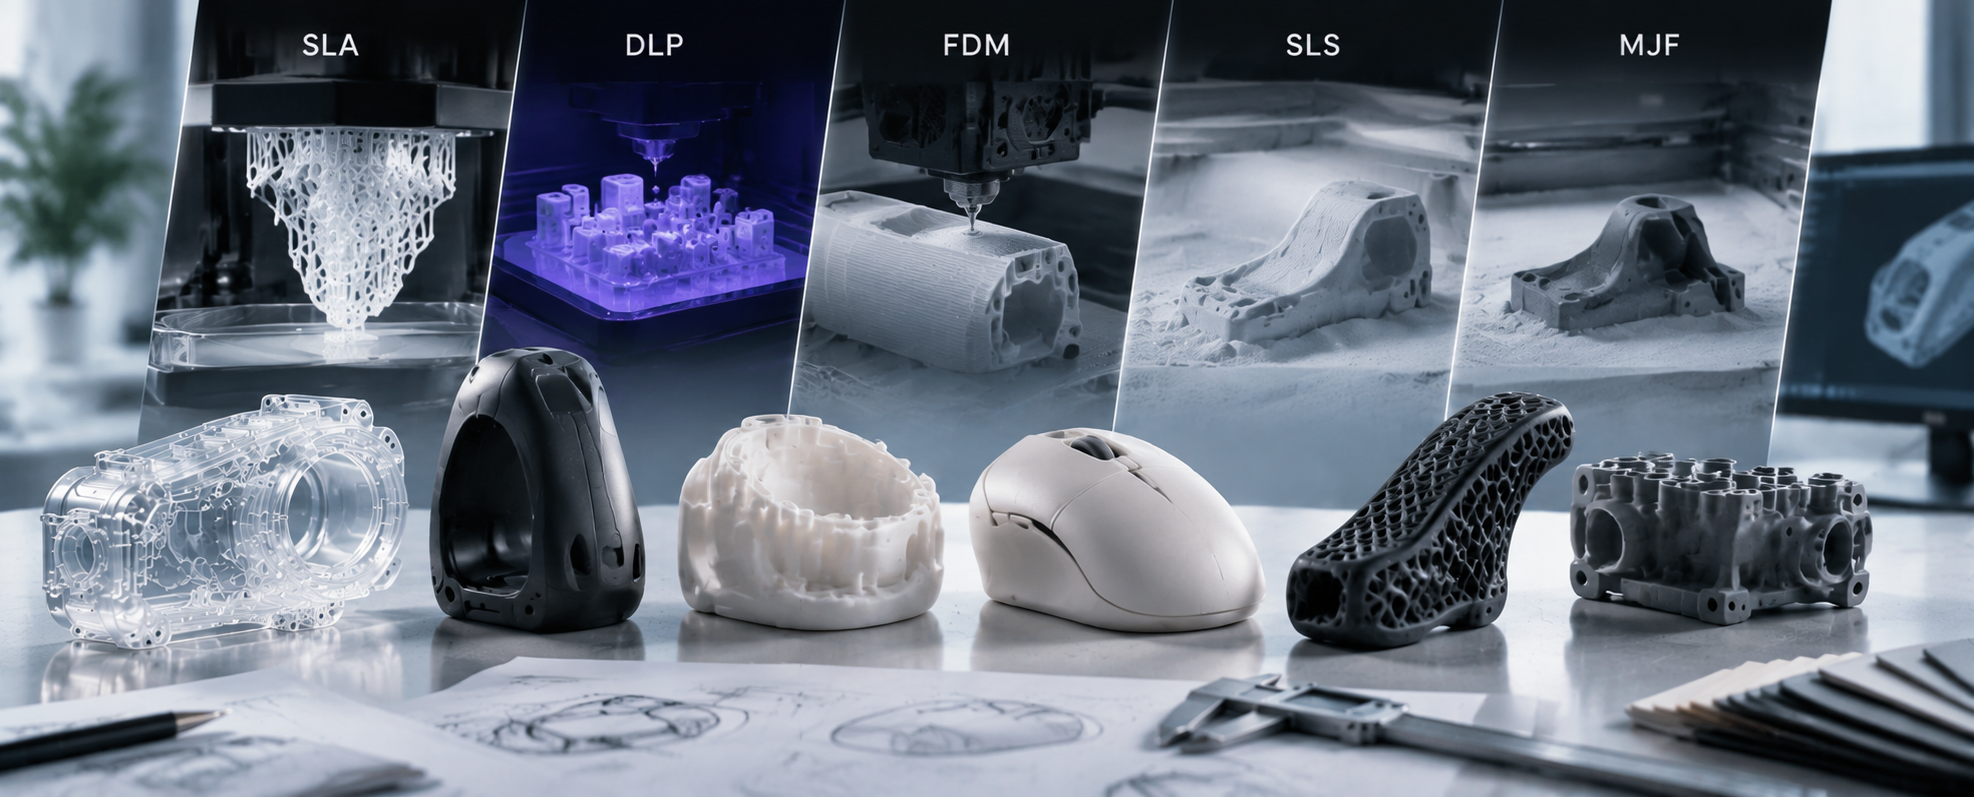
Learn how to choose the right 3D printing process for cosmetic prototype parts. Compare SLA, DLP, FDM, SLS, and MJF for surface quality, detail, fit, and finishing.
プロセス詳細を見る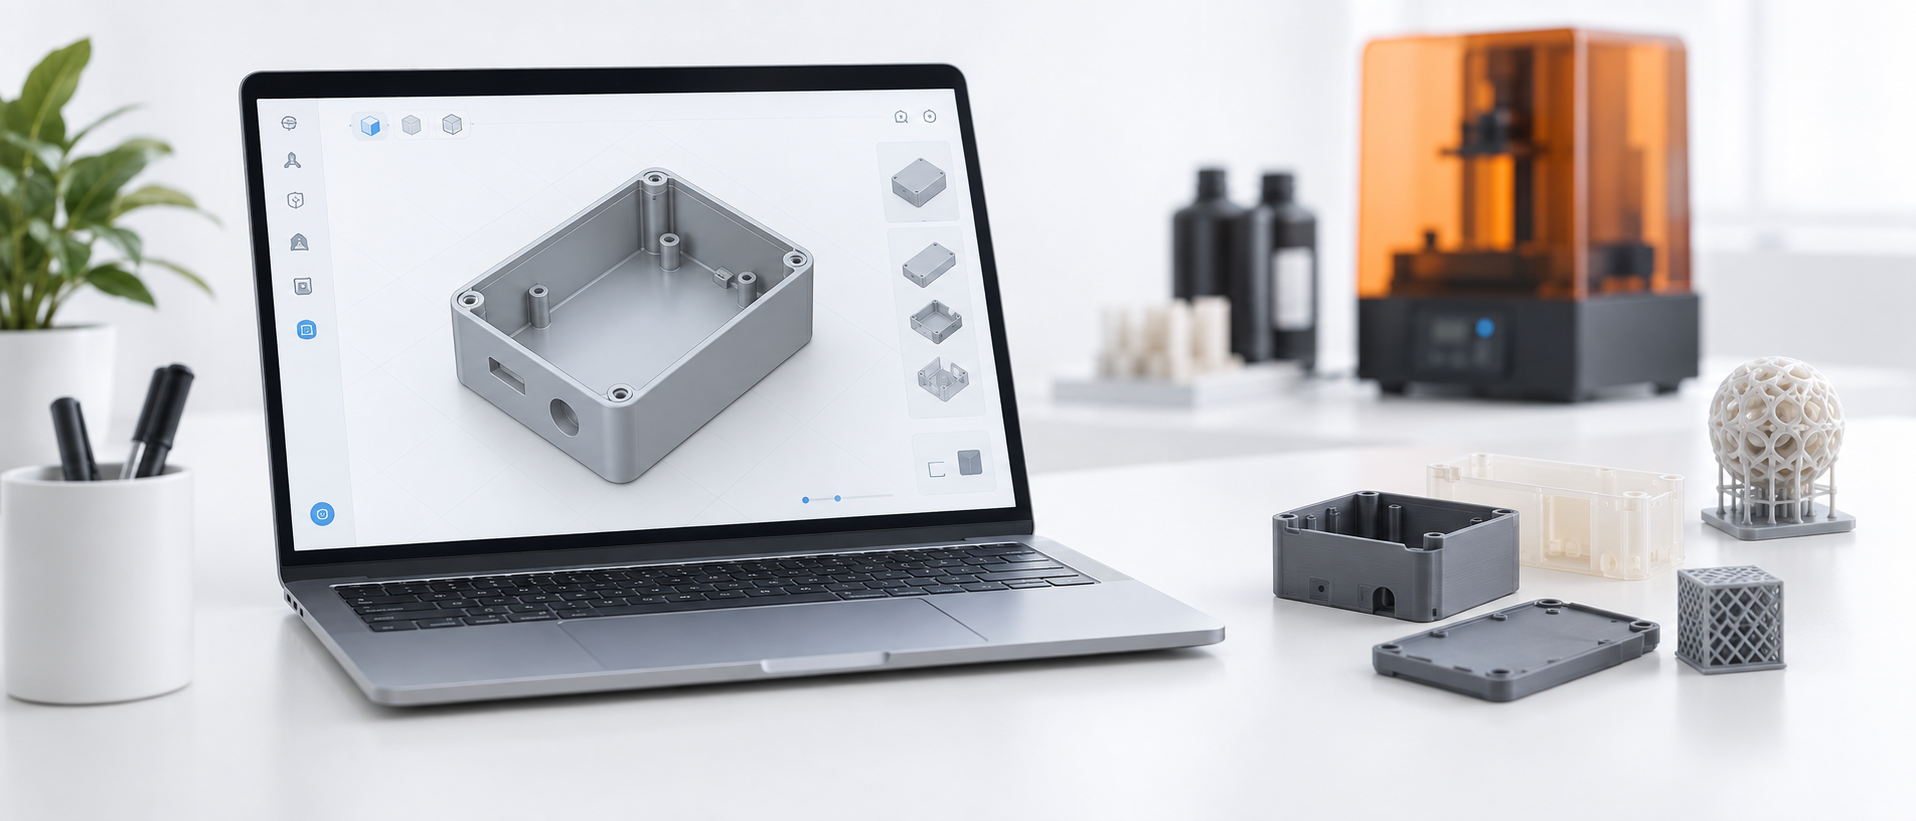
Step-by-step guide to uploading STL and STEP files for instant resin 3D printing quotes. Learn file preparation, unit settings, wall thickness, orientation, and how to read quote r
プロセス詳細を見るUse these process-specific checks when preparing your model, drawing and quote request. The confirmed quotation and approved drawing define the requirements for your part.
FDM parts are built from deposited roads and layers. Show the direction of load and the environment so orientation, wall strategy and material can be reviewed together. ABS and PETG are different materials; neither should be selected by appearance alone.
Support-facing surfaces can have a different texture and accuracy from accessible walls. Consider splitting a large part into an assembly when support removal is difficult. Specify inserts and threaded interfaces early, and state whether the part is a visual model or working fixture.
Confirm filament grade, build orientation where function depends on it, visible layer texture and required assembly fit. Discuss heat exposure and sustained load before using a printed fixture in production.
AIHFABSはCADアップロードからカスタム3DプリントとCNCの見積を出します。SLA、SLS、MJF、SLM、FDM、DLP、フライス、旋削を比較し、同じ注文でベイパースムージング、染色、陽極酸化、研磨、粉体塗装を追加できます。
インスタント見積は試作、治具、ハウジング、小ロット向けです。材料、プロセス、数量、納期が揃って表示されます。
材料、プロセス、数量、納期が揃って表示され、仕様変更が新たな問い合わせにならないようにします。
STL、STEPなど一般的なCADをアップロードしてオンライン見積。
同じ部品で3Dプリント技術とCNCを比較。
ポリマーまたは金属を選び、必要なら3D Plusハードウェア仕上げを追加。
決済前に価格と納期を確認。特殊仕様は手動見積。
このページのプロセス、業界、サンプルを再現したい場合は、アップロードから技術と仕上げを図面に合わせてください。
当サイトでは Cookie を使用して体験をパーソナライズしています。本サイトを利用することで、以下に同意したものとみなされます: プライバシーポリシー
同意する