Lead time
From 48 hours express; 72 hours / 5 days standard tiers

3Dプリント
Professional nylon 3D printing for functional prototypes, jigs, and production-like SLS parts — no support trees on most geometry.
AIHFABS SLS 3D printing services fuse engineering-grade SLS plastics into durable, self-supporting parts. A laser sinters nylon powder layer by layer; unsintered powder holds the geometry, so ducts, hinges, and nested batches print without support scars. Choose sintered nylon when you need tough SLS parts for fit, function, and short-run production — not a show-resin cosmetic.
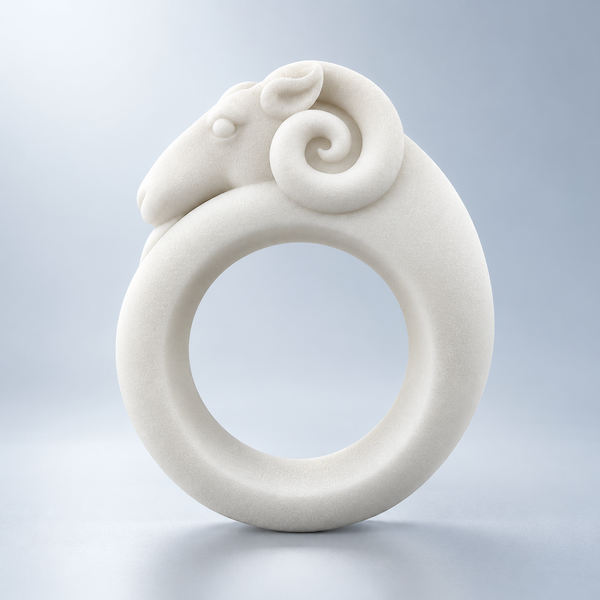
Selective Laser Sintering (SLS) is a powder-bed process: a laser traces each slice and fuses thermoplastic particles into sintered nylon. Loose powder stays around the part and acts as a nest, so most geometries do not need printed supports. That is why ducts, living features, and packed batches are everyday SLS work.
AIHFABS runs nylon SLS printing mainly in PA11, PA12, and glass filled nylon SLS, plus PP and TPU where the job needs them. After cool-down we break the cake, depowder, and dye or vapor-smooth when you ask for a less grainy skin.
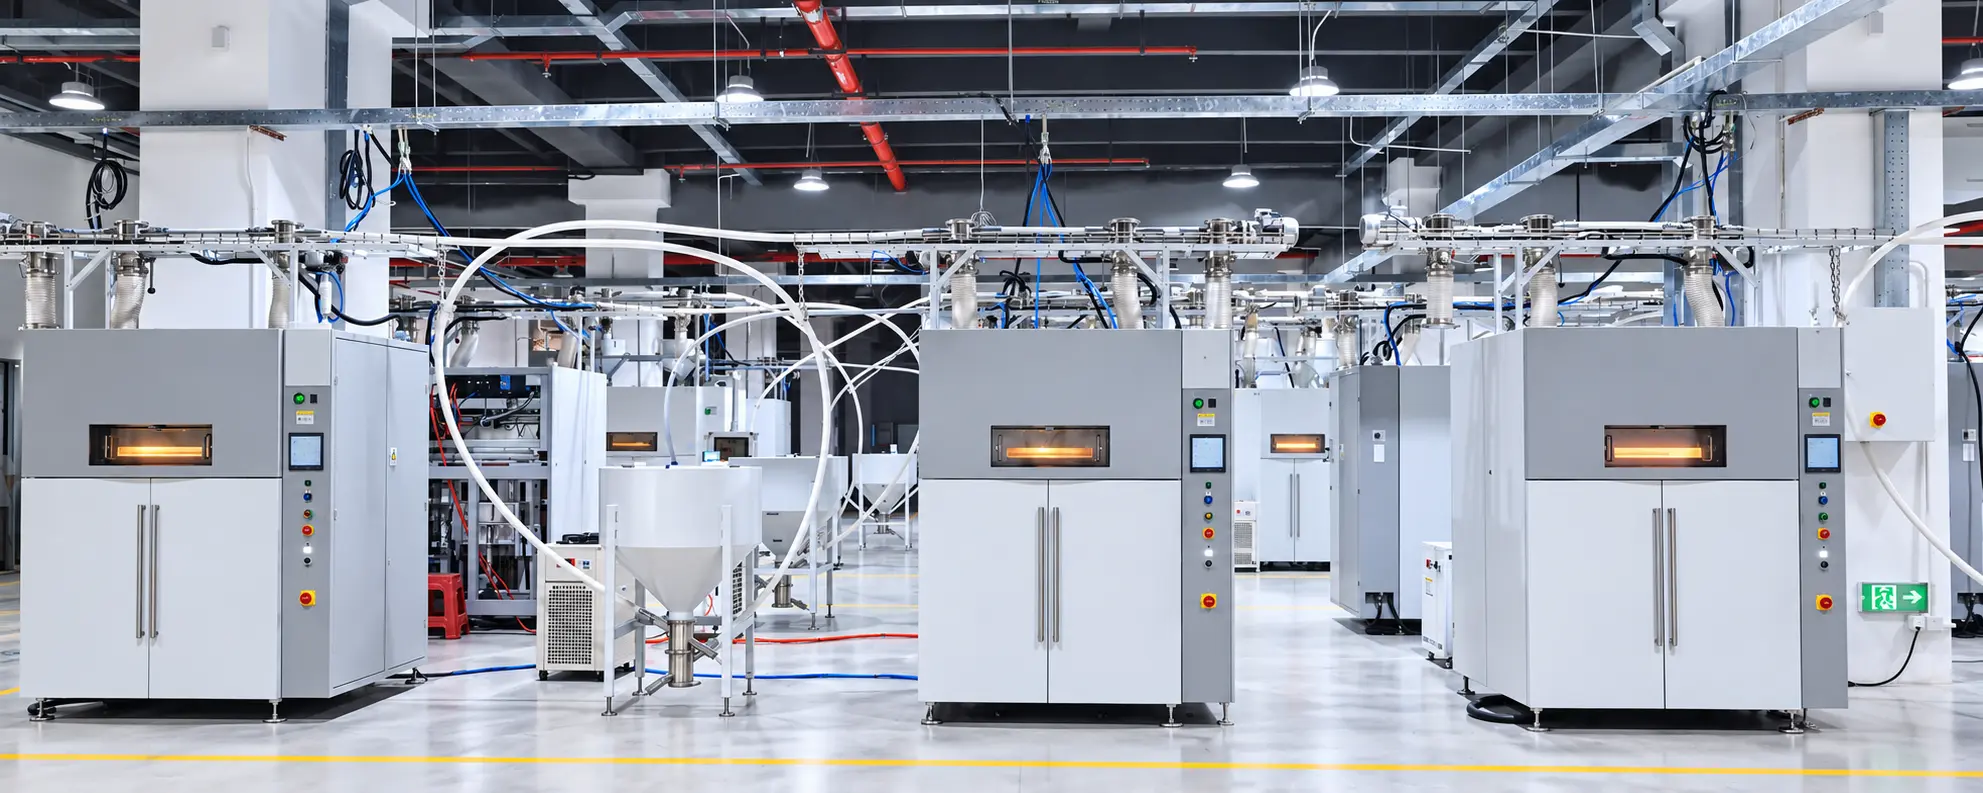
A dedicated nylon 3D printing service for functional SLS plastics — not filament mock-ups.
If you need a nylon 3D printing service that holds clips, ducts, and housings through assembly, nylon SLS is the usual first quote. Nylon SLS printing fuses engineering-grade SLS plastics into isotropic-enough parts for shop trials and short production — without support scars on internal channels.
Unfilled SLS nylon (PA12 / PA11) is the workhorse: tough, dyeable, and chemically stable. Specify glass filled nylon SLS when the cover must stay stiff near heat, or carbon-filled nylon when you want stiffness without the glass-bead mass. Grade cards are in the materials table below and on the 3D printing materials hub.
Custom SLS parts manufacturing for functional SLS printed parts — from first articles to nested production cakes.
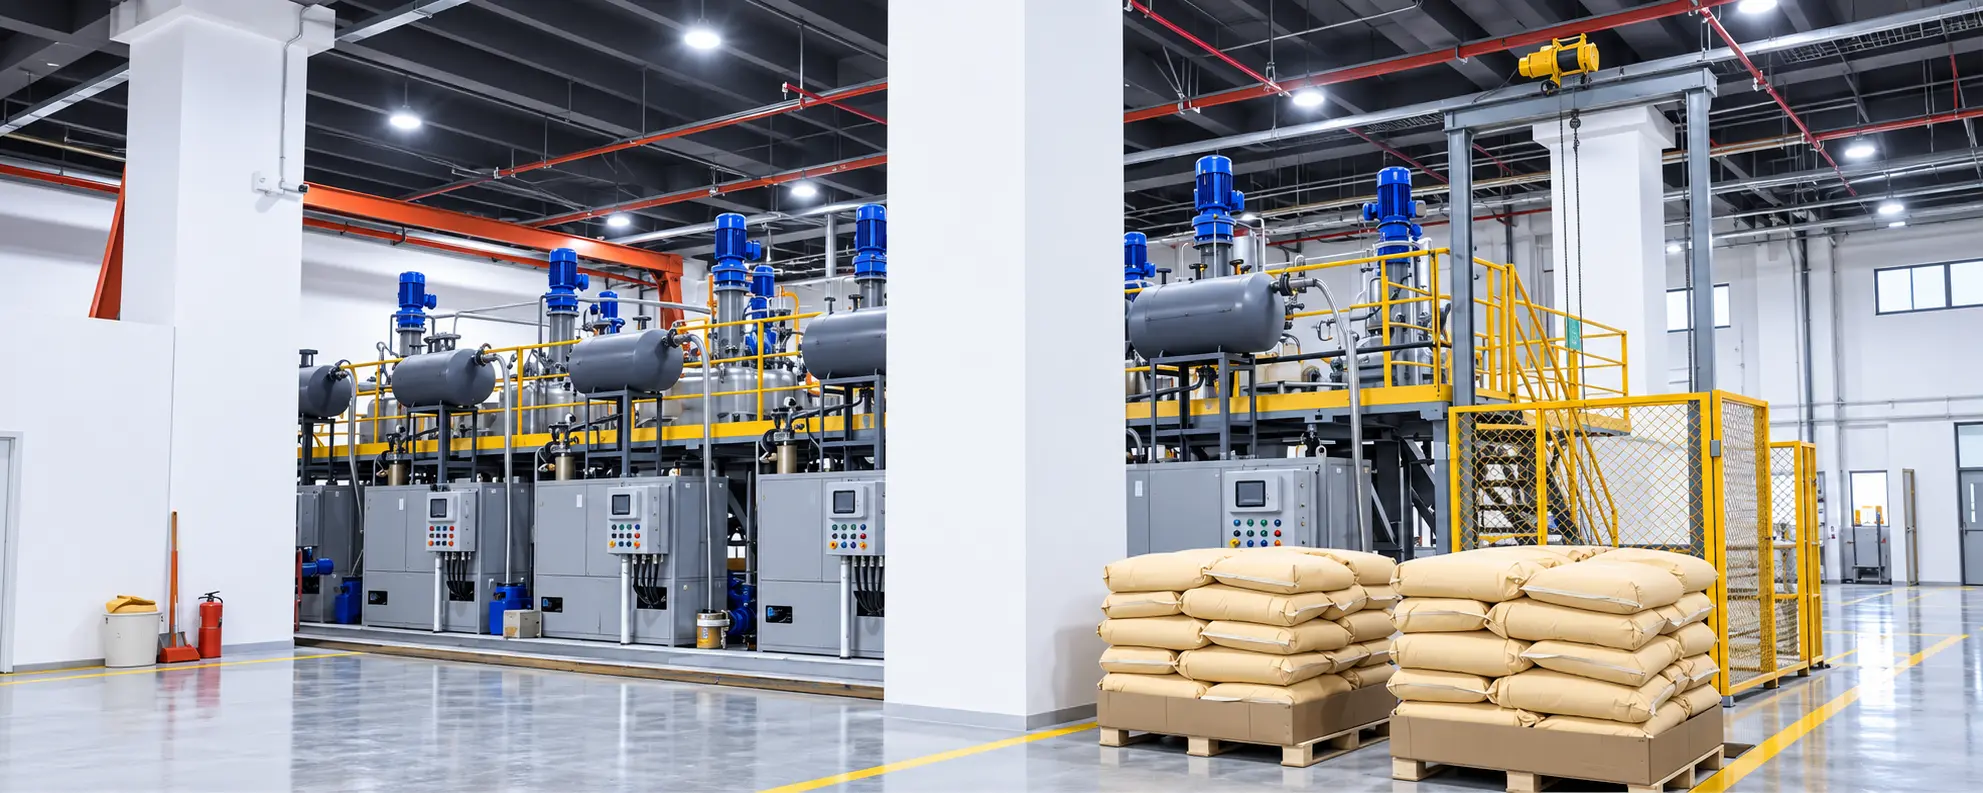
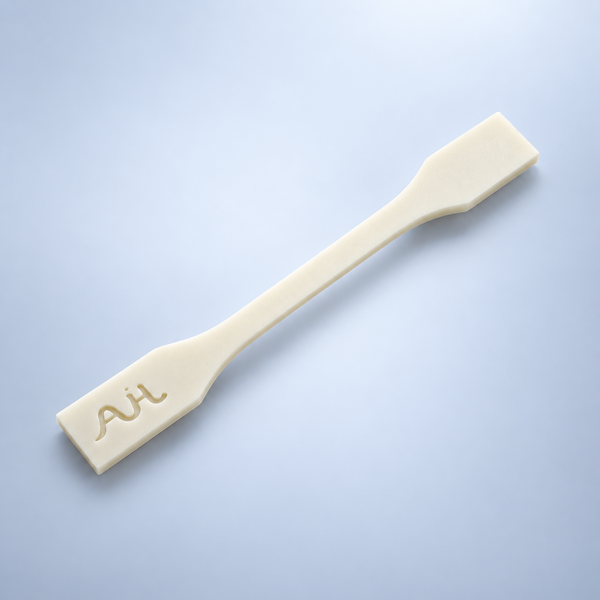
Powder-bed size and as-sintered tolerance below are planning values, not a substitute for the live quote.
From 48 hours express; 72 hours / 5 days standard tiers
±0.3 mm or ±0.3%
645 × 325 × 520 mm
Matte, slightly grainy; vapor smoothing or tumbling optional
Not required — powder bed supports the part
Engineering-grade SLS plastics first: SLS nylon (PA12 / PA11), glass filled nylon SLS, carbon-filled nylon, PP, and TPU. Catalog cards below open the grade page; filled-nylon trade-offs are in the comparison table.
Unfilled sintered nylon for snaps, ducts, and housings. PA12 is the default; PA11 when impact and elongation matter more than stiffness.
Glass beads raise modulus and heat deflection so covers and jigs hold shape. Avoid living hinges and high-elongation snaps on this grade.
Carbon fiber or mineral fill for light, stiff brackets. Different surface and anisotropy than glass-bead PA12 — pick from the datasheet on the quote, not from a slogan.
| Grade | Why choose it | Watch-outs |
|---|---|---|
| SLS nylon PA12 / PA11 | Balanced toughness, dyeable, everyday nylon SLS printing | As-sintered grain; not as stiff as filled grades |
| Glass filled nylon SLS | Stiffness, dimensional stability, higher HDT for fixtures and covers | Lower elongation; abrasive on mating plastics |
| Carbon-filled nylon | High stiffness-to-weight for brackets and light structures | Grade-specific anisotropy; confirm the datasheet on the quote |
Unpolished SLS parts leave the cake matte and slightly grainy. Dye, tumble, and vapor smooth are the usual next steps — see 3D Plus finishing for dyeing, smoothing, and coating options.
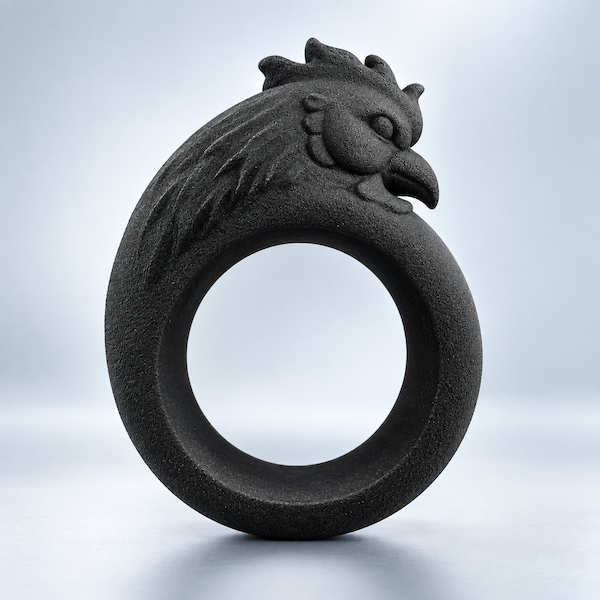
Natural white or stone-gray powder texture. Functional unpolished SLS parts — no dye, no extra cycle.
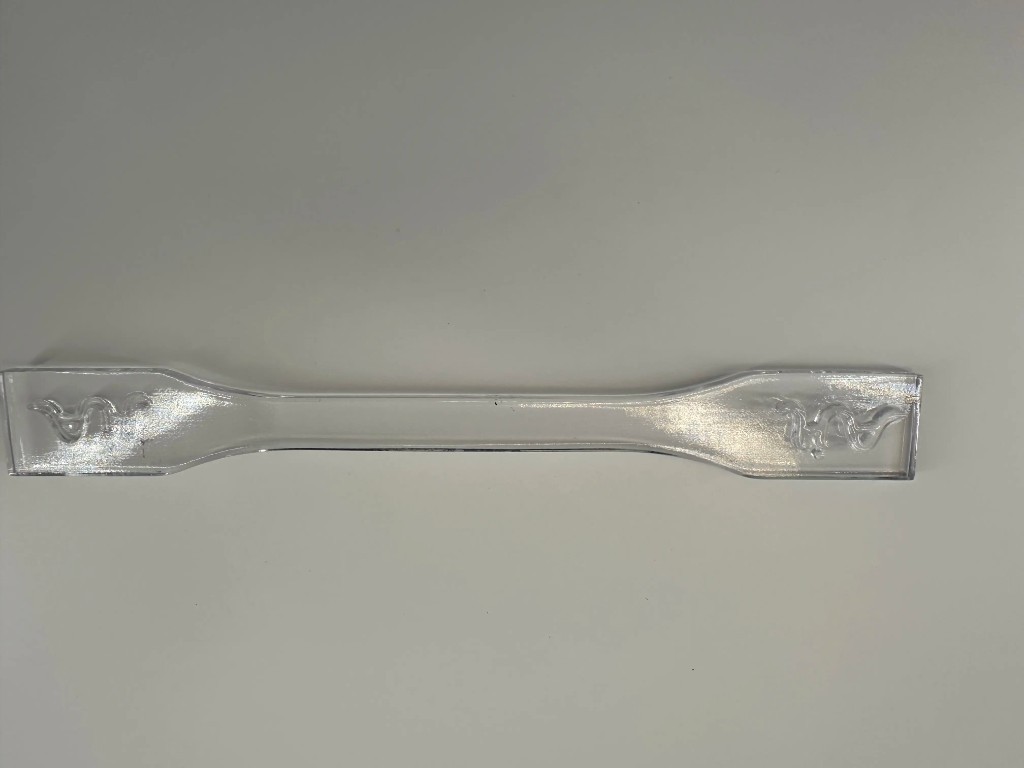
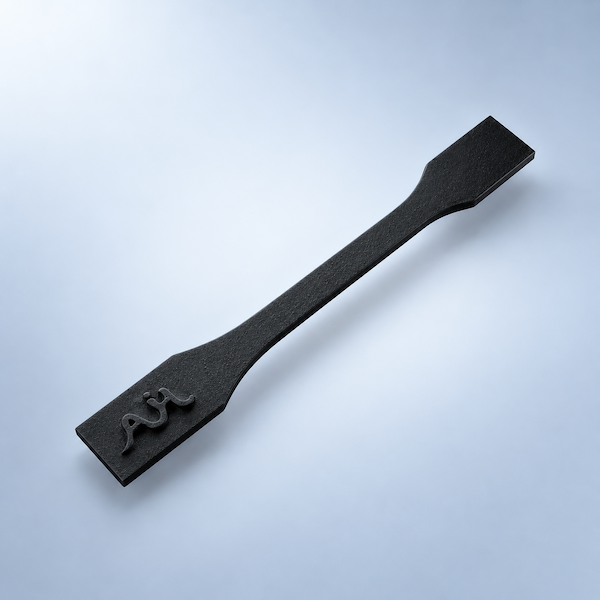
Immersion dye, most often black, that soaks a shallow layer and covers the open grain.
Chemical smooth or media tumble to close pores and take the chalky feel down on SLS printed parts.
SLS and MJF both print nylon without support trees. MJF is often faster on dense production nests; SLS still wins on some powder grades and envelopes.
| プロセス | 納期 | 公差 | 料金 |
|---|---|---|---|
| 選択的レーザー溶融 (SLM)Metal | From 5 business days (express options where available) | ±0.3 mm or ±0.3% (whichever is greater), tighter after machining | Instant quote · typical metal part from $90 |
| 光造形 (SLA)Resin | Quoted with your CAD upload | Instant quote · typical resin part from $18 | |
| デジタルライトプロセッシング (DLP)Resin | From 48 hours | ±0.2 mm on supported geometry | Instant quote · typical resin batch from $20 |
| 液晶ディスプレイ光造形 (LCD)Resin | From 48 hours | ±0.2 mm on supported geometry | Instant quote · typical resin part from $16 |
| 選択的レーザー焼結 (SLS)Plastic powder | From 48 hours express; 72 hours / 5 days standard tiers | ±0.3 mm or ±0.3% | Instant quote · typical nylon part from $28 |
| マルチジェットフュージョン (MJF)Plastic powder | From 48 hours express; standard 72 hours / 5 days | ±0.3 mm or ±0.3% | Instant quote · typical PA12 part from $25 |
| 熱溶解積層法 (FDM)Thermoplastic filament | From 24–48 hours depending on size | ±0.5 mm or ±0.5% on FDM-appropriate geometry | Instant quote · typical prototype from $12 |
Powder is preheated and spread in a thin layer across the build chamber.
The laser sinters the cross-section; unsintered powder remains in place.
The platform indexes downward; fresh powder is recoated for the next layer.
The cake is cooled, depowdered, and finished with dye, vapor smooth, or machining.
Packing density, escape holes, and wall thickness are checked before the cake is committed. Enclosed volumes without a powder exit are flagged in DFM.
After cool-down, parts are depowdered and blasted. Dye, vapor smooth, or tapping is added only when the order lists it. Unpolished SLS parts ship as-sintered unless you ask for a finish.
Let powder out, then keep walls in a band the cake can cool without banana-ing.
| Feature | Recommended practice |
|---|---|
| Escape holes | Open every enclosed volume so unsintered powder can leave. |
| Walls | About 1.0 mm unsupported and 0.8 mm supported is a safe first pass. |
| Holes & details | Keep holes and embossed details around 0.8–1.0 mm or larger. |
| Living hinges | Use a TPU grade and a tuned thickness — PA12 is the wrong hinge material. |
| Large flats | Rib large panels so they stay flatter through cool-down. |
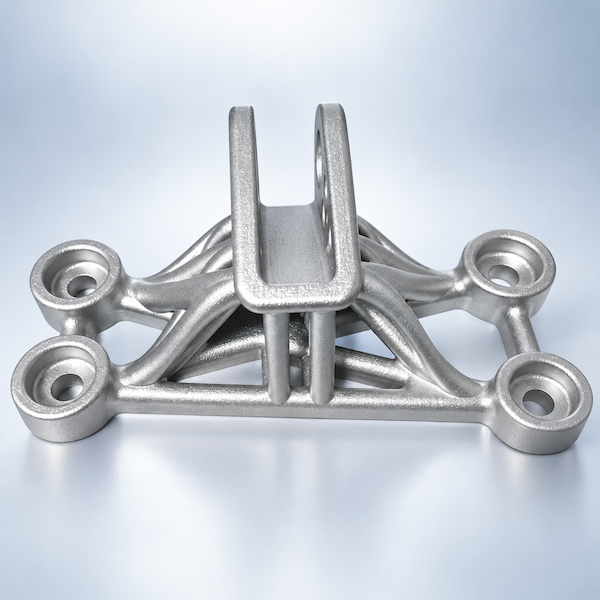
Selective Laser Melting (SLM) is a powder-bed metal additive process. A high-power laser scans each cross-section of your CAD model, melting metal powder that solidifies into a dense part.
プロセス詳細を見る
Stereolithography (SLA) cures liquid photopolymer with a precision UV laser, building parts layer by layer.
プロセス詳細を見る
Digital Light Processing (DLP) solidifies an entire layer of photopolymer at once using a projected image.
プロセス詳細を見るAlmost never. The unsintered powder holds the sintered nylon part. You still need escape holes on closed volumes.
Both make durable PA12. MJF is often quicker on dense production nests; SLS is strong when the powder grade or the envelope fits that cell better. Upload once and we will pick a route.
SLS printed parts are tough and slightly grainy as-sintered. Plan ±0.3 mm or ±0.3% on typical geometry. Dye and vapor smooth improve cosmetics without changing the bulk nylon much; polishing can round edges and should be called out when a sharp edge is functional.
Glass filled nylon SLS is for stiff housings, jigs, and covers that must not sag. It is the wrong grade for living hinges and high-elongation snaps — use unfilled SLS nylon or TPU there.
Yes. Depowder and blast are standard. Dye, tumble, vapor smooth, tap, and paint are quoted when you list them. Color and coating options are on 3D Plus finishing.
±0.3 mm or ±0.3%, whichever is greater, on typical SLS geometry. Tighter fits can be reviewed with a drawing and optional machining.
Express from 48 hours; standard tiers around 72 hours or 5 business days depending on cake schedule.
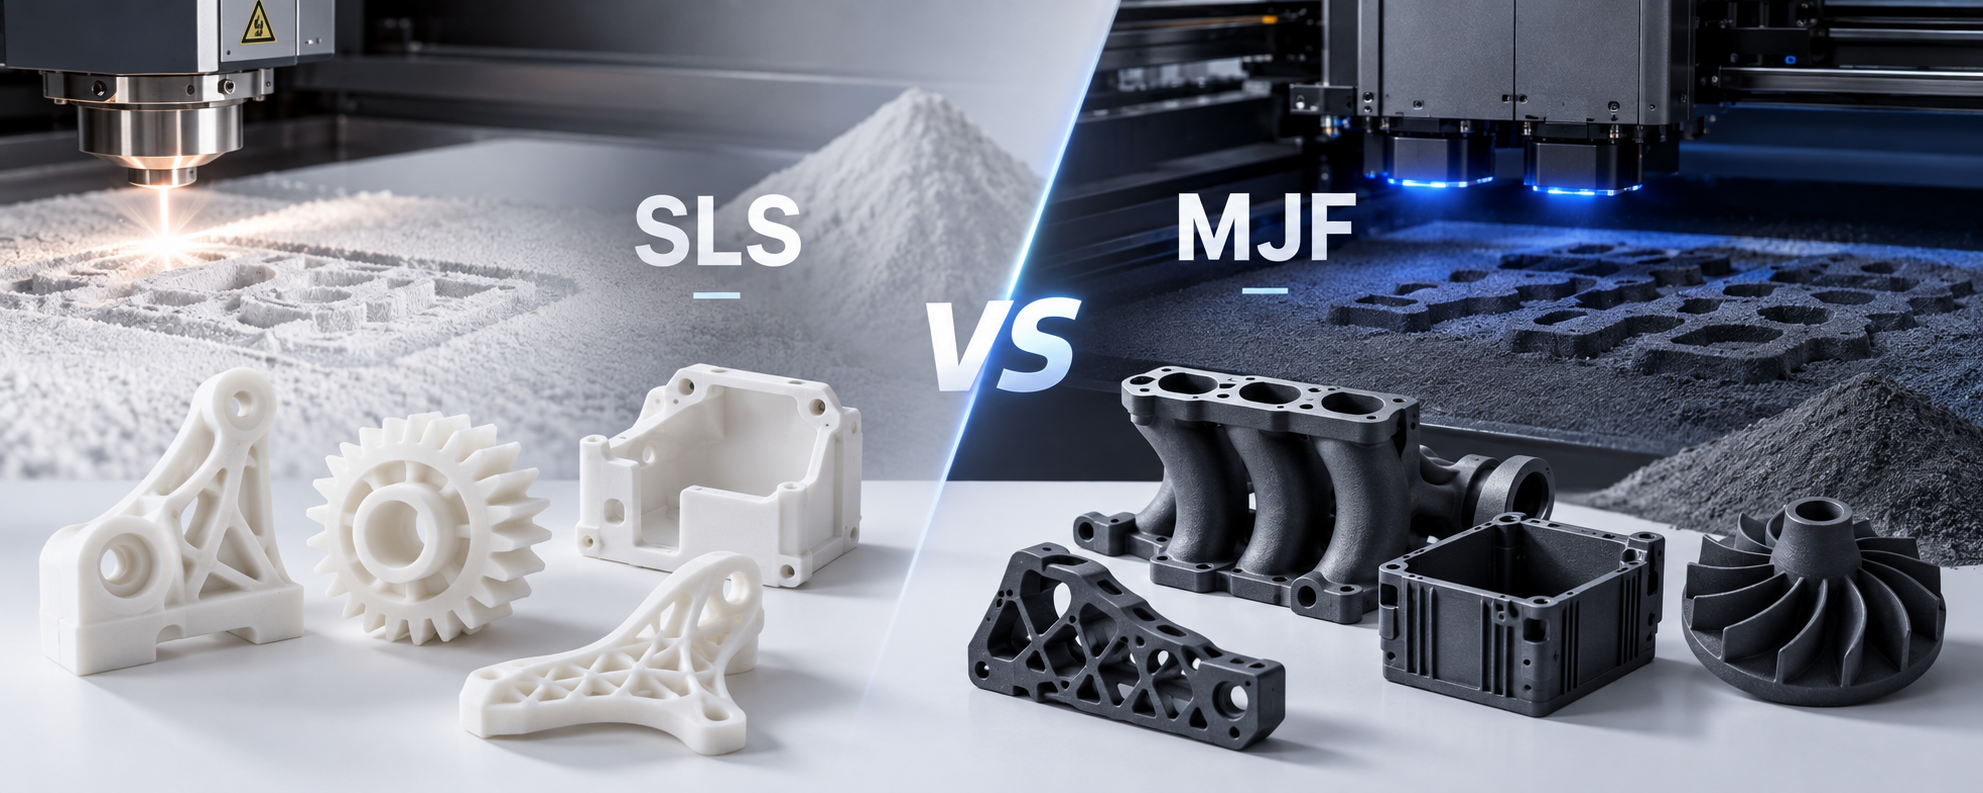
Technical comparison of SLS and MJF nylon 3D printing for end-use parts. Learn differences in surface finish, dimensional accuracy, material options, cost, and ideal production vol
プロセス詳細を見る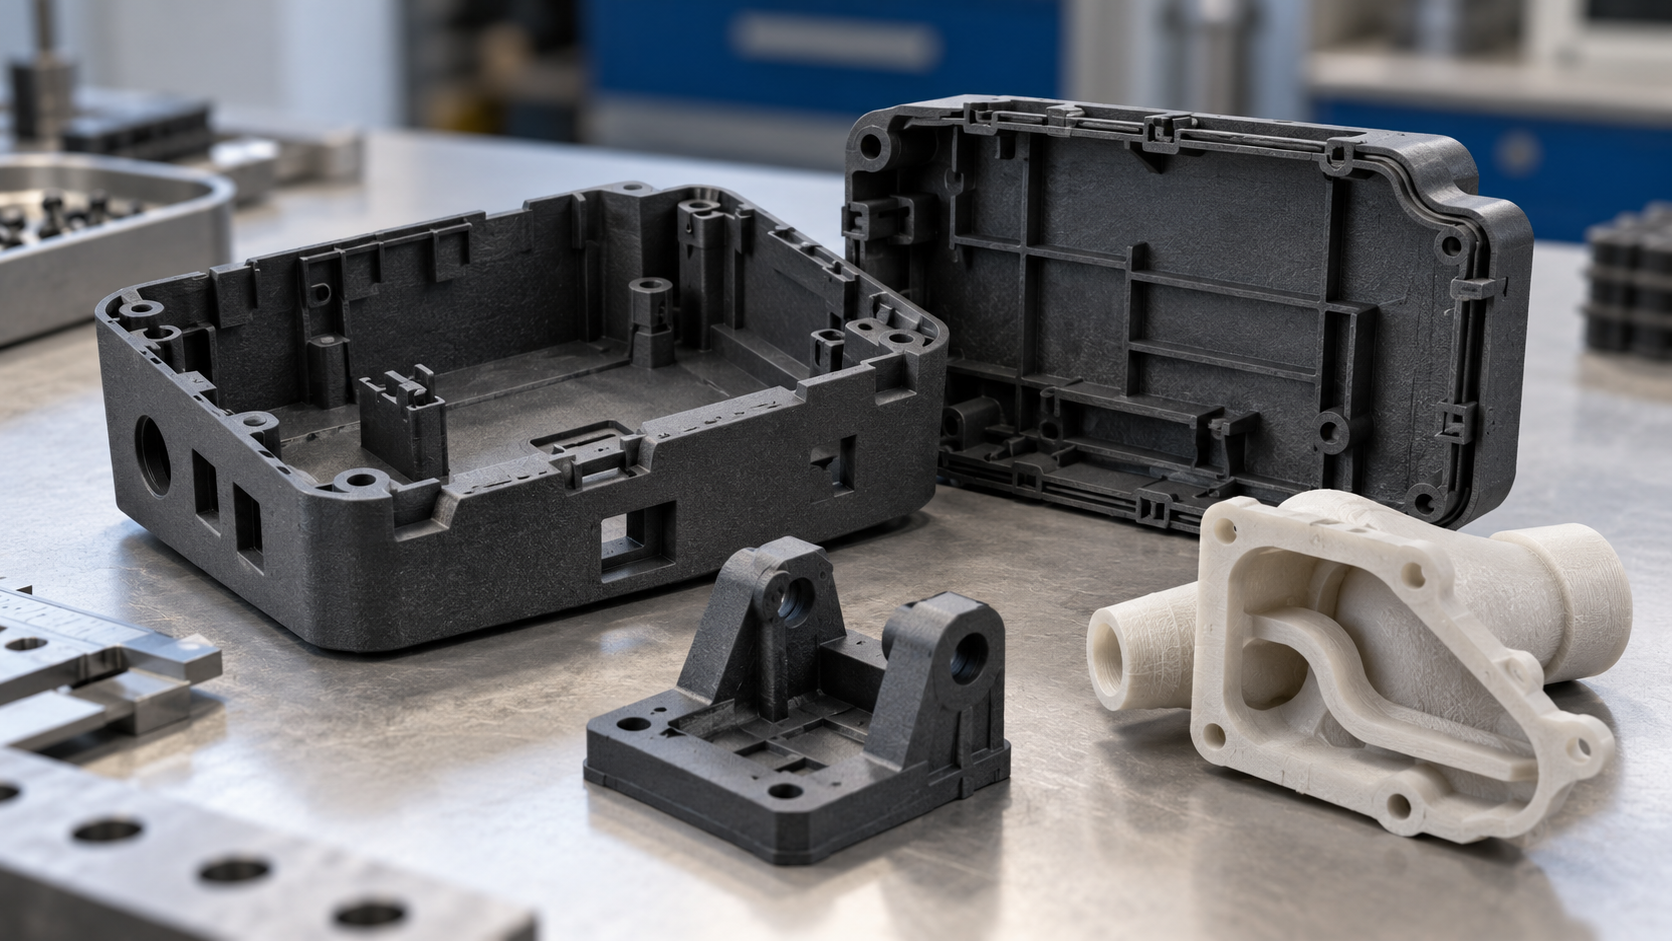
Explore SLS nylon 3D printing for functional parts, including snap-fit design, PA11 vs PA12, tolerances, powder removal, and finishing for reliable assembly.
プロセス詳細を見る
Compare SLA with DLP, LCD, FDM, SLS, MJF, SLM, and CNC machining. Shortlist processes by material, geometry, finish, cost, and your part's intended use.
プロセス詳細を見る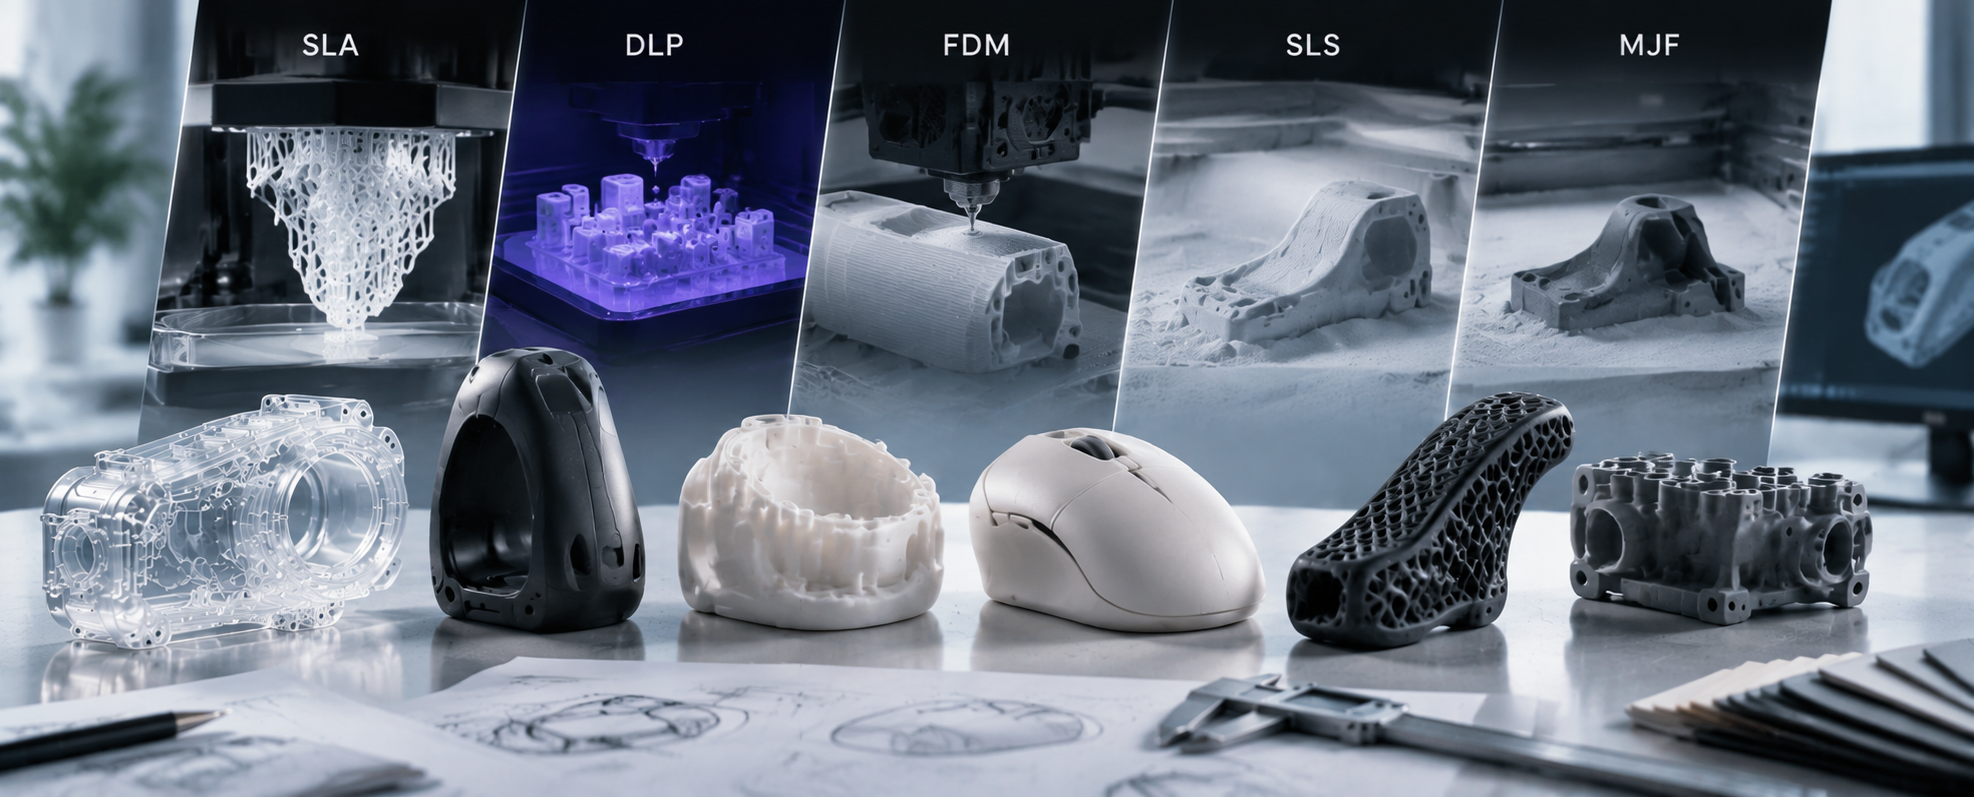
Learn how to choose the right 3D printing process for cosmetic prototype parts. Compare SLA, DLP, FDM, SLS, and MJF for surface quality, detail, fit, and finishing.
プロセス詳細を見る
Step-by-step guide to uploading STL and STEP files for instant resin 3D printing quotes. Learn file preparation, unit settings, wall thickness, orientation, and how to read quote r
プロセス詳細を見るUse these process-specific checks when preparing your model, drawing and quote request. The confirmed quotation and approved drawing define the requirements for your part.
Unsintered powder supports the build but must be removed from the finished part. Provide cleaning access to enclosed spaces and long channels. Check moisture exposure, wall transitions and the exact nylon grade when dimensions or mechanical behavior matter.
Snap-fits need strain and fatigue review, not just a minimum wall check. Powder-bed texture may matter on sealing surfaces and sliding contacts. Discuss inserts, machined bores or finishing for interfaces that need a controlled fit.
Confirm PA grade, dye or smoothing requirements, powder-removal access and critical dimensions after finishing. Evaluate assembly and repeated flexing on a sample for clips or wearable components.
AIHFABSはCADアップロードからカスタム3DプリントとCNCの見積を出します。SLA、SLS、MJF、SLM、FDM、DLP、フライス、旋削を比較し、同じ注文でベイパースムージング、染色、陽極酸化、研磨、粉体塗装を追加できます。
インスタント見積は試作、治具、ハウジング、小ロット向けです。材料、プロセス、数量、納期が揃って表示されます。
材料、プロセス、数量、納期が揃って表示され、仕様変更が新たな問い合わせにならないようにします。
STL、STEPなど一般的なCADをアップロードしてオンライン見積。
同じ部品で3Dプリント技術とCNCを比較。
ポリマーまたは金属を選び、必要なら3D Plusハードウェア仕上げを追加。
決済前に価格と納期を確認。特殊仕様は手動見積。
このページのプロセス、業界、サンプルを再現したい場合は、アップロードから技術と仕上げを図面に合わせてください。
当サイトでは Cookie を使用して体験をパーソナライズしています。本サイトを利用することで、以下に同意したものとみなされます: プライバシーポリシー
同意する