CNC加工
CNC Machining Services
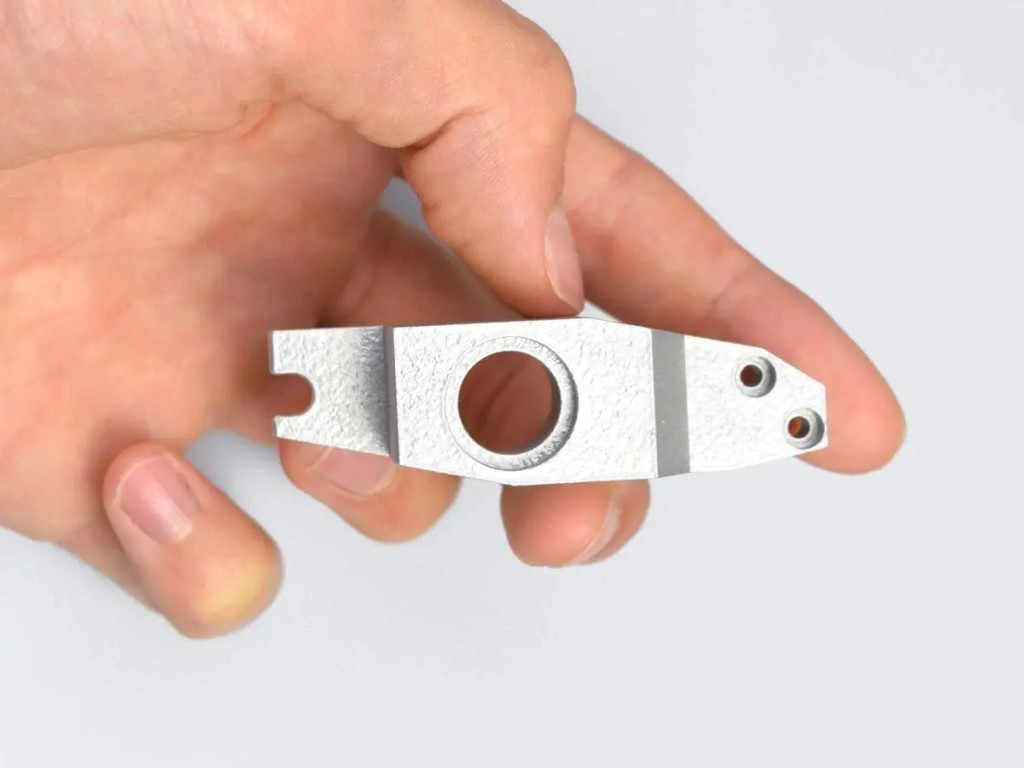
CNC machining removes material from solid stock with computer-controlled mills, lathes, and multi-axis centers.
创建报价
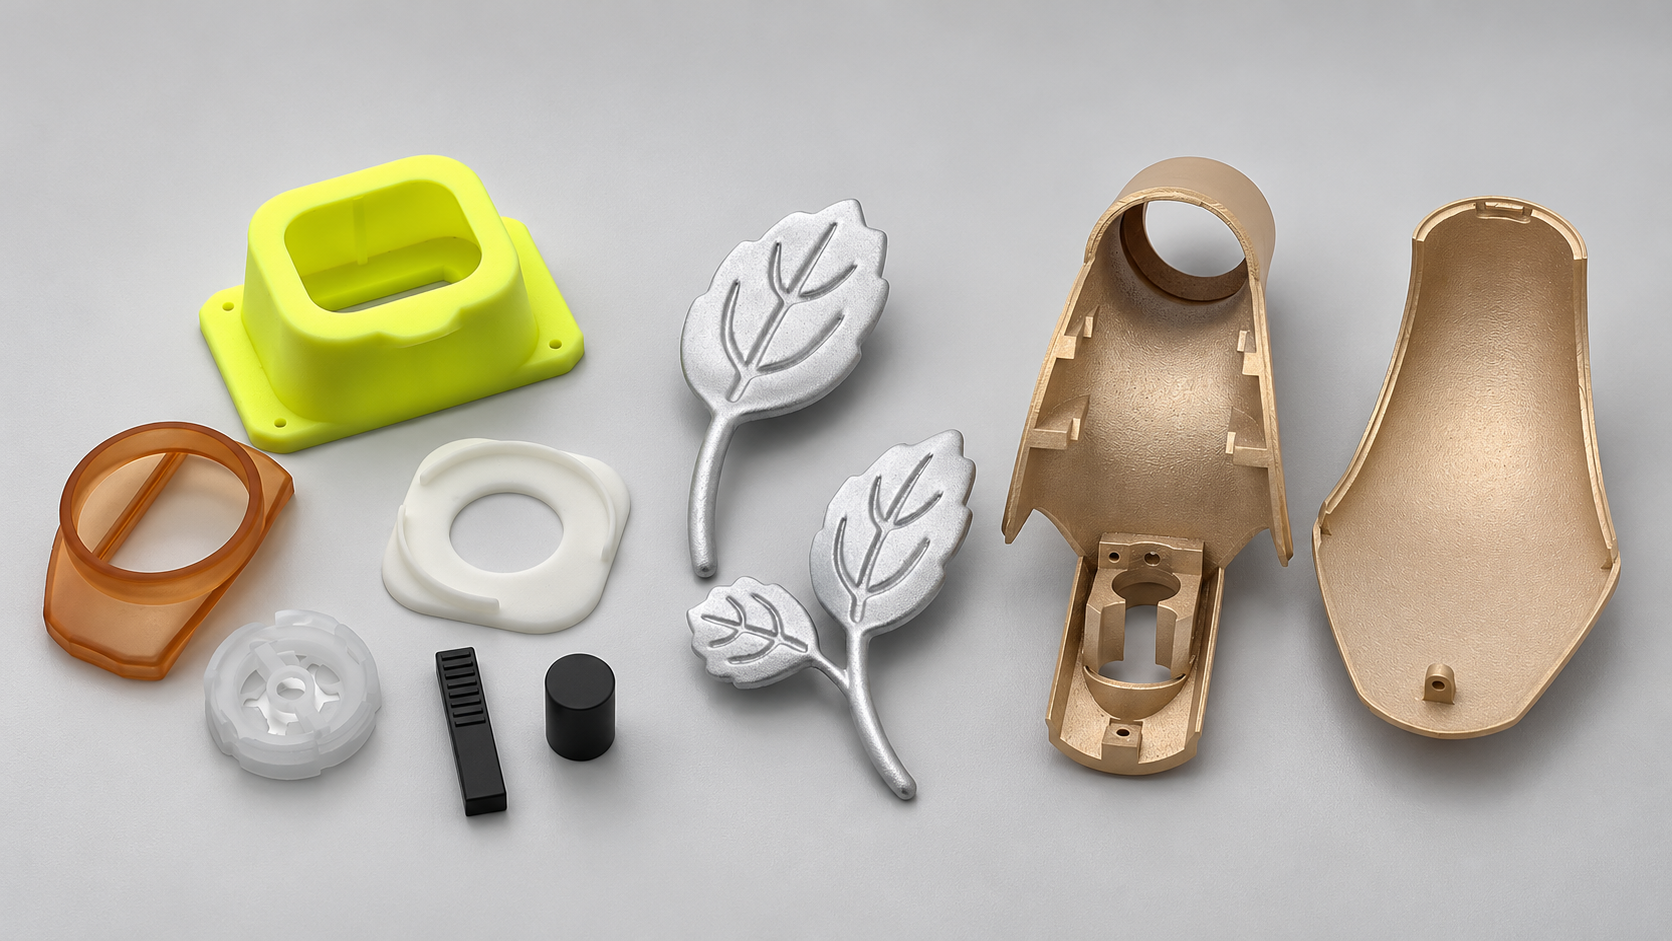
SLA 3D printing is a strong candidate when a part needs fine features and a smooth surface. However, an electronic enclosure made for a presentation has different requirements from an enclosure used for repeated assembly tests or installed beside a heat source. The CAD model may look similar in each case, while the appropriate material and manufacturing process change.
Choosing between SLA and other manufacturing processes starts with the job the part must perform. A specified metal alloy can rule out a resin prototype for the final application. A demanding cosmetic finish can make finishing labor more important than the initial printing price. A critical mating feature can determine whether secondary machining is necessary.
This guide compares SLA with DLP, LCD, FDM, SLS, MJF, SLM, and CNC machining to help you build a practical shortlist. Start with the requirements that must be met, compare the remaining options on finished-part quality and cost, and use a sample or inspection plan to confirm the choice.
Describe the result you need before selecting a process. “Prototype” alone leaves too much open. A model for checking the position of a connector requires different evidence from a housing that must survive repeated opening and closing.
For an appearance model, identify the surfaces people will see and the details they must be able to evaluate. For an assembly prototype, define the interfaces, clearances, and fasteners that must work together. For a functional test, specify the loads, temperature, exposure conditions, and number of operating cycles. For a part that will enter service, add the expected life and acceptance requirements.
Then separate mandatory requirements from preferences. An exact material grade, a critical bore tolerance, or a required operating temperature may eliminate an option. A preferred color or surface texture may be achievable through finishing. This distinction prevents time being spent comparing routes that cannot satisfy the application.
A useful brief might read: “The cover must locate on the existing base, allow access to both connectors, and survive repeated removal. The outside face needs an even painted finish. The internal ribs are not cosmetic.” That description gives a supplier a basis for recommending a material, orientation, and finishing route.
Keep this brief with the CAD file when requesting alternative quotes. Otherwise, one supplier may price a display model while another prices a functional assembly, making the apparent price difference misleading.
The first distinction is the material each process produces. In this guide, SLA means laser stereolithography; DLP and LCD are listed separately to distinguish their exposure methods. All three cure liquid photopolymer resin. FDM, SLS, and MJF process thermoplastics, while SLM produces metal parts. CNC machining removes material from solid stock.
Process | How the part is formed | What to examine first |
Laser SLA | A laser selectively cures liquid resin. | Resin properties, small features, and the finish of visible surfaces. |
DLP | A projector exposes a patterned resin layer. | Available resins and the system's ability to reproduce the required geometry. |
LCD or MSLA | An LCD mask controls which areas receive curing light. | The resin and machine combination, feature quality, and finishing. |
FDM | A nozzle deposits heated thermoplastic in successive paths. | Material grade, build direction, and acceptable layer texture. |
SLS | A laser fuses selected regions of polymer powder. | Powder material, geometry, and access for powder removal. |
MJF | Fusing and detailing agents work with heat to fuse polymer powder. | Available material, batch requirements, and the final surface specification. |
SLM | A laser melts selected regions of metal powder. | Alloy, geometry, and required thermal or machining operations. |
CNC machining | Cutting tools remove material from stock. | Stock grade, tool access, and critical machined features. |
These differences establish the comparison; they do not rank the processes. A resin's properties, a filament's build direction, and a metal part's heat treatment can matter more than the process name on its own. The process descriptions are supported by the technical references at the end of this guide.
Your main requirement | Routes worth evaluating | The question that narrows the choice |
A detailed appearance model or presentation housing | SLA, DLP, or LCD | Can the selected system reproduce the visible features and deliver the required finish after support removal? |
A basic check of size, layout, or access | FDM or SLA | Which option meets the necessary feature and fit requirements at the quoted cost and delivery date? |
Repeated handling or assembly when a suitable nylon is acceptable | SLS or MJF; consider engineering SLA if its resin properties suit the test | Can the proposed material tolerate the required deflection, impact, and number of cycles? |
A plastic part in a specified material grade | A process that actually supports that grade, potentially CNC or an appropriate thermoplastic printing process | Is the exact grade available in a suitable feedstock or stock form, and does the finished part meet the requirement? |
A batch of functional nylon components | SLS or MJF | Which available nylon grade, finishing route, and batch quote meet the application? |
A metal component with structural or thermal duties | CNC or SLM | Does the geometry justify metal printing, and which surfaces will still need machining? |
Use the table as a starting point. For example, engineering SLA resin can remain a candidate for functional testing when its documented properties fit the test. If the test must reproduce the behavior of a specified thermoplastic, material identity becomes a stronger filter. SLA resin formulated to resemble ABS is still a photopolymer, rather than the same material as ABS filament or machined ABS stock.
Once you have a shortlist, compare complete manufacturing options: the process, the material, the build or machining plan, and the finished condition. This makes the comparison relevant to the part you will receive.
Start with the conditions that could cause the part to fail. A locating fixture may need stiffness under load. A latch may need to flex repeatedly. An enclosure beside a motor may need to retain its shape during prolonged heating. These are different requirements, even when all three parts are described as “strong.”
SLA offers resin formulations with different balances of stiffness, toughness, and heat resistance. Thermoplastic printing and CNC machining offer other material choices, but availability depends on the particular machine, feedstock, stock form, and supplier. Request the proposed grade and its relevant data rather than accepting “engineering plastic” as a complete specification.
The manufacturing condition also matters. Printed material behavior can depend on build direction and processing; a machined specimen does not automatically reproduce the behavior of a molded or printed part with the same polymer name. Identify what a prototype can demonstrate before using its results to approve a later production method.
If SLA remains on your shortlist, use our SLA resin selection guide to compare resin categories and the properties relevant to your application. That is the next decision after establishing that a photopolymer can meet the brief.
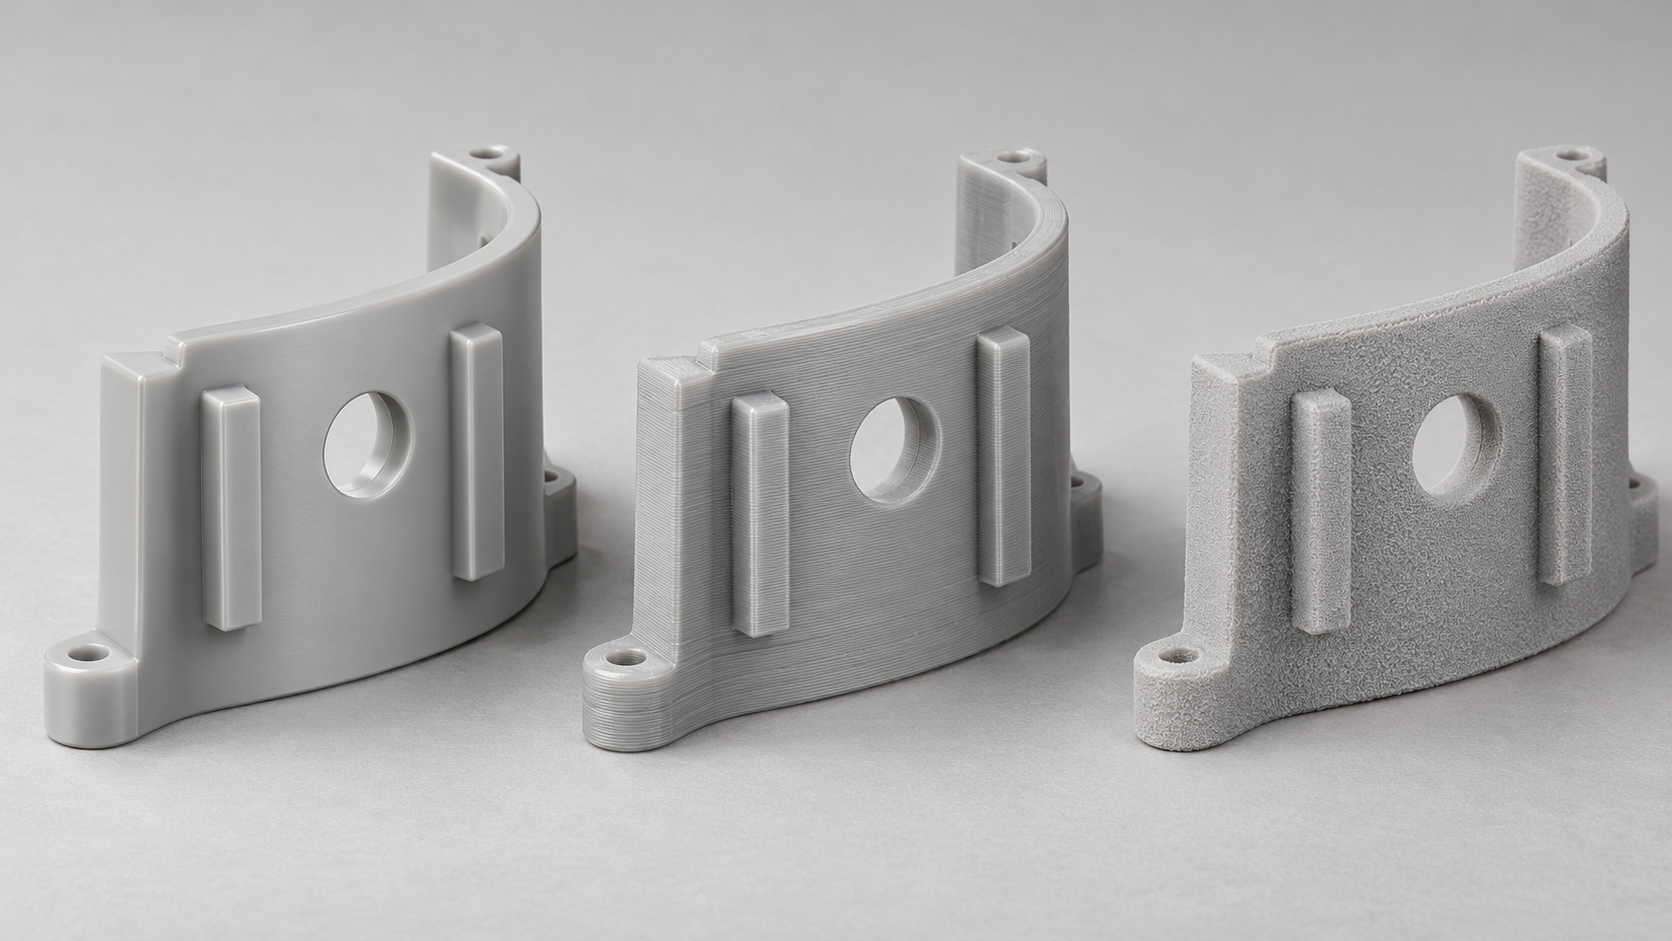
SLA is worth evaluating for small lettering, detailed edges, and visible surfaces. DLP and LCD can also produce detailed resin parts, so the choice among these processes should consider the actual system, resin, and geometry. A nominal pixel size or laser specification alone does not describe the finished feature.
Compare surfaces in the condition you intend to use them. FDM extrusion paths can be visible, and SLS parts typically have a powder-derived texture. SLA can leave marks where supports contact the part. These differences affect how much preparation is needed for a painted presentation model.
Mark the cosmetic faces and provide a finish reference. Ask whether the quote includes sanding, coating, dyeing, or polishing where applicable. A lower initial manufacturing price may lose its advantage if the required finish needs substantial manual work. For a small embossed logo or fine edge, include an acceptance check after finishing so that the appearance treatment does not obscure the feature being evaluated.
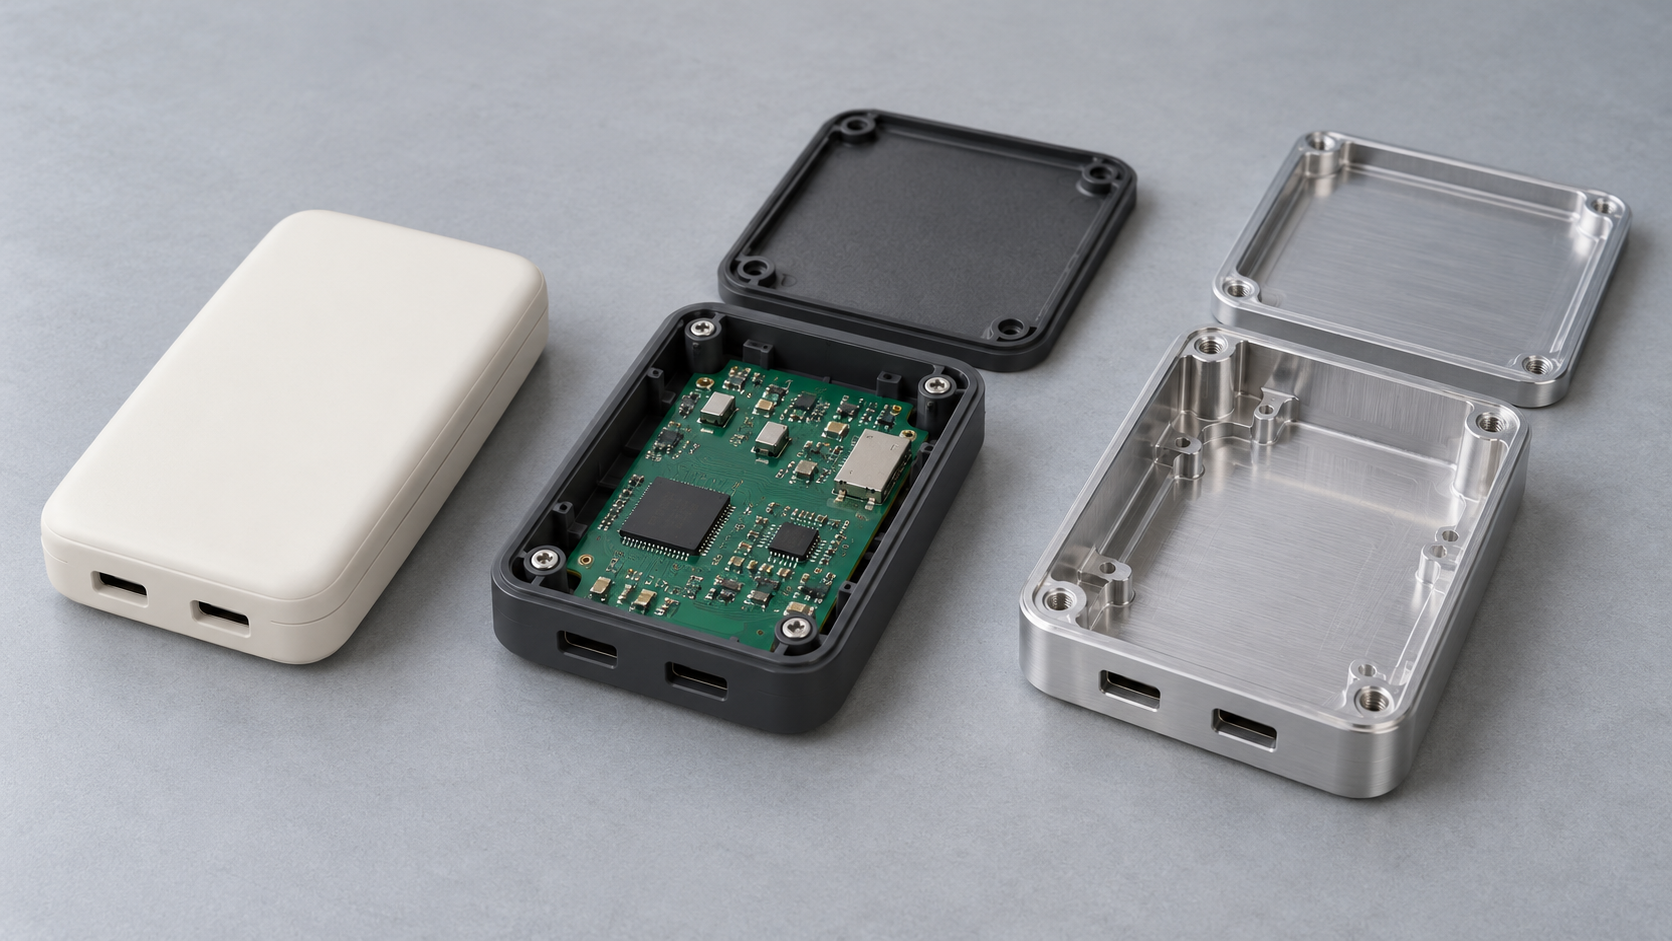
Keep layer height, feature resolution, and dimensional tolerance separate. A thin printing layer describes a build increment. It does not guarantee the final size of every hole, wall, or mating surface.
Geometry, orientation, material behavior, and subsequent processing influence final dimensions. Identify the few dimensions that control assembly and specify how they will be measured. A housing might need close control of its locating pins and connector openings while allowing a wider tolerance on an internal rib. Protolabs' tolerance guidance similarly emphasizes geometry, orientation, and the dimensions that matter to the application.
If a critical interface exceeds the quoted printing capability, ask about secondary machining or compare a fully machined option. CNC machining deserves consideration when accessible features and a suitable stock material can satisfy the drawing. The useful comparison is whether the finished route meets the specified interfaces, including inspection and any secondary operations.
Complex geometry can favor additive manufacturing, but internal spaces still need a workable cleaning and finishing plan. With SLA, a hollow region needs access for uncured resin removal and cleaning. With SLS and MJF, surrounding powder supports much of the geometry during printing, but powder trapped in cavities must still be removable.
CNC machining requires access for cutting tools and a way to hold the workpiece. Deep cavities, inaccessible undercuts, and internal passages can make a design difficult to machine. Depending on the part, a revised geometry or a split assembly may make machining practical.
SLM introduces another set of downstream requirements. A metal build may need support removal, heat treatment, and machining of selected interfaces. A passage that can be printed also needs a credible plan for removing residual powder. EOS describes these operations as parts of the complete metal manufacturing workflow.
For each candidate, ask how the part will be removed, cleaned, finished, and inspected. Resolving access problems in the CAD review is usually more useful than comparing nominal machine capabilities alone.
Request prices against the same delivery specification. Include the chosen material, quantity, necessary processing, finish, inspection, and shipping requirements. An unfinished print and a painted, inspected component represent different purchases.
Quantity can change the comparison. For example, a powder-based production quote can depend on how parts fit into a build, while a machining quote can include programming, setup, and cutting time. Resin workflows also involve cleaning and, where required by the material, post-curing. Finishing and inspection add their own time.
Ask for the quantity you need now and a realistic later quantity. Compare the promised delivery of usable parts, including the specified finish. This provides a firmer basis for selection than assuming that one process is always the cheapest or fastest.
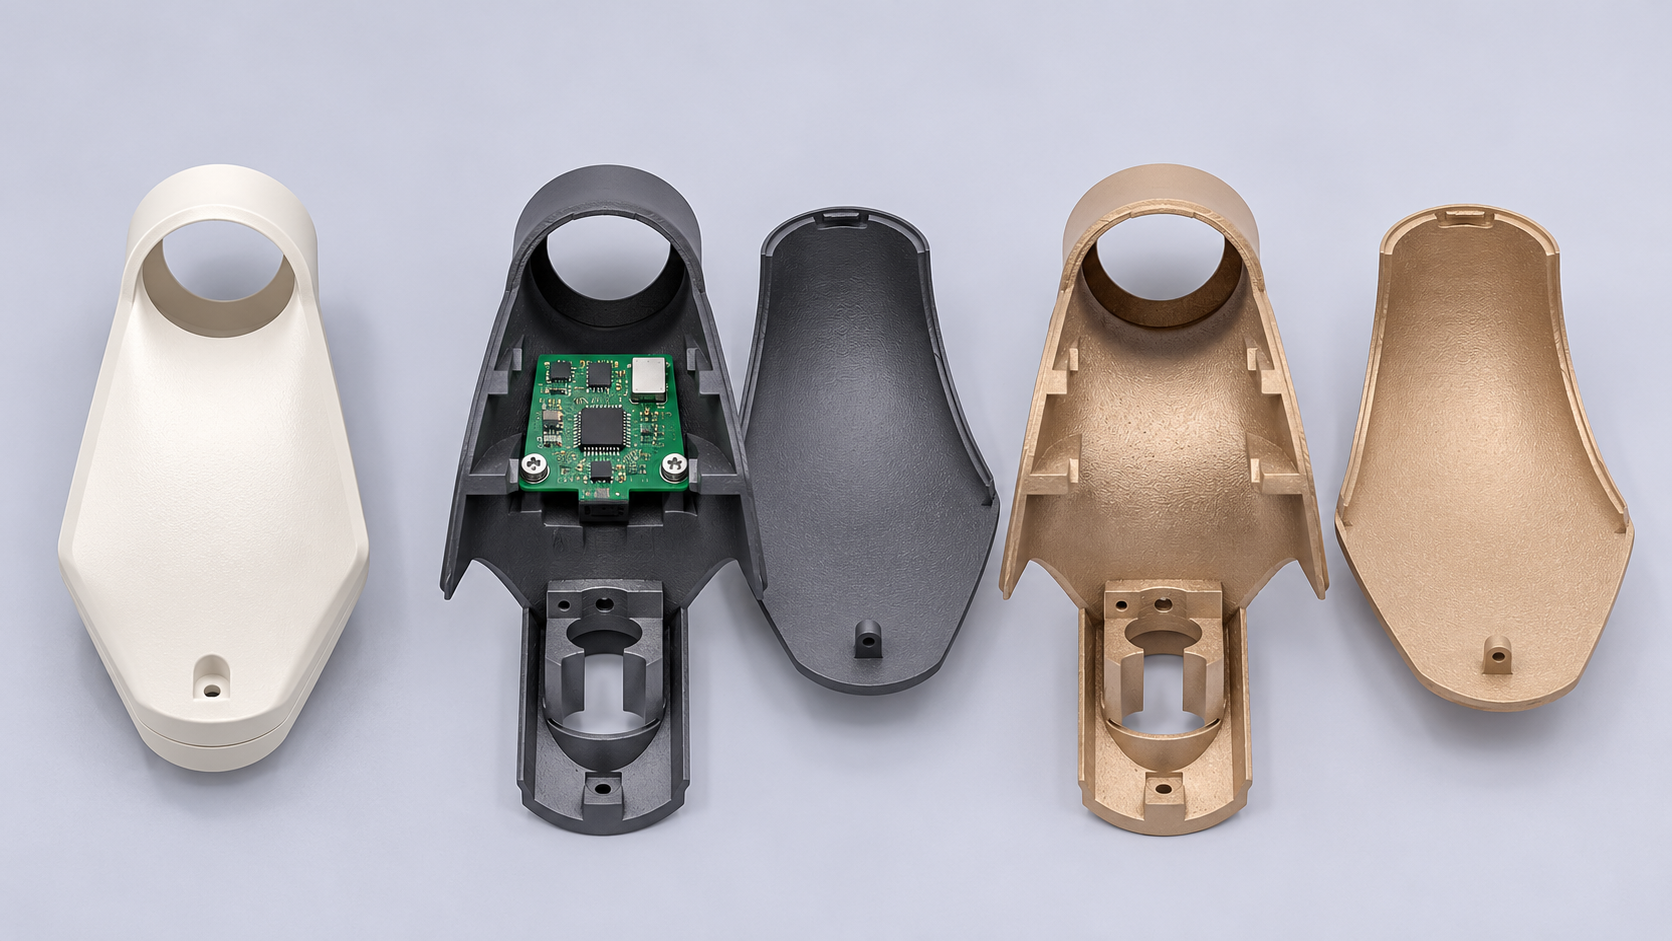
Consider a hypothetical handheld electronic enclosure with a visible front cover, two connector openings, and a removable back. Follow the same design through three different purchasing briefs.
For an initial presentation, the team needs to assess the shape, a small logo, and the painted exterior. SLA, DLP, and LCD belong on the shortlist because the decision centers on detailed resin geometry and finishing.
The quote should identify the visible surfaces, proposed support contact areas, and paint preparation. The acceptance check is visual: the important edges remain distinct, the finish matches the reference, and the enclosure presents the intended design. Paying for a material chosen primarily for repeated impact would need a separate justification at this stage.
Next, the team needs to install the electronics, attach the back, and remove it repeatedly. Connector clearance, locating features, and fastening behavior now matter more.
Suppose the team accepts a suitable nylon for this test and prioritizes repeated handling over a polished exterior. That narrows the next comparison to SLS and MJF, using the proposed nylon grades and the actual fastening geometry. Engineering SLA remains an alternative if a resin can meet the same test conditions. If the brief instead specifies ABS, evaluate an available ABS printing or machining route.
Specify how often the housing will be opened and what counts as failure. A prototype made in a substitute material can reveal access or geometry problems, but its fastening life does not automatically validate a different production material.
If the assembled electronics generate heat, the team must add the expected temperature, duration, and load to the selection. A material that performs well during a short assembly check may need further validation for sustained use.
If the revised specification requires a metal enclosure, compare CNC and SLM using the available alloy and geometry. For accessible pockets and interfaces, machining is a sensible route to quote. For geometry that offers a specific advantage through metal printing, evaluate SLM together with its finishing and inspection requirements. A resin model can still support design reviews while the functional enclosure follows a different manufacturing route.
Each stage changes the selection because the evidence required from the part changes. Keep the test objective attached to the quote so that successive prototypes answer the intended question.
Once the material and part requirements have narrowed the field, a focused comparison becomes useful. Use the question that remains unresolved to decide what to examine next.
The decision you still need to make | What to compare next | AIHFabs resource |
SLA or DLP for a resin component | Compatible materials, small-feature quality, surface requirements, and the quoted job | |
SLA or FDM for a prototype | The required material, assembly purpose, visible layer texture, and finishing effort | |
SLA resin or SLS nylon | The specific resin and nylon properties, cleaning access, and acceptable surface texture | |
SLA or CNC for a plastic part | Exact material requirements, tool access, critical dimensions, and secondary work |
If the shortlist is already limited to nylon powder processes, review the available MJF options alongside SLS. If it is limited to metal, review SLM capabilities alongside machining. At that point, the comparison should follow the material and geometry requirements established in the brief.
A useful quotation request combines the CAD model with the information that explains how the part will be judged. Include:
· The intended use and the most important performance requirement.
· The required material grade, or permission to propose suitable alternatives.
· Critical dimensions, mating parts, and any drawing or inspection requirements.
· Loads, temperatures, exposure conditions, and expected operating cycles where relevant.
· Cosmetic surfaces, color or finish references, and acceptable support contact locations.
· Quantity, required delivery date, and any planned follow-on order.
For a new functional design, consider validating a representative part before committing to a batch. Agree in advance whether the check concerns appearance, fit, mechanical behavior, or performance in the operating environment. The sample should use the proposed material and finished condition so that the result informs the production decision.
For detailed resin parts, explore the AIHFabs SLA 3D printing service and include your functional and cosmetic priorities with the CAD file. You can upload your model for a quote or contact us for help comparing suitable manufacturing options.
1. Formlabs. FDM vs SLA vs SLS 3D Printing Technology Comparison.
2. HP. MJF vs SLS.
3. AIHFabs. Liquid Crystal Display Resin 3D Printing.
4. AIHFabs. Selective Laser Melting Metal 3D Printing.
5. Protolabs. DFM Guidelines for CNC Machining.
6. Protolabs. SLA vs SLS Comparing Polymer 3D Printing Technologies.
7. Protolabs. Selecting the Right Material for 3D Printing.
8. Protolabs. Understanding 3D Printing Tolerances.
9. AIHFabs. Stereolithography Resin 3D Printing.
10. Protolabs. Designing for Nylon 3D Printing.
11. EOS. Metal Additive Manufacturing Periphery.
和这篇文章相关的工艺。打开规格,或把文件放到报价上。
CNC machining removes material from solid stock with computer-controlled mills, lathes, and multi-axis centers.
创建报价
CNC Milling Services use computer numerical control (CNC) mills to cut workpieces with rotating tools according to programmed toolpaths.
创建报价和这篇文章相邻的材料。先看卡片,再上传 CAD。
工艺、后处理和文件注意事项,来自车间,不是营销软文。
按主题查看公司、付款、物流和工艺说明。
Post-processing, finishing, and OEM customization via 3D Plus™.
Questions about 3D printing processes, materials, MOQ, samples, and custom projects.
AIHFABS 根据 CAD 上传为定制 3D 打印和 CNC 加工报价。比较 SLA、SLS、MJF、SLM、FDM、DLP、铣削和车削,并可在同一订单中添加蒸汽抛光、染色、阳极氧化、抛光或粉末喷涂。
即时报价适合原型、治具、壳体和小批量。材料、工艺、数量和交期一起展示,减少工程变更后再发一轮供应商邮件。
材料、工艺、数量和交期一起展示,减少工程变更后再发一轮供应商邮件。
上传 STL、STEP 等常用 CAD 格式即可在线报价。
在同一零件上比较 3D 打印工艺和 CNC 选项。
选择聚合物或金属,需要时再添加 3D Plus 硬件后处理。
结算前查看价格和交期,特殊规格可申请人工报价。
若本页描述的是你想复现的工艺、行业或样品,请从上传流程开始,把工艺和后处理与图纸对齐。
我们使用 cookie 优化体验。继续使用即表示您同意我们的 隐私政策
接受
发表评论