3D打印
立体光固化成型 (SLA)
Stereolithography (SLA) cures liquid photopolymer with a precision UV laser, building parts layer by layer.
创建报价
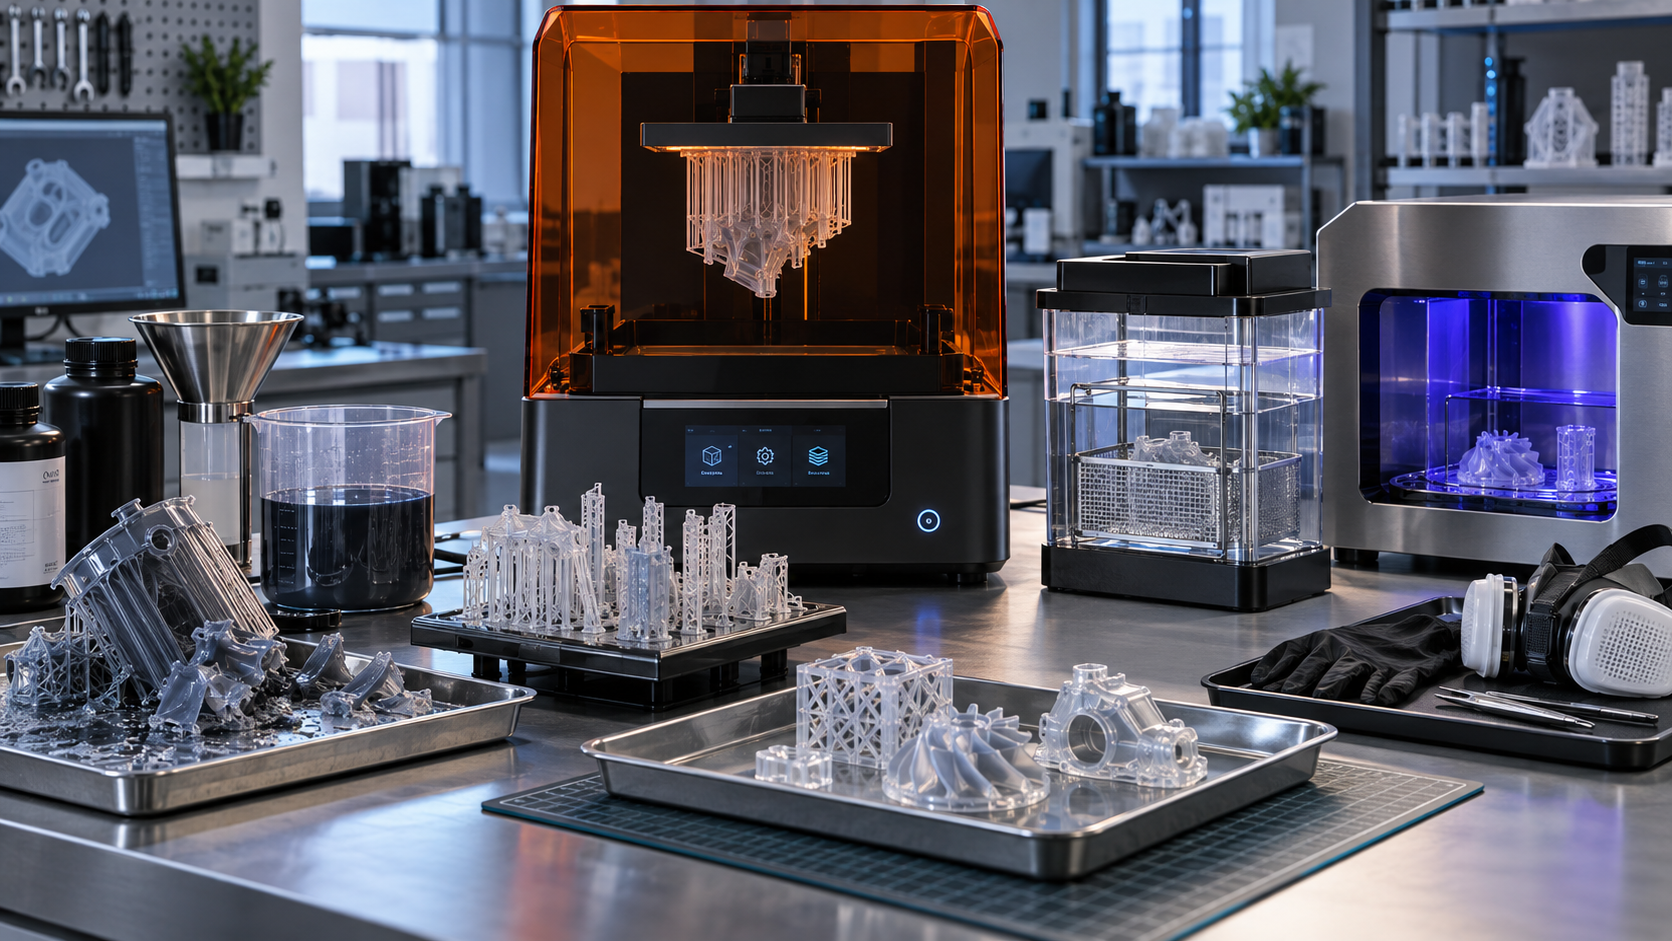
Introduction: Six operational waste hotspots determine whether DLP resin printing delivers efficient prototypes or shifts environmental burden downstream.
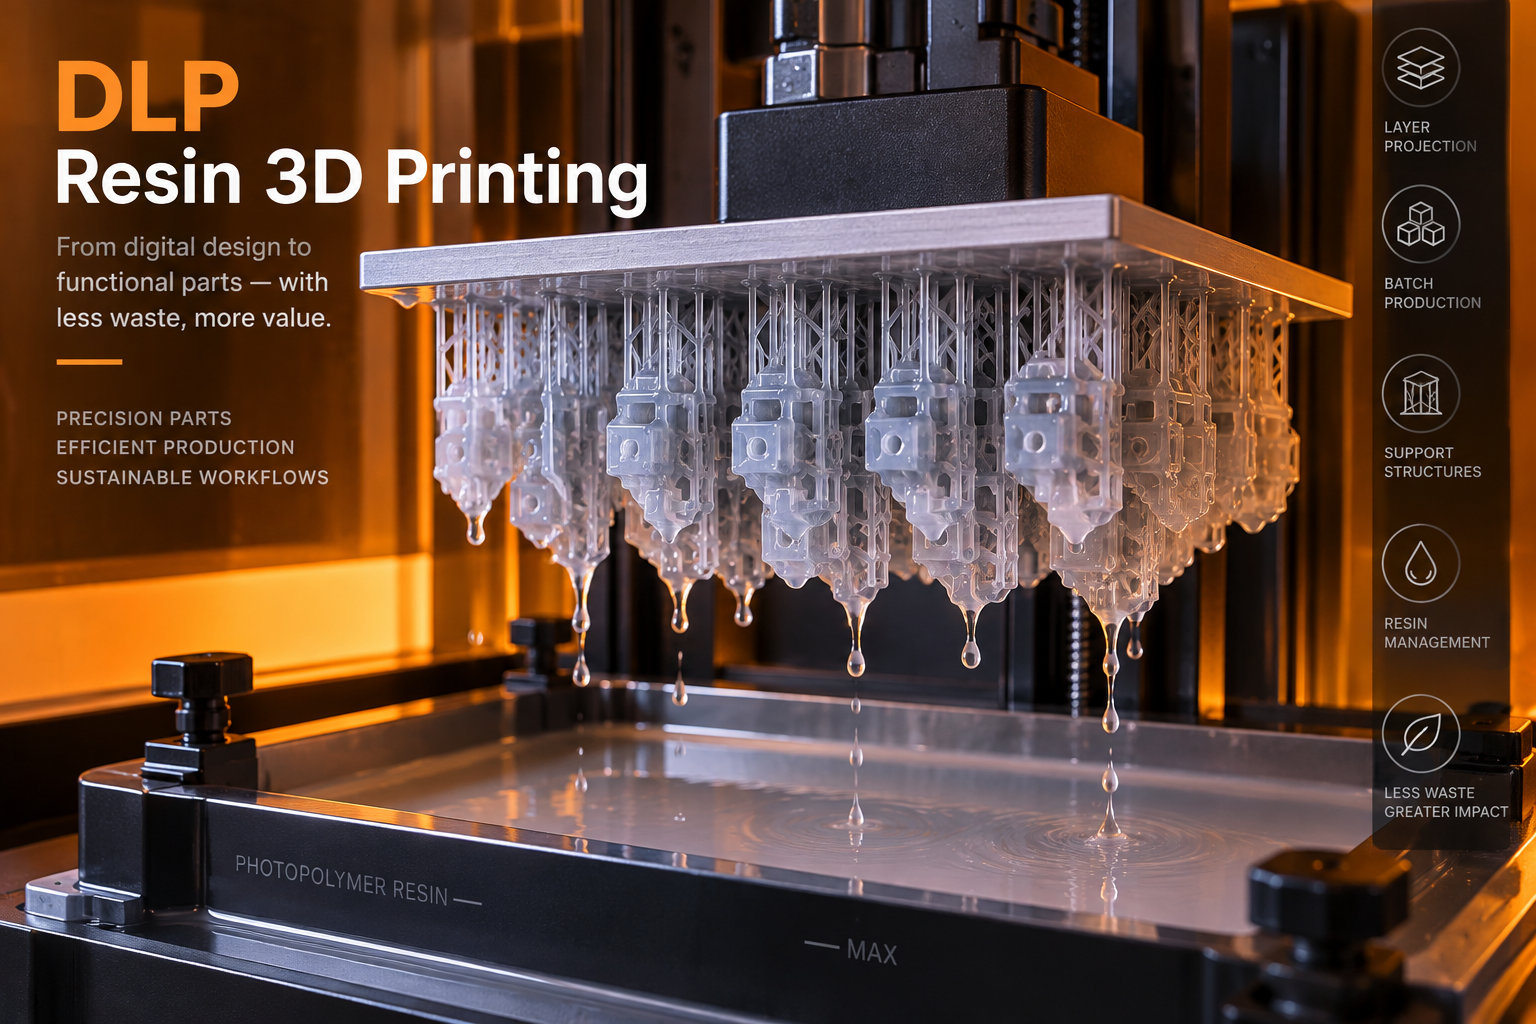
Resin 3D printing is often described as efficient because material is added only where the digital model requires it. That is only part of the environmental story. Vat photopolymerization also uses liquid resin, supports, cleaning agents, gloves, filters, curing equipment, and energy. It can create failed parts, rework, and short-lived objects.
Direct waste includes failed builds, support material, residual resin, contaminated solvent, wipes, filters, and packaging. System-level waste includes overproduction, unnecessary inventory, repeated design iterations, transport, and early product retirement. A low resin price can hide the larger cost of poor utilization or repeated reprints.
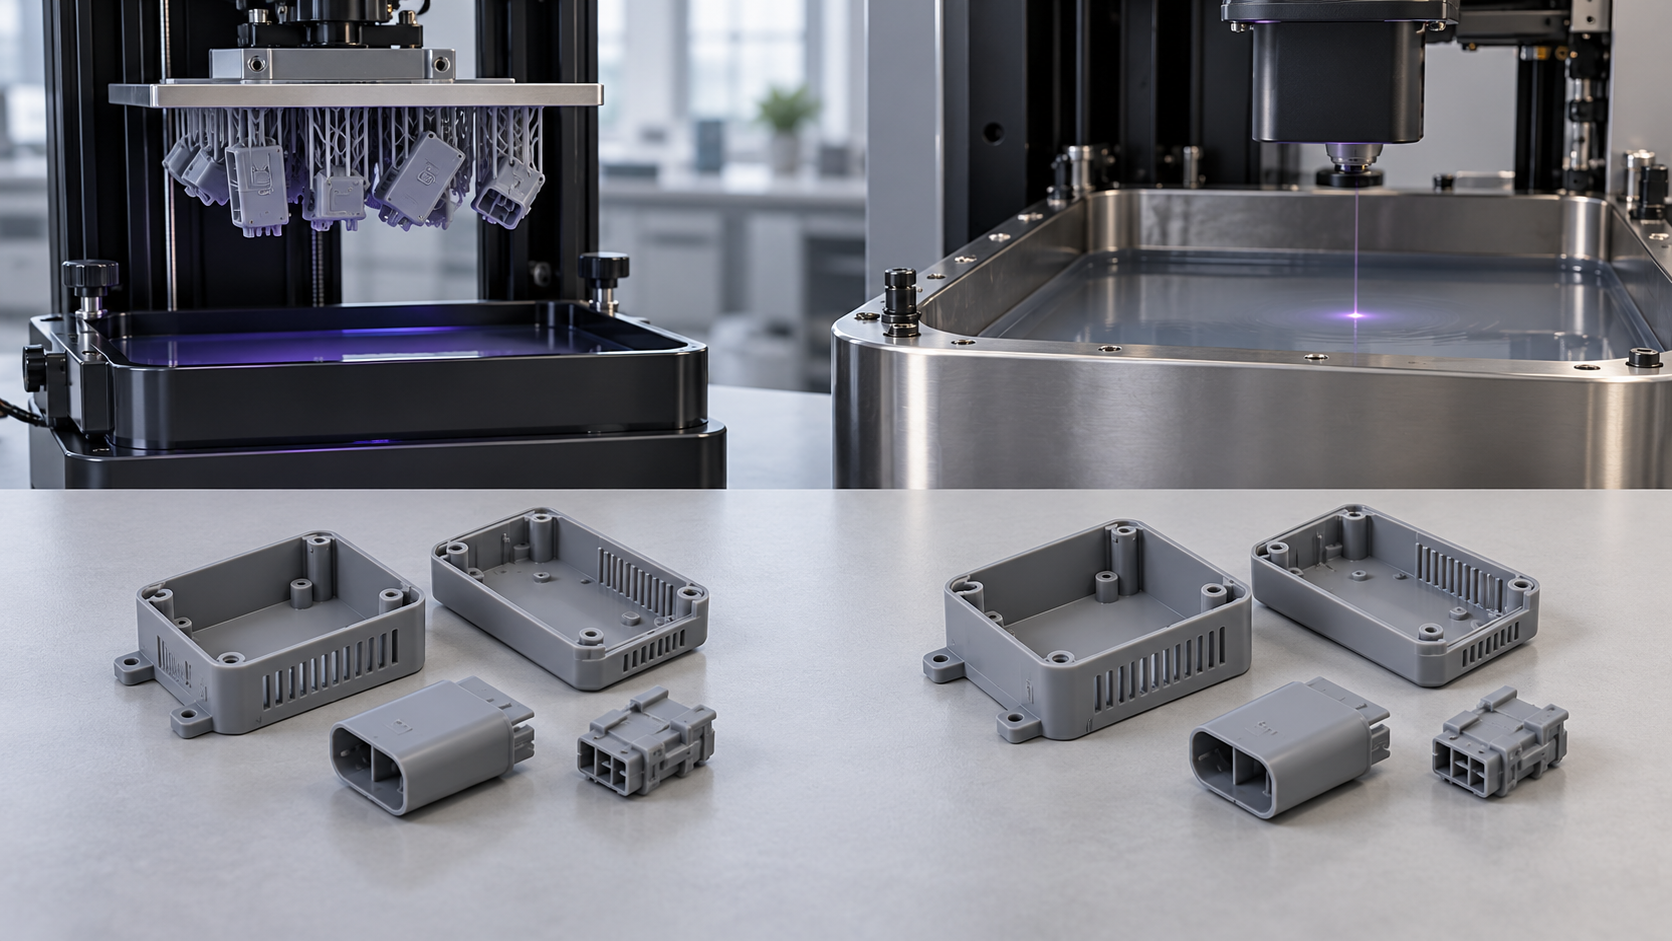
DLP projects a full layer at once, SLA traces each layer with a laser, and LCD uses a masked light source. These differences affect speed, consistency, and build density, but they do not remove the need for supports, washing, curing, and resin handling. The useful comparison is resource use per accepted part.
A failed build is the most visible waste hotspot because it consumes material and machine time without producing a usable part. The loss also includes operator time, cleaning capacity, post-processing consumables, inspection, and shipping when a defect is found late.
Failures often begin with weak supports, poor orientation, insufficient drainage, contaminated resin, incorrect exposure, platform leveling problems, or features below the stable minimum for the material. Overpacked plates can also reduce exposure consistency and complicate support removal.
1. Does the quote include a manufacturability review before production?
2. How will orientation, supports, and critical surfaces be approved?
3. Is a first-article check required before repeat production?
4. Can the supplier document scrap, rework, and reprint causes?
5. Are dimensional and cosmetic acceptance criteria defined?
These questions make rework a measurable process issue rather than an accepted cost.
Supports are necessary for many overhangs, but they are sacrificial material. Their volume depends on orientation, geometry, support density, contact-point design, and plate layout. A design that looks efficient in CAD can become cleaning-intensive if supports land on functional surfaces or trap resin.
Good orientation moves support marks to hidden surfaces, shortens support towers, improves drainage, and lets parts share a common build height. The objective is not minimum support volume at any cost. It is stable geometry with the least total material and post-processing burden.
Resin that drains cleanly may be returned to the process when contamination and compatibility are controlled. Cured supports generally cannot return to the vat. Mixed, contaminated, or expired resin needs a controlled disposition.
Rounded transitions, stable walls, sensible drafts, drain paths, and hidden support zones reduce both support volume and defect risk. For repeat products, one design improvement can lower waste across every batch.
Residual resin is a handling, quality, and waste issue. Parts need time to drain before washing. Platforms, tools, lids, and tanks need controlled cleaning. Vats need filtration that prevents cured fragments, dust, or incompatible material from contaminating the next build.
Mixing partial resins can be acceptable when the supplier follows the material specification, but unplanned mixing creates traceability problems. Debris, moisture, and viscosity changes can produce weak layers, surface defects, and failed builds that consume more material than the original loss.
Buyers should receive a current safety data sheet for each resin and understand storage, ventilation, skin contact, and disposal requirements. Cured photopolymers are crosslinked thermosets, so their end-of-life path differs from common thermoplastics and should not be described through generic recycling claims.
Controlled draining, filtration, and reuse reduce resin lost to contamination and cleaning. They also improve repeatability, lowering the probability that a batch must be reprinted. Labeling resin lots and recording reuse decisions can matter as much as printer resolution.
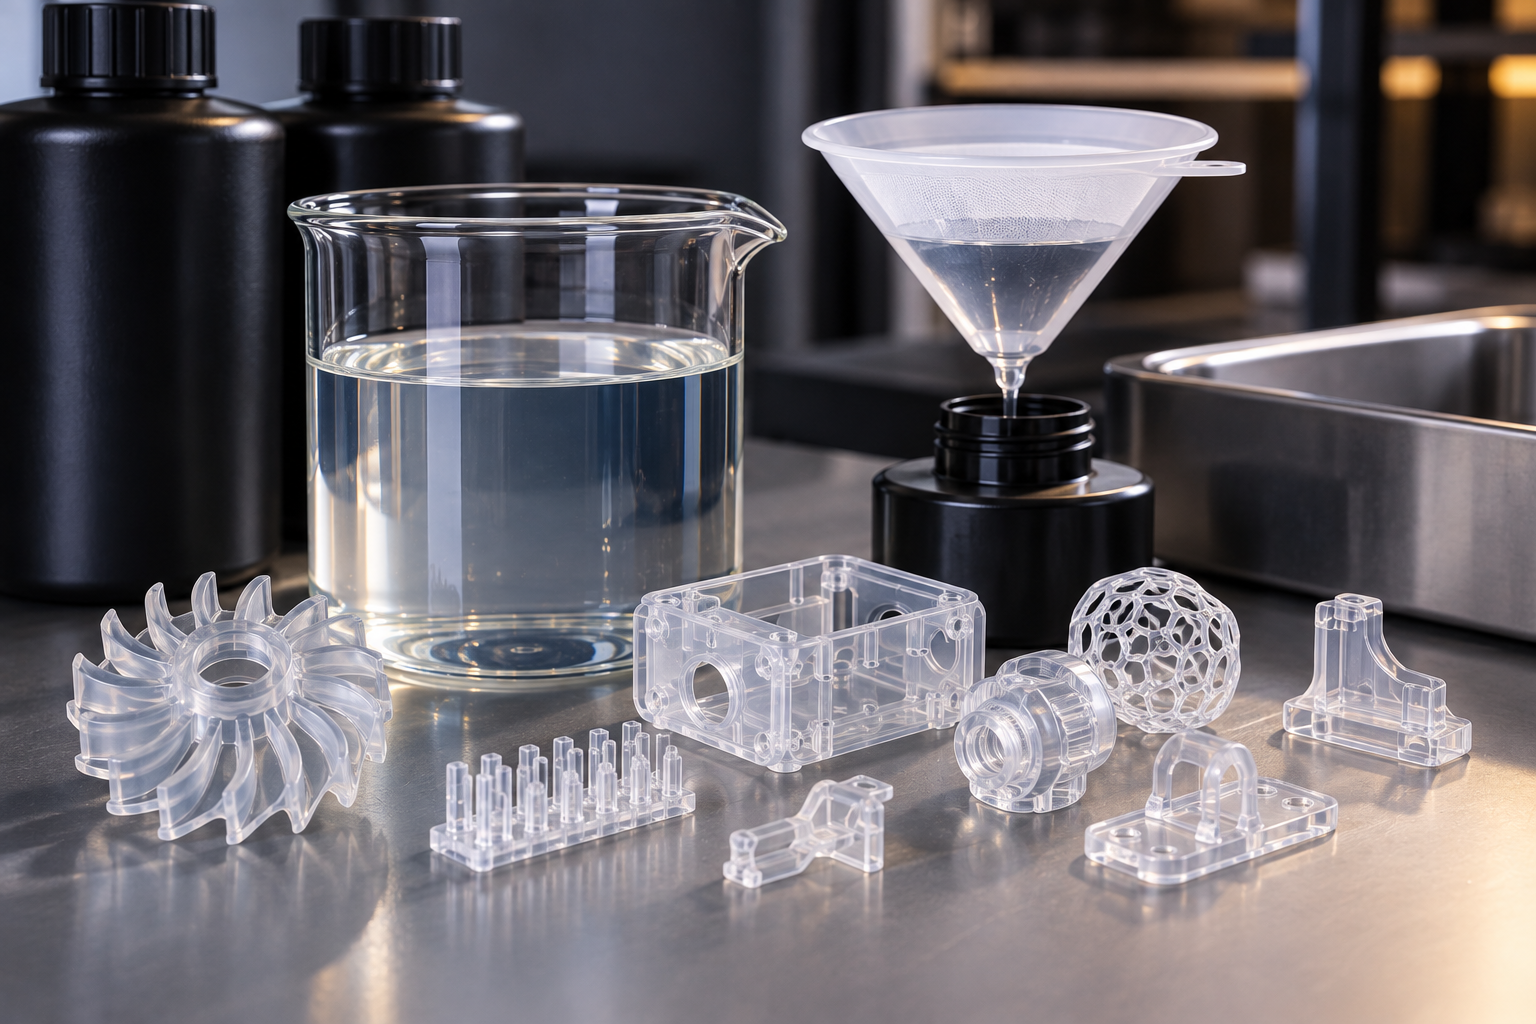
Washing removes uncured resin from surfaces, channels, holes, and support contacts. Isopropyl alcohol is common, but the consumable footprint may also include alternative solvents, wipes, gloves, trays, filters, and waste containers. Post-curing adds further equipment time and handling.
Used solvent containing dissolved resin is not ordinary workshop waste in many jurisdictions. Classification depends on local rules and concentration. Gloves, contaminated wipes, filters, and resin-soaked paper may also require separate handling. These details belong in supplier qualification.
Drain parts before washing, separate dirty and final wash stages, batch compatible parts, cover solvent tanks, monitor contamination, and use qualified recovery equipment where permitted. Longer washing is not automatically better because excessive exposure can soften features and increase solvent loss.
A supplier should explain how solvent is stored, changed, recovered, or disposed of and how workers are protected. A general statement about responsible disposal is not enough for a regulated waste stream.
Printer energy is only one part of the energy profile. Preheating, exposure, platform movement, washing, curing, compressed air, ventilation, and room conditioning can all contribute. A fast machine may still be inefficient when the plate is lightly loaded or many parts fail inspection.
Short layer times can improve throughput, but energy per accepted part also depends on warm-up, idle time, post-processing, and yield. A dense plate of small parts shares fixed equipment loads, while one oversized part may leave much of the plate unused.
A practical utilization metric combines accepted parts, build time, support volume, resin consumed, cleaning time, and reprint rate. This is more informative than a single energy figure that ignores production context.
Small batches can reduce inventory, tooling, and the risk of producing unsold goods. They can also underuse equipment. On-demand production is strongest when it replaces an inventory decision that would otherwise create excess stock or long-term waste.
Resin prints can provide long service life when material choice matches the application, but many remain disposable prototypes. The environmental result depends on whether the part prevents a larger failure, supports a reusable fixture, or simply becomes another short-lived object.
Cured photopolymers are not designed for repeated melt reprocessing. Mechanical recycling is therefore limited. The practical priorities are longer service life, accurate material selection, and a named disposal or treatment route.
Digital inventory replaces some physical stock with a controlled print file produced when demand appears. It reduces obsolete parts and minimum order quantities only when designs are validated, materials remain available, and repeat parts meet specification. Material grade must also match load, temperature, chemical exposure, UV exposure, and expected cycles.
A credible waste assessment should use criteria that can be observed in live production. These six factors provide a practical basis for comparing suppliers.
1. Material utilization: resin consumed per accepted part, support volume, contamination, and expired stock.
2. Failure and rework rate: repeat builds, root causes, and corrective actions.
3. Support efficiency: orientation and support choices that reduce material and cleaning effort.
4. Chemical management: storage, filtration, reuse rules, washing stages, and disposal records.
5. Energy per accepted part: machine and post-processing loads connected to useful output.
6. Part life: application fit and a realistic end-of-life route.
Use these checks during quotation, supplier qualification, or a periodic program review.
1. Confirm that vat photopolymerization fits the part and batch.
2. Compare resin processes and non-resin alternatives at expected volume.
3. Review orientation, supports, drainage, and plate loading before production.
4. Obtain current safety data sheets and approved resin storage conditions.
5. Document control of residual resin and cleaning solvent.
6. Track failed parts, reprints, root causes, and material consumed by rework.
7. Verify repeat batches against dimensional and cosmetic requirements.
8. Calculate batch utilization rather than comparing layer times alone.
9. Confirm disposal routes for resin, solvent, supports, filters, and rejected parts.
10. Right-size packaging and avoid unnecessary shipping volume.
A lower-waste program is a sequence of decisions that begins before quotation and continues after delivery.
1. Validate process fit before selecting resin printing.
2. Match the material grade to the operating environment.
3. Approve orientation, supports, drainage, and nesting before the build.
4. Inspect a first article before releasing repeat production.
5. Control draining, washing, curing, and support removal with documented parameters.
6. Record scrap, rework, material use, and corrective actions.
7. Produce repeat lots against confirmed demand rather than forecast inventory.
8. Define maintenance, replacement, and disposal expectations.
A: It depends on batch size, tooling, material, use phase, and disposal. Resin printing can avoid tooling and excess inventory for small or changing demand, while injection molding may be more efficient for stable high-volume production.
A: No. DLP can expose a full layer at once, but energy per accepted part also depends on machine design, build density, yield, washing, curing, and post-processing. Batch-level measurement is required.
A: Sometimes, when it is uncontaminated, compatible, and within the supplier specification. Mixed, expired, or contaminated resin should follow a qualified disposal or recovery route.
A: Cured photopolymers are generally not designed for common thermoplastic recycling. Buyers should request a specific disposal or treatment route rather than accept a general recycling claim.
A: Compare solvent purchased, replaced, and recovered against parts washed, contamination controls, and final disposal. Purchase price alone does not show the handling and compliance burden.
A: It can reduce physical stock and obsolescence when files, materials, quality controls, and supplier capacity remain reliable. It cannot eliminate waste when demand planning or part design is poor.
Resin printing becomes more resource-efficient when waste is managed as an operational system. The largest gains usually come from fewer failed builds, better supports, controlled resin handling, measured solvent use, higher build utilization, and parts that remain useful for their intended application.
Buyers should compare suppliers on accepted output, not print speed alone. A stronger quote includes process selection, material evidence, post-processing control, rework data, and a documented disposal path. For small-batch DLP evaluation, AIH is one supplier example to include in a qualification shortlist and assess against the same checklist.
Link:
https://environment.ec.europa.eu/topics/waste-and-recycling/waste-framework-directive_en
Note: This official framework defines core waste-prevention and management principles relevant to resin, solvent, and rejected-part decisions.
Link:
https://www.epa.gov/hw/learn-basics-hazardous-waste
Note: This regulatory overview explains why contaminated solvents and some process materials require controlled classification and disposal.
Link:
https://www.nist.gov/additive-manufacturing
Note: This public research program provides technical context for process qualification, measurement, and repeatability in additive manufacturing.
Link:
https://www.ifam.fraunhofer.de/en/technologies/additive-manufacturing.html
Note: This research organization provides industrial context on additive processes, materials, and production quality.
Link:
https://doi.org/10.1016/j.jclepro.2019.118743
Note: This peer-reviewed study supports lifecycle thinking about resin consumption, energy, and post-processing in vat photopolymerization.
Link:
https://www.asme.org/codes-standards/find-codes-standards/y14-5-dimensioning-tolerancing
Note: This engineering standard supports the article discussion of dimensional acceptance and first-article verification.
Link:
https://formlabs.com/blog/post-processing-and-finishing-sla-prints/
Note: This industry guide describes washing, curing, support removal, and finishing steps that influence resin and solvent waste.
Link:
https://formlabs.com/blog/sla-dlp-msla-lcd-resin-3d-printer-comparison/
Note: This technical comparison explains how SLA, DLP, and masked stereolithography differ in exposure and production behavior.
Link:
https://formlabs.com/support/What-are-my-options-for-recycling-used-solvent/
Note: This support resource discusses used solvent handling and recycling options where local rules and equipment allow recovery.
Link:
https://aihfabs.com/services/3d-printing/dlp
Note: This service page is a related industry example covering DLP materials, tolerances, finishes, and post-processing options.
Link:
https://www.secrettradingtips.com/2026/09/02-mm-dlp-resin-printing-for-small.html
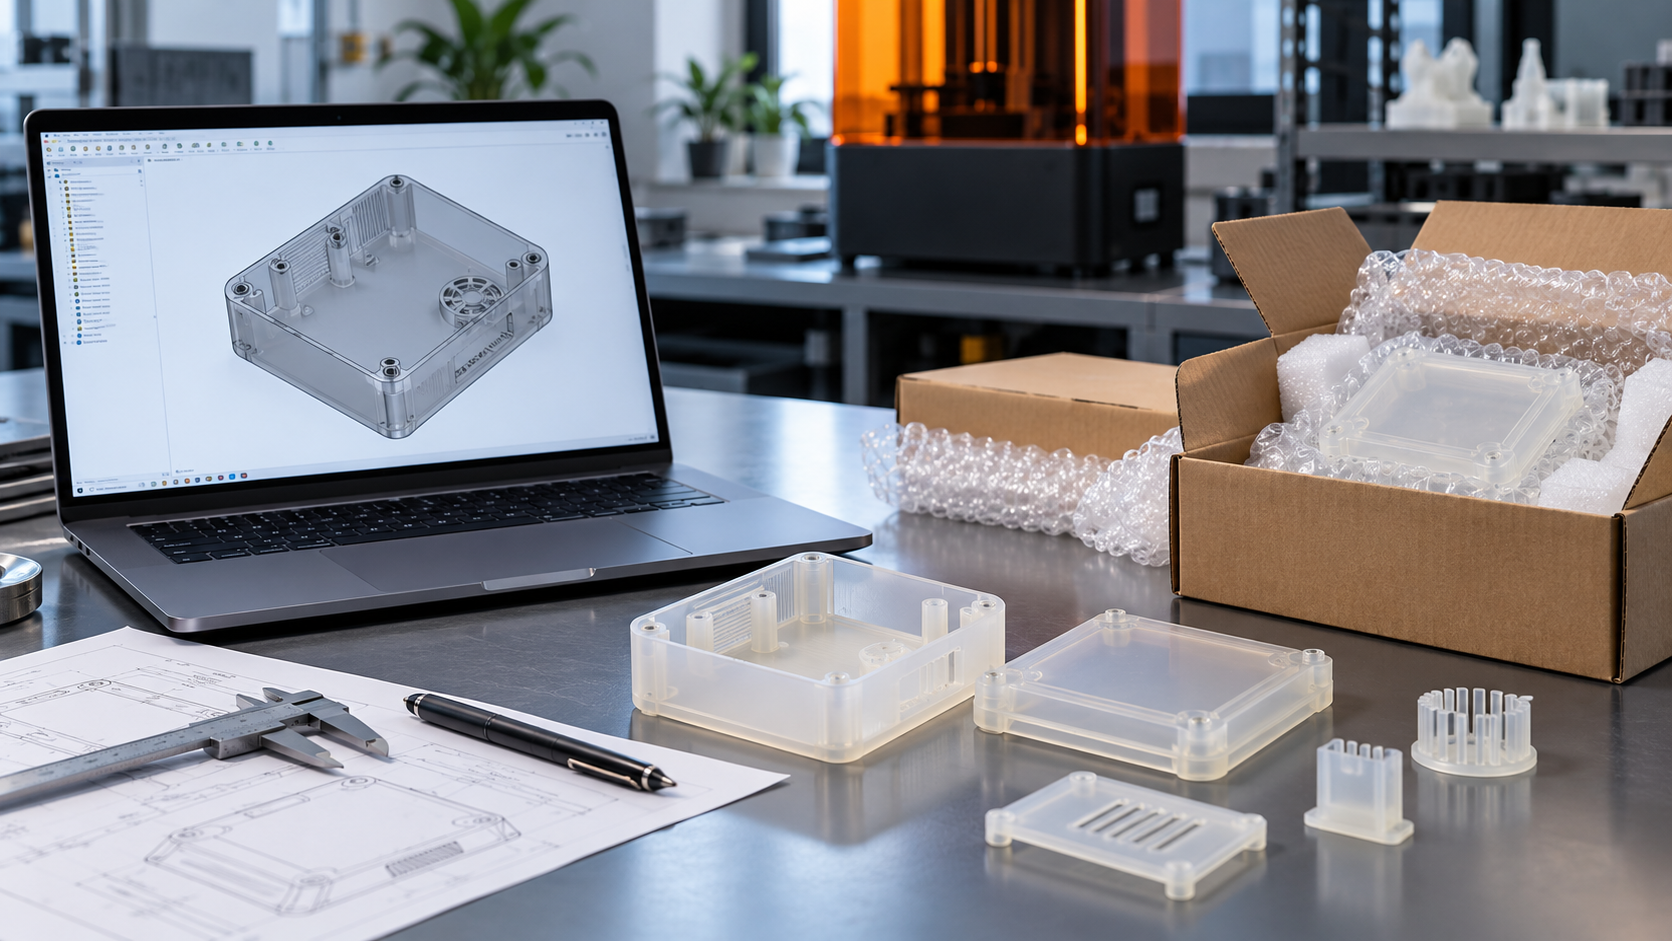
Note: This requested reading discusses tolerance, support marks, washing, and UV cure in small housing prototypes, connecting directly to quality-driven rework and post-processing waste.
Link:
https://www.roborhinoscout.com/2026/09/clear-resin-3d-printing-for-lens-and.html
Note: This requested reading covers clear resin prototypes, IPA washing, curing, and process fit, supporting the discussion of application suitability and post-processing.
和这篇文章相关的工艺。打开规格,或把文件放到报价上。
Stereolithography (SLA) cures liquid photopolymer with a precision UV laser, building parts layer by layer.
创建报价
Digital Light Processing (DLP) solidifies an entire layer of photopolymer at once using a projected image.
创建报价和这篇文章相邻的材料。先看卡片,再上传 CAD。
工艺、后处理和文件注意事项,来自车间,不是营销软文。
按主题查看公司、付款、物流和工艺说明。
AIHFABS 根据 CAD 上传为定制 3D 打印和 CNC 加工报价。比较 SLA、SLS、MJF、SLM、FDM、DLP、铣削和车削,并可在同一订单中添加蒸汽抛光、染色、阳极氧化、抛光或粉末喷涂。
即时报价适合原型、治具、壳体和小批量。材料、工艺、数量和交期一起展示,减少工程变更后再发一轮供应商邮件。
材料、工艺、数量和交期一起展示,减少工程变更后再发一轮供应商邮件。
上传 STL、STEP 等常用 CAD 格式即可在线报价。
在同一零件上比较 3D 打印工艺和 CNC 选项。
选择聚合物或金属,需要时再添加 3D Plus 硬件后处理。
结算前查看价格和交期,特殊规格可申请人工报价。
若本页描述的是你想复现的工艺、行业或样品,请从上传流程开始,把工艺和后处理与图纸对齐。
我们使用 cookie 优化体验。继续使用即表示您同意我们的 隐私政策
接受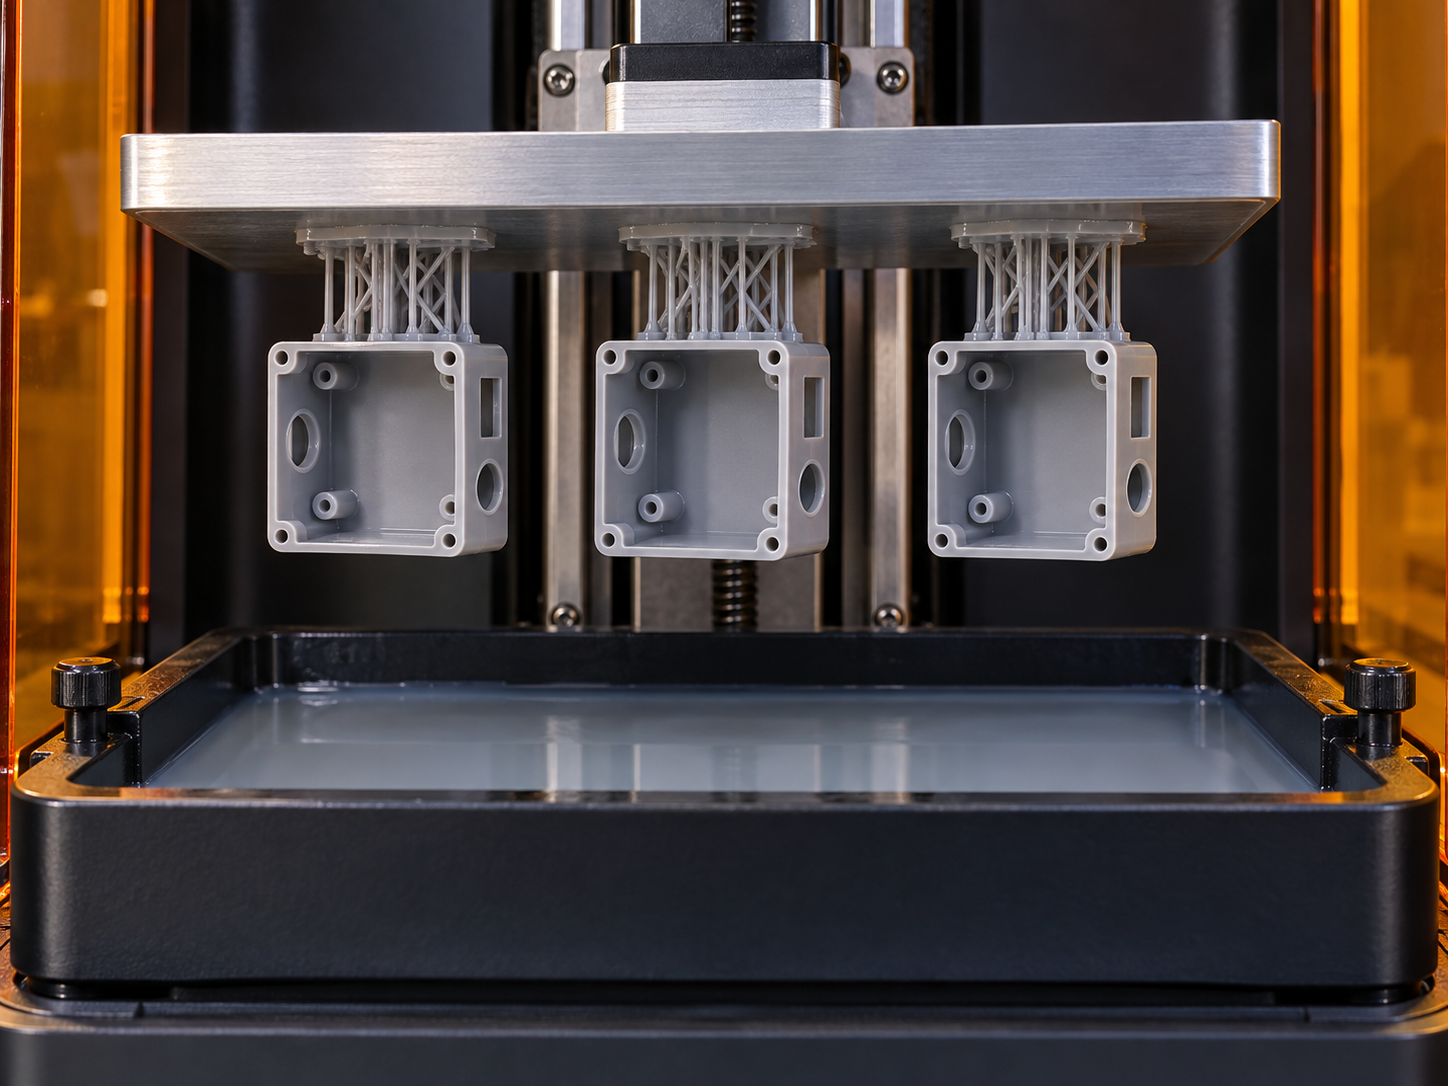
发表评论