Lead time
From 48 hours express; 72 hours / 5 days standard tiers

3D Printing
Professional nylon 3D printing for functional prototypes, jigs, and production-like SLS parts — no support trees on most geometry.
AIHFABS SLS 3D printing services fuse engineering-grade SLS plastics into durable, self-supporting parts. A laser sinters nylon powder layer by layer; unsintered powder holds the geometry, so ducts, hinges, and nested batches print without support scars. Choose sintered nylon when you need tough SLS parts for fit, function, and short-run production — not a show-resin cosmetic.
Selective Laser Sintering (SLS) is a powder-bed process: a laser traces each slice and fuses thermoplastic particles into sintered nylon. Loose powder stays around the part and acts as a nest, so most geometries do not need printed supports. That is why ducts, living features, and packed batches are everyday SLS work.
AIHFABS runs nylon SLS printing mainly in PA11, PA12, and glass filled nylon SLS, plus PP and TPU where the job needs them. After cool-down we break the cake, depowder, and dye or vapor-smooth when you ask for a less grainy skin.
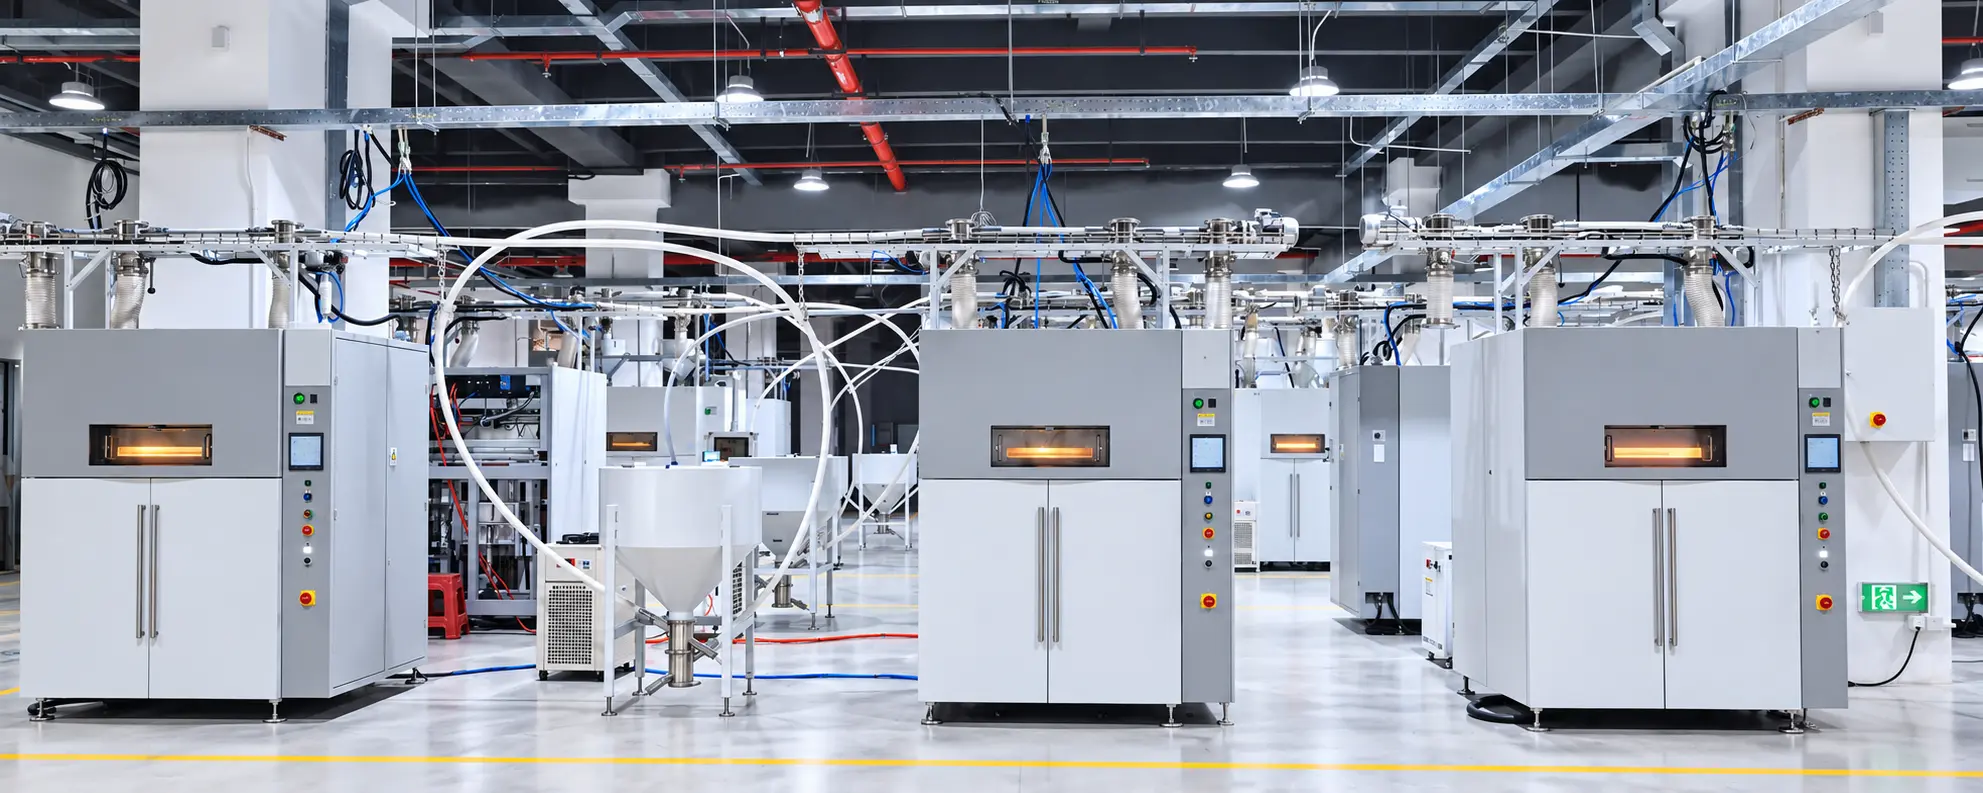
A dedicated nylon 3D printing service for functional SLS plastics — not filament mock-ups.
If you need a nylon 3D printing service that holds clips, ducts, and housings through assembly, nylon SLS is the usual first quote. Nylon SLS printing fuses engineering-grade SLS plastics into isotropic-enough parts for shop trials and short production — without support scars on internal channels.
Unfilled SLS nylon (PA12 / PA11) is the workhorse: tough, dyeable, and chemically stable. Specify glass filled nylon SLS when the cover must stay stiff near heat, or carbon-filled nylon when you want stiffness without the glass-bead mass. Grade cards are in the materials table below and on the 3D printing materials hub.
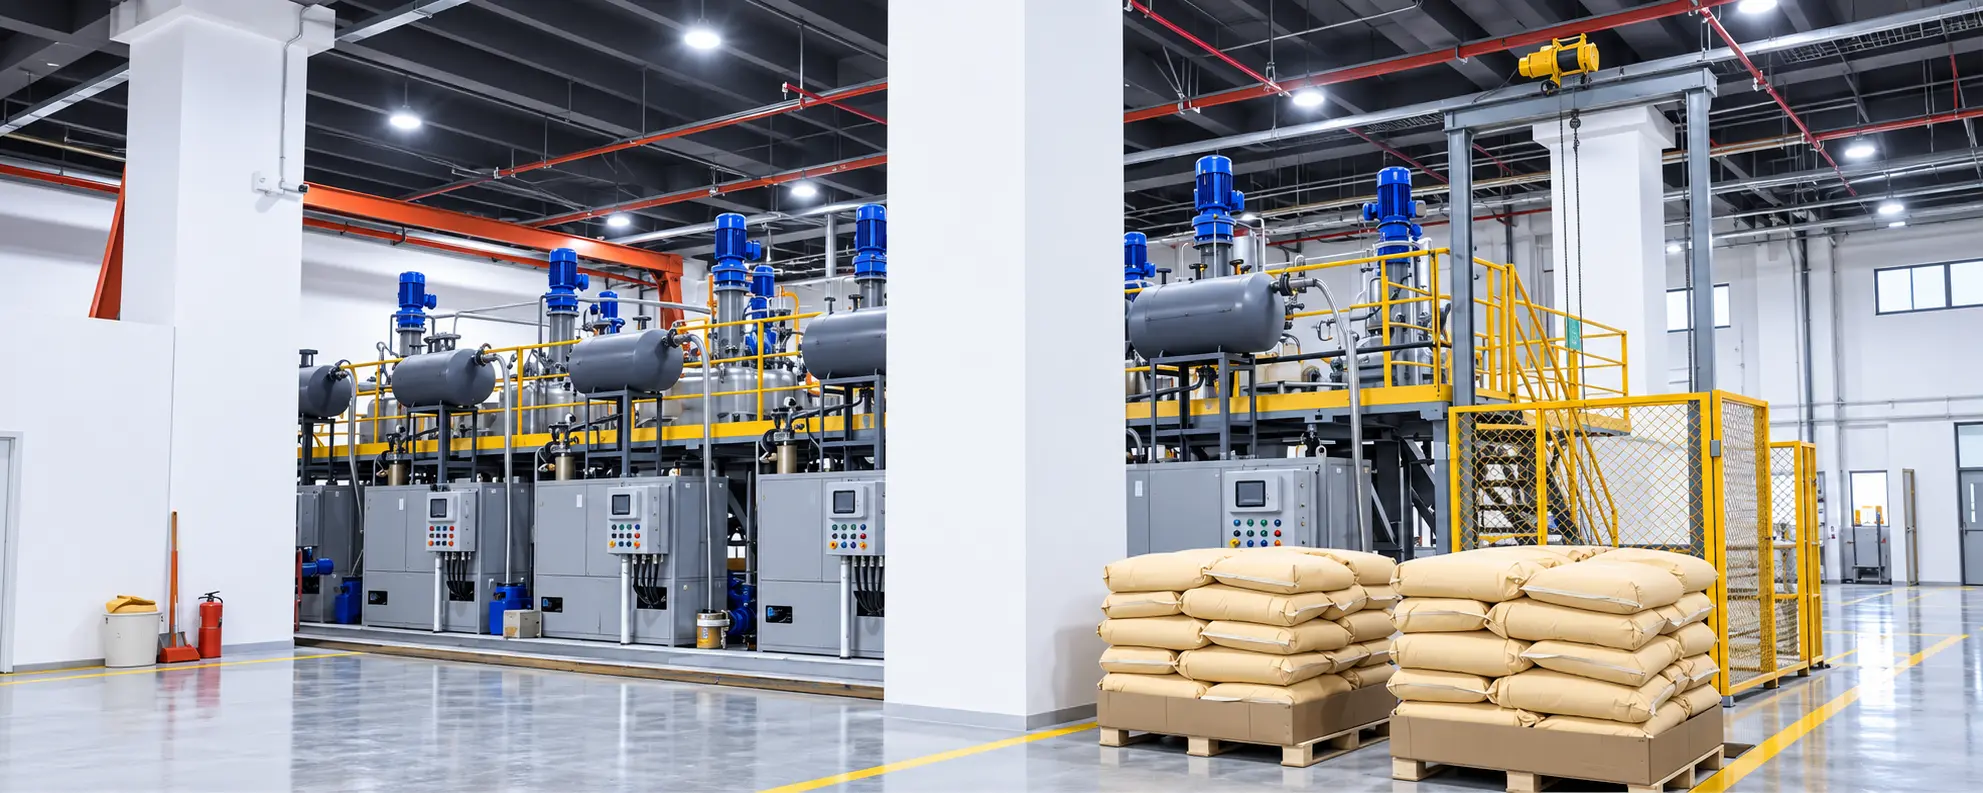
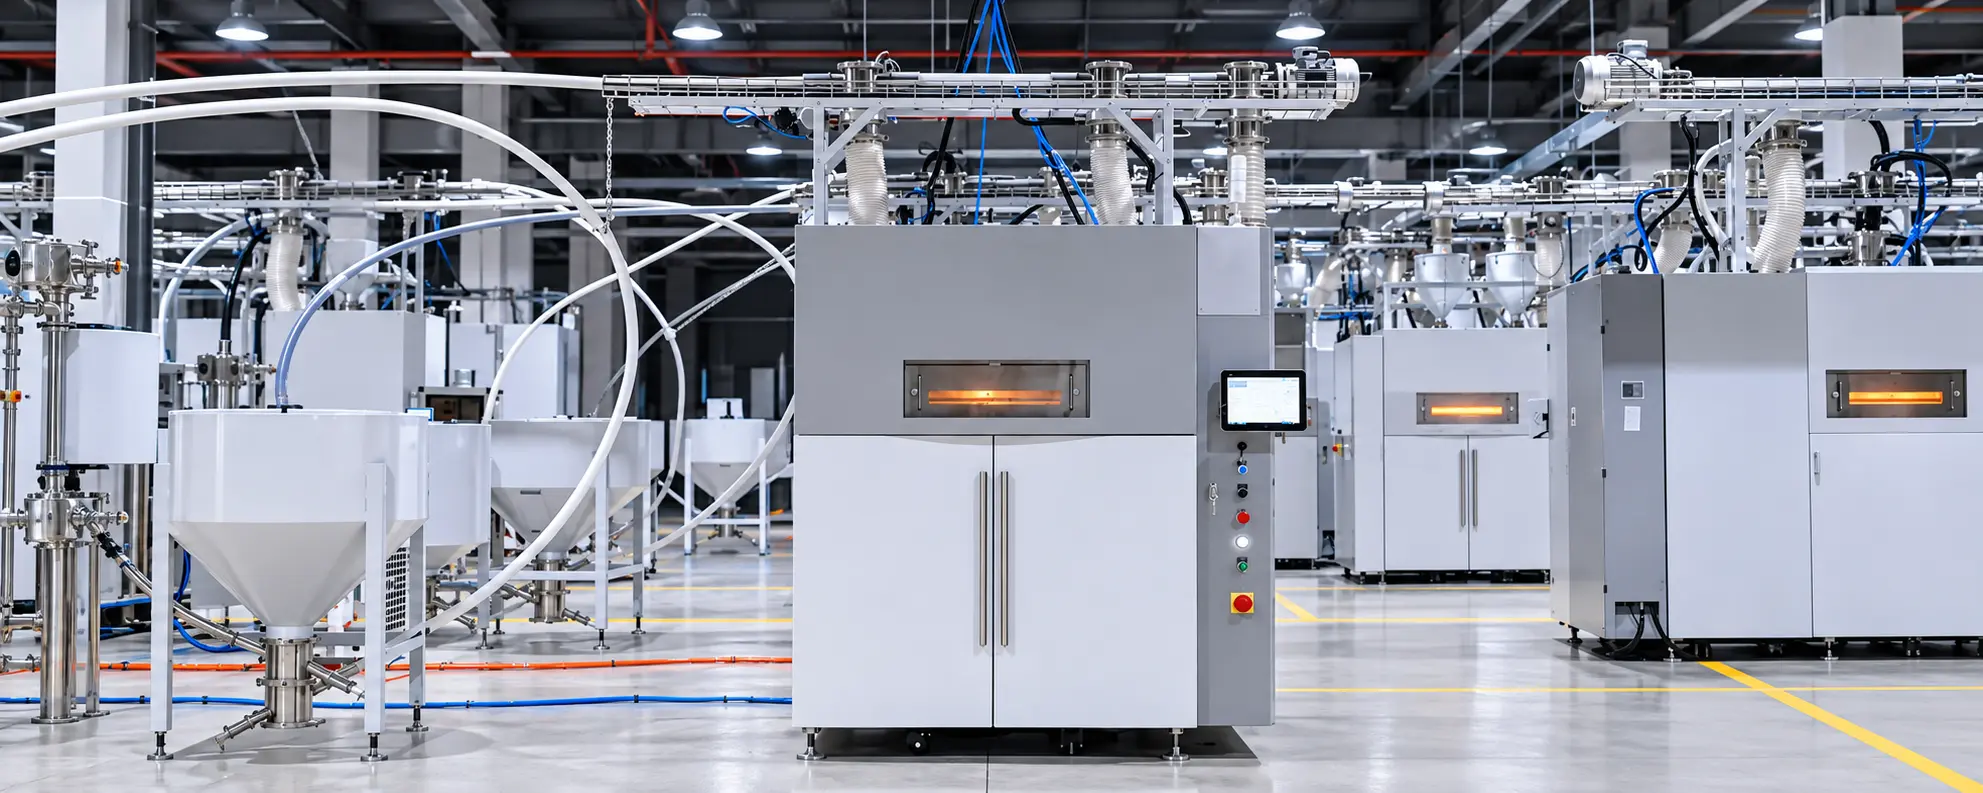
Custom SLS parts manufacturing for functional SLS printed parts — from first articles to nested production cakes.
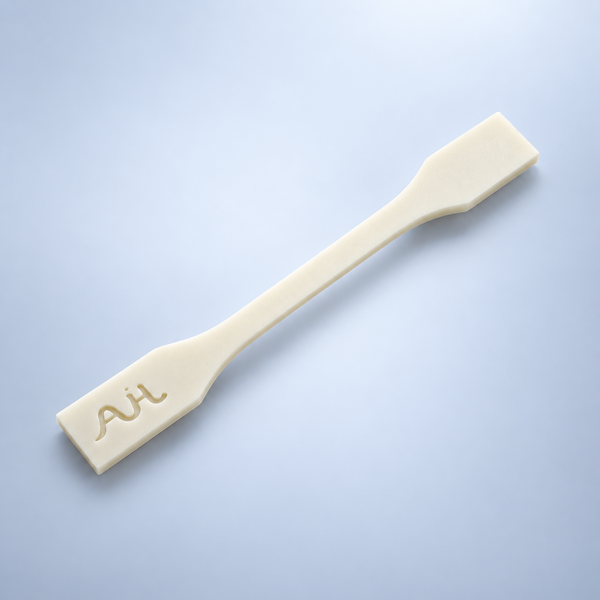
Powder-bed size and as-sintered tolerance below are planning values, not a substitute for the live quote.
From 48 hours express; 72 hours / 5 days standard tiers
±0.3 mm or ±0.3%
645 × 325 × 520 mm
Matte, slightly grainy; vapor smoothing or tumbling optional
Not required — powder bed supports the part
Engineering-grade SLS plastics first: SLS nylon (PA12 / PA11), glass filled nylon SLS, carbon-filled nylon, PP, and TPU. Catalog cards below open the grade page; filled-nylon trade-offs are in the comparison table.
Unfilled sintered nylon for snaps, ducts, and housings. PA12 is the default; PA11 when impact and elongation matter more than stiffness.
Glass beads raise modulus and heat deflection so covers and jigs hold shape. Avoid living hinges and high-elongation snaps on this grade.
Carbon fiber or mineral fill for light, stiff brackets. Different surface and anisotropy than glass-bead PA12 — pick from the datasheet on the quote, not from a slogan.
| Grade | Why choose it | Watch-outs |
|---|---|---|
| SLS nylon PA12 / PA11 | Balanced toughness, dyeable, everyday nylon SLS printing | As-sintered grain; not as stiff as filled grades |
| Glass filled nylon SLS | Stiffness, dimensional stability, higher HDT for fixtures and covers | Lower elongation; abrasive on mating plastics |
| Carbon-filled nylon | High stiffness-to-weight for brackets and light structures | Grade-specific anisotropy; confirm the datasheet on the quote |
Unpolished SLS parts leave the cake matte and slightly grainy. Dye, tumble, and vapor smooth are the usual next steps — see 3D Plus finishing for dyeing, smoothing, and coating options.
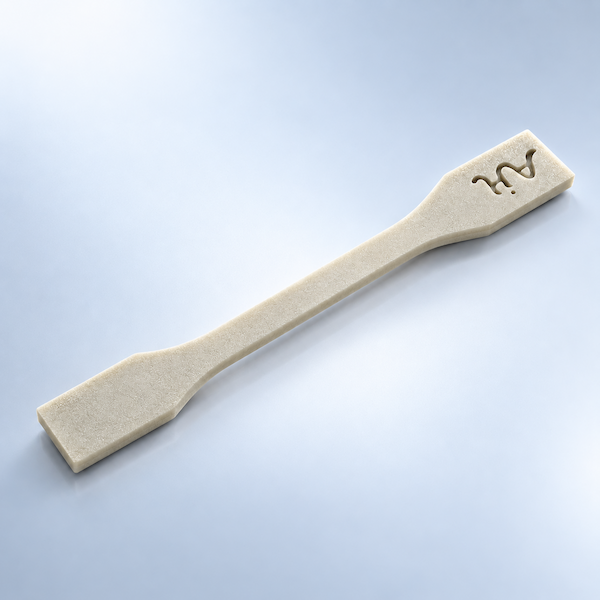
Natural white or stone-gray powder texture. Functional unpolished SLS parts — no dye, no extra cycle.
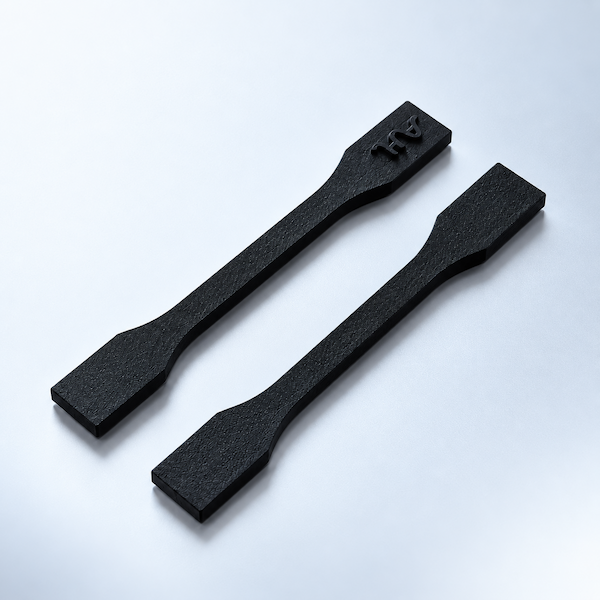
Immersion dye, most often black, that soaks a shallow layer and covers the open grain.
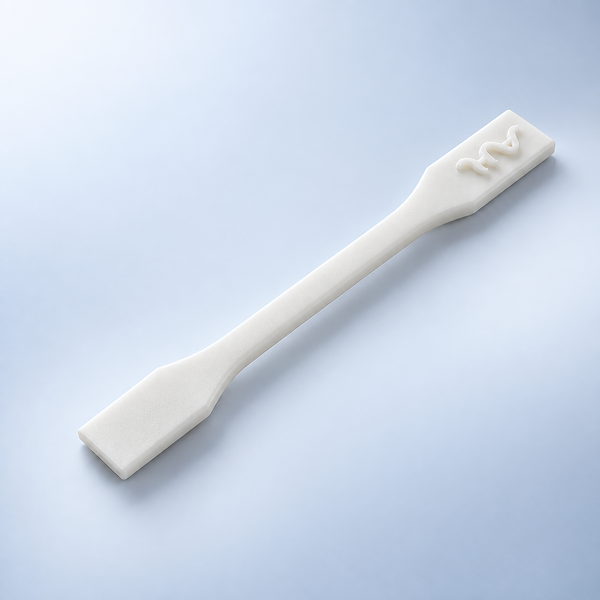
Chemical smooth or media tumble to close pores and take the chalky feel down on SLS printed parts.
SLS and MJF both print nylon without support trees. MJF is often faster on dense production nests; SLS still wins on some powder grades and envelopes.
| Process | Lead time | Tolerance | Pricing |
|---|---|---|---|
| Selective Laser Melting (SLM)Metal | From 5 business days (express options where available) | ±0.3 mm or ±0.3% (whichever is greater), tighter after machining | Instant quote · typical metal part from $90 |
| Stereolithography (SLA)Resin | Quoted with your CAD upload | Instant quote · typical resin part from $18 | |
| Digital Light Processing (DLP)Resin | From 48 hours | ±0.2 mm on supported geometry | Instant quote · typical resin batch from $20 |
| Liquid Crystal Display (LCD)Resin | From 48 hours | ±0.2 mm on supported geometry | Instant quote · typical resin part from $16 |
| Selective Laser Sintering (SLS)Plastic powder | From 48 hours express; 72 hours / 5 days standard tiers | ±0.3 mm or ±0.3% | Instant quote · typical nylon part from $28 |
| Multi Jet Fusion (MJF)Plastic powder | From 48 hours express; standard 72 hours / 5 days | ±0.3 mm or ±0.3% | Instant quote · typical PA12 part from $25 |
| Fused Deposition Modeling (FDM)Thermoplastic filament | From 24–48 hours depending on size | ±0.5 mm or ±0.5% on FDM-appropriate geometry | Instant quote · typical prototype from $12 |
Powder is preheated and spread in a thin layer across the build chamber.
The laser sinters the cross-section; unsintered powder remains in place.
The platform indexes downward; fresh powder is recoated for the next layer.
The cake is cooled, depowdered, and finished with dye, vapor smooth, or machining.
Packing density, escape holes, and wall thickness are checked before the cake is committed. Enclosed volumes without a powder exit are flagged in DFM.
After cool-down, parts are depowdered and blasted. Dye, vapor smooth, or tapping is added only when the order lists it. Unpolished SLS parts ship as-sintered unless you ask for a finish.
Let powder out, then keep walls in a band the cake can cool without banana-ing.
| Feature | Recommended practice |
|---|---|
| Escape holes | Open every enclosed volume so unsintered powder can leave. |
| Walls | About 1.0 mm unsupported and 0.8 mm supported is a safe first pass. |
| Holes & details | Keep holes and embossed details around 0.8–1.0 mm or larger. |
| Living hinges | Use a TPU grade and a tuned thickness — PA12 is the wrong hinge material. |
| Large flats | Rib large panels so they stay flatter through cool-down. |
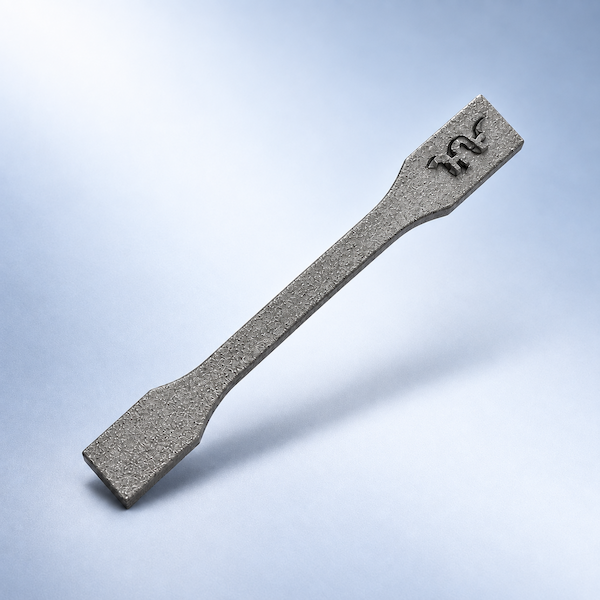
Selective Laser Melting (SLM) is a powder-bed metal additive process. A high-power laser scans each cross-section of your CAD model, melting metal powder that solidifies into a dense part.
Full process details
Stereolithography (SLA) cures liquid photopolymer with a precision UV laser, building parts layer by layer.
Full process details
Digital Light Processing (DLP) solidifies an entire layer of photopolymer at once using a projected image.
Full process details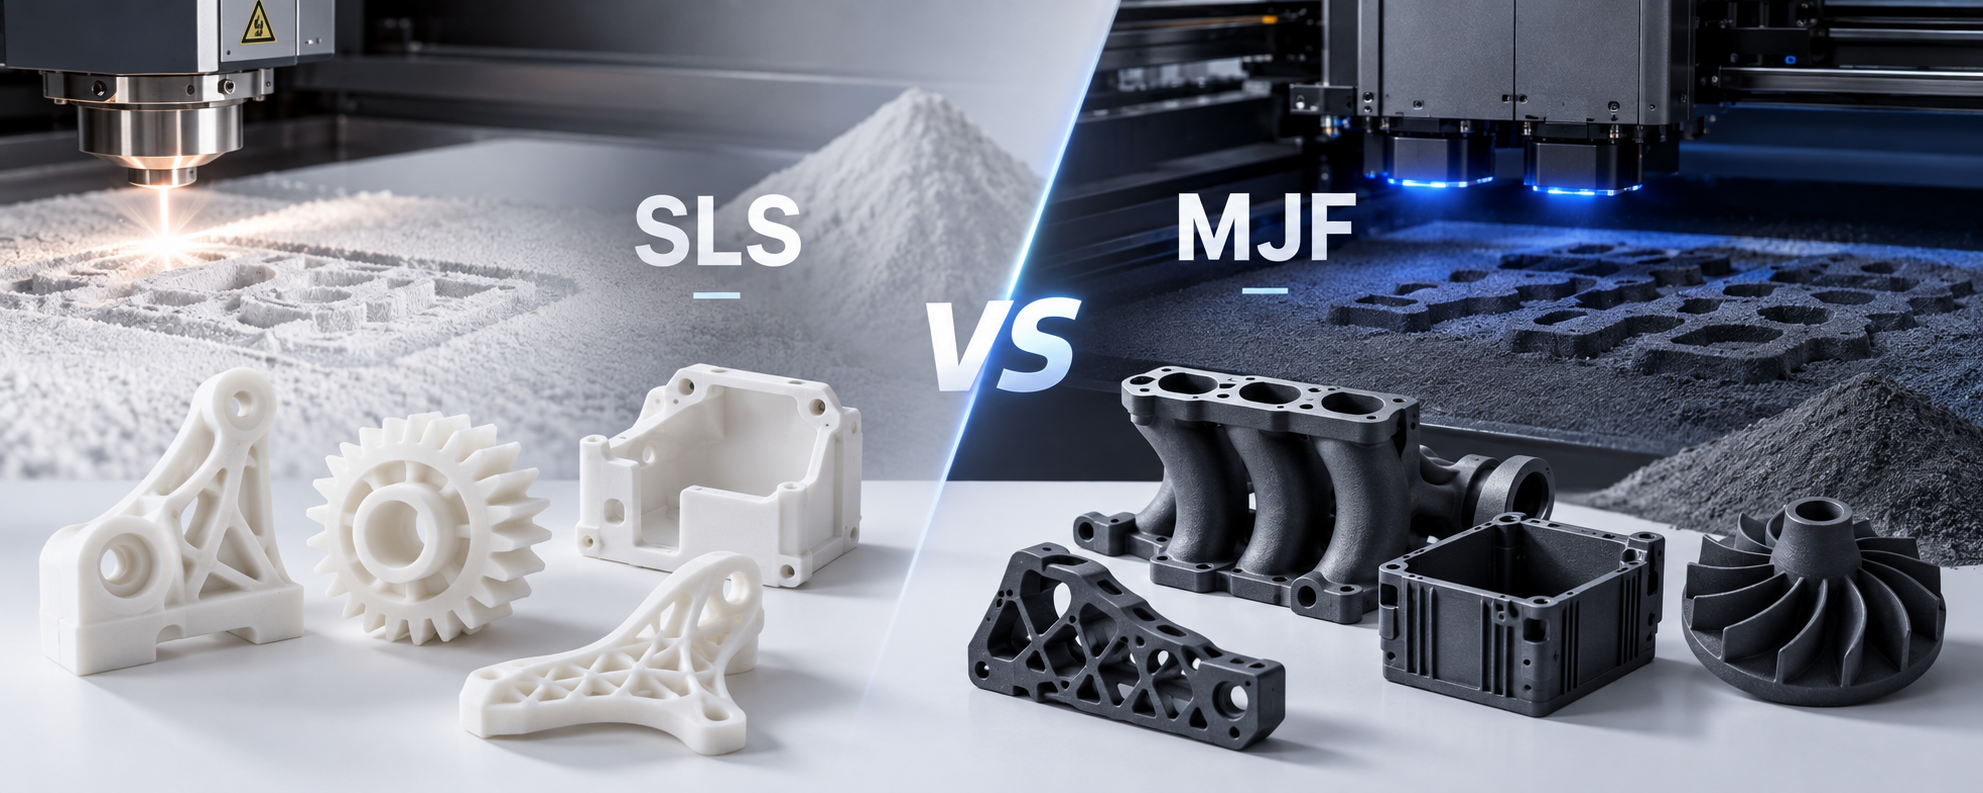
Surface, accuracy, and when powder-bed nylon belongs on the quote as SLS or MJF.
Full process details
File prep, units, and what to upload so an SLS or nylon quote comes back clean.
Full process details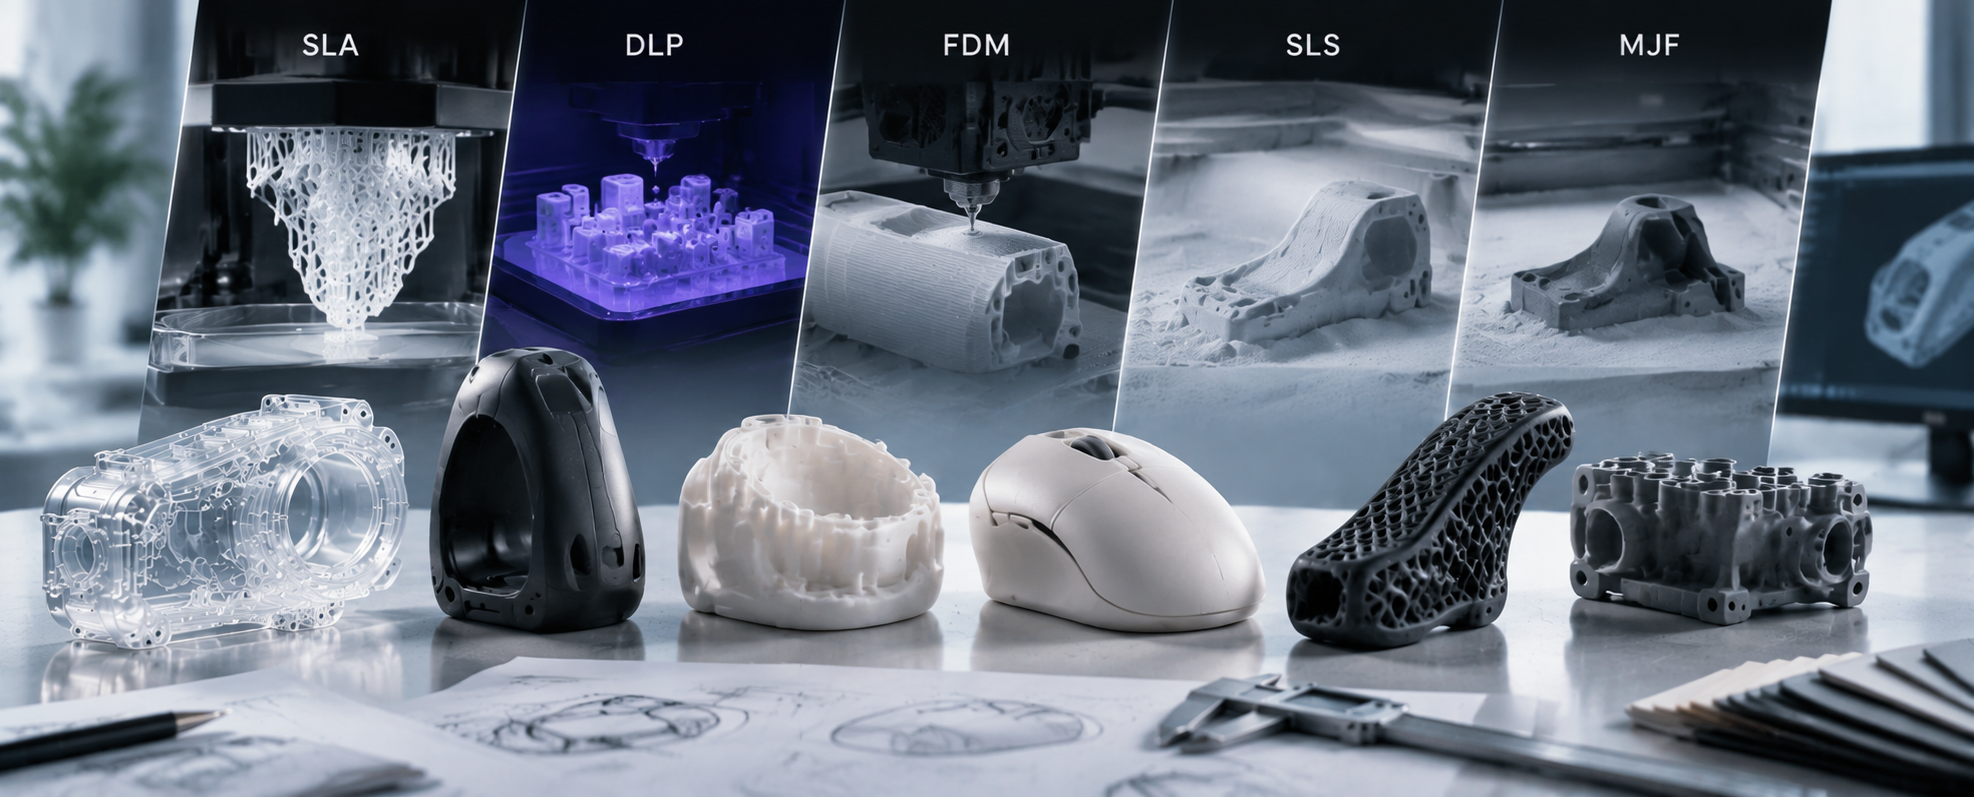
When sintered nylon is the right first quote — and when resin or CNC is a better start.
Full process detailsAlmost never. The unsintered powder holds the sintered nylon part. You still need escape holes on closed volumes.
Both make durable PA12. MJF is often quicker on dense production nests; SLS is strong when the powder grade or the envelope fits that cell better. Upload once and we will pick a route.
SLS printed parts are tough and slightly grainy as-sintered. Plan ±0.3 mm or ±0.3% on typical geometry. Dye and vapor smooth improve cosmetics without changing the bulk nylon much; polishing can round edges and should be called out when a sharp edge is functional.
Glass filled nylon SLS is for stiff housings, jigs, and covers that must not sag. It is the wrong grade for living hinges and high-elongation snaps — use unfilled SLS nylon or TPU there.
Yes. Depowder and blast are standard. Dye, tumble, vapor smooth, tap, and paint are quoted when you list them. Color and coating options are on 3D Plus finishing.
±0.3 mm or ±0.3%, whichever is greater, on typical SLS geometry. Tighter fits can be reviewed with a drawing and optional machining.
Express from 48 hours; standard tiers around 72 hours or 5 business days depending on cake schedule.
AIHFABS quotes custom 3D printing and CNC machining from a CAD upload. Compare SLA, SLS, MJF, SLM, FDM, DLP, milling, and turning, then add finishing such as vapor smoothing, dyeing, anodizing, polishing, or powder coating in the same order.
Instant quoting is built for prototypes, jigs, housings, and small-batch production. You see material, process, quantity, and lead time together, which keeps engineering changes from turning into a new round of supplier emails.
You can review material, process, quantity, and lead time together, so engineering changes do not turn into another round of supplier emails.
Upload STL, STEP, and other common CAD formats for an online quote.
Compare 3D printing technologies and CNC options on the same part.
Select polymers or metals, then add 3D Plus hardware finishing when needed.
Review price and lead time before checkout, or request a manual quote for special specs.
If this page describes a process, industry, or sample part you want to reproduce, start from the upload flow and match technology plus finishing to your drawing.
We use cookies to personalize your experience. By using this site, you agree to our Privacy Policy
Accept