CNC加工
CNC Machining Services
CNC machining removes material from solid stock with computer-controlled mills, lathes, and multi-axis centers.
创建报价
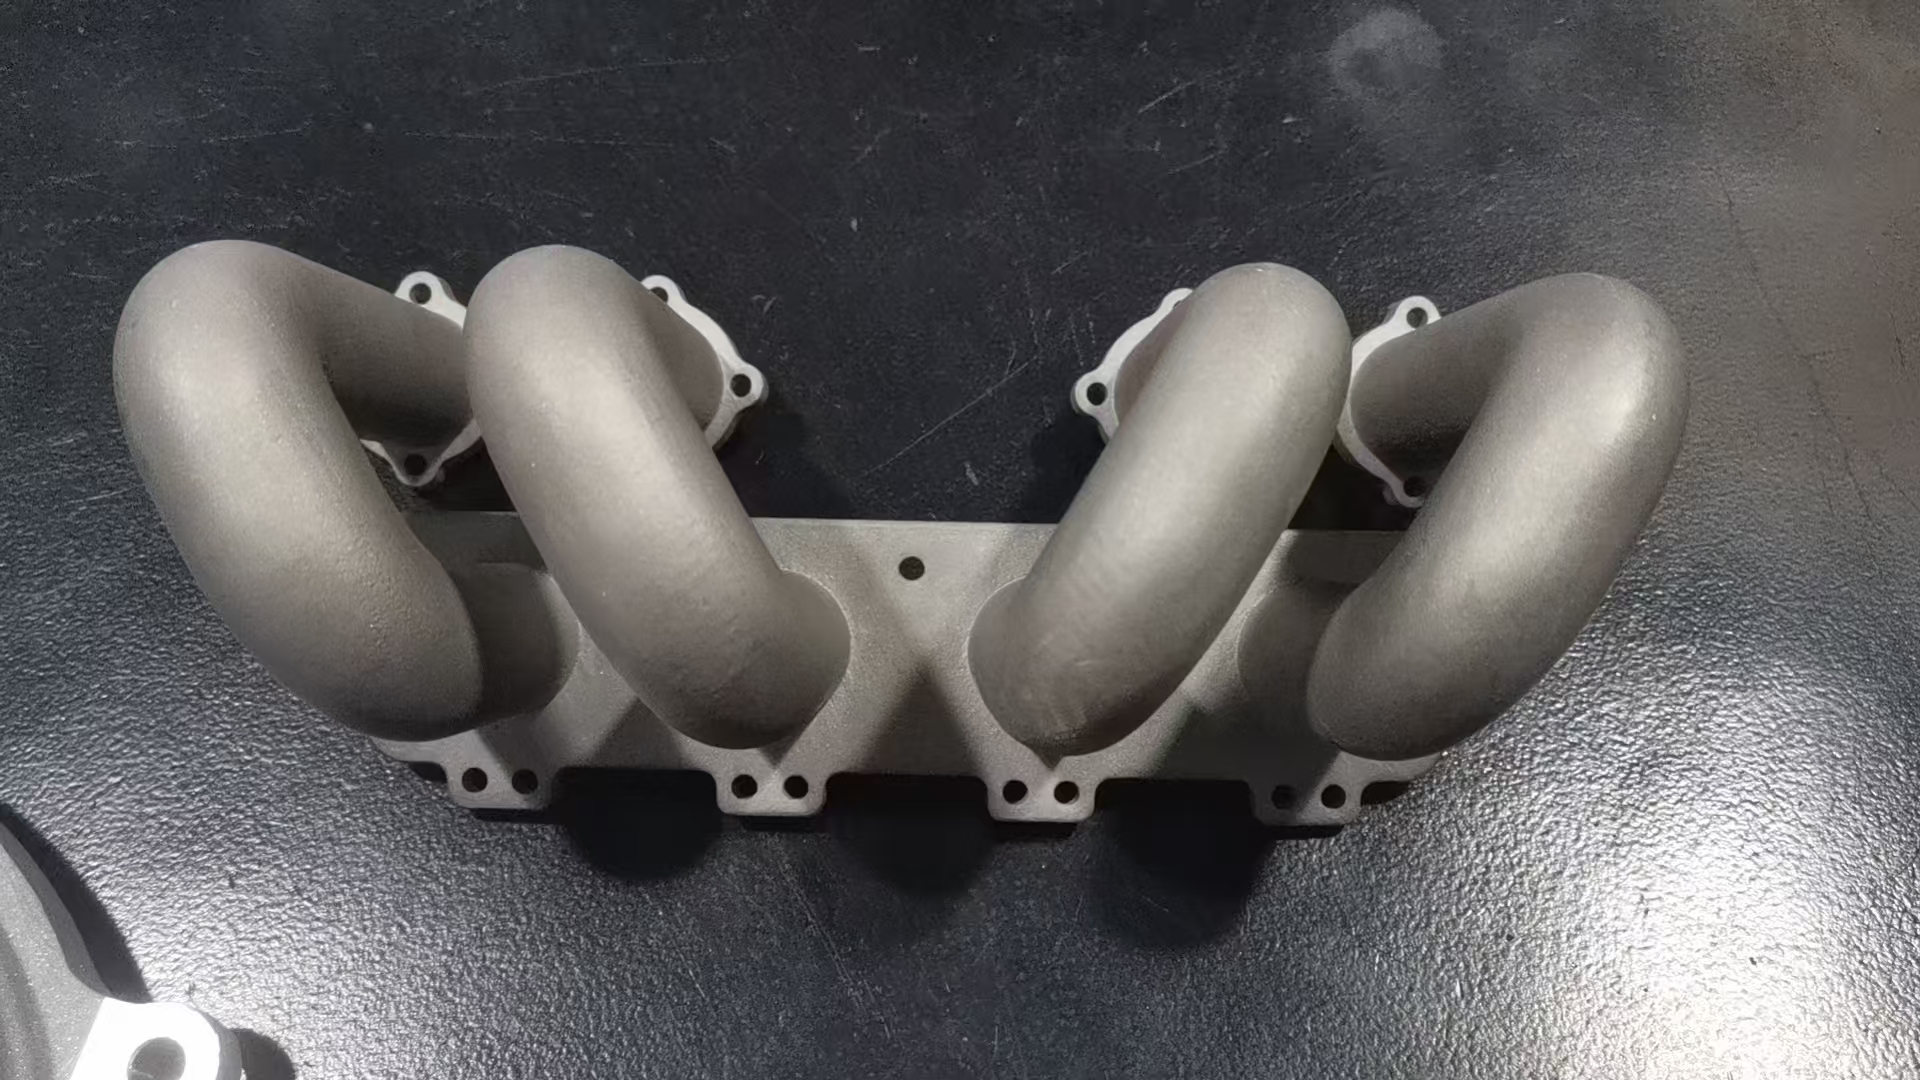
Introduction: Hardware teams can use metal 3D printing to screen functional parts where geometry, weight, and integration drive manufacturing value.
For many hardware projects, the real question is not whether a metal part can be printed. It is whether a metal 3d printing service creates enough engineering advantage to justify SLM evaluation over machining, casting, sheet fabrication, or assembly from multiple components. This article maps common industrial scenarios where SLM may be worth early consideration, where engineering review is essential, and where application language should stay conservative, especially in aerospace and medical contexts.
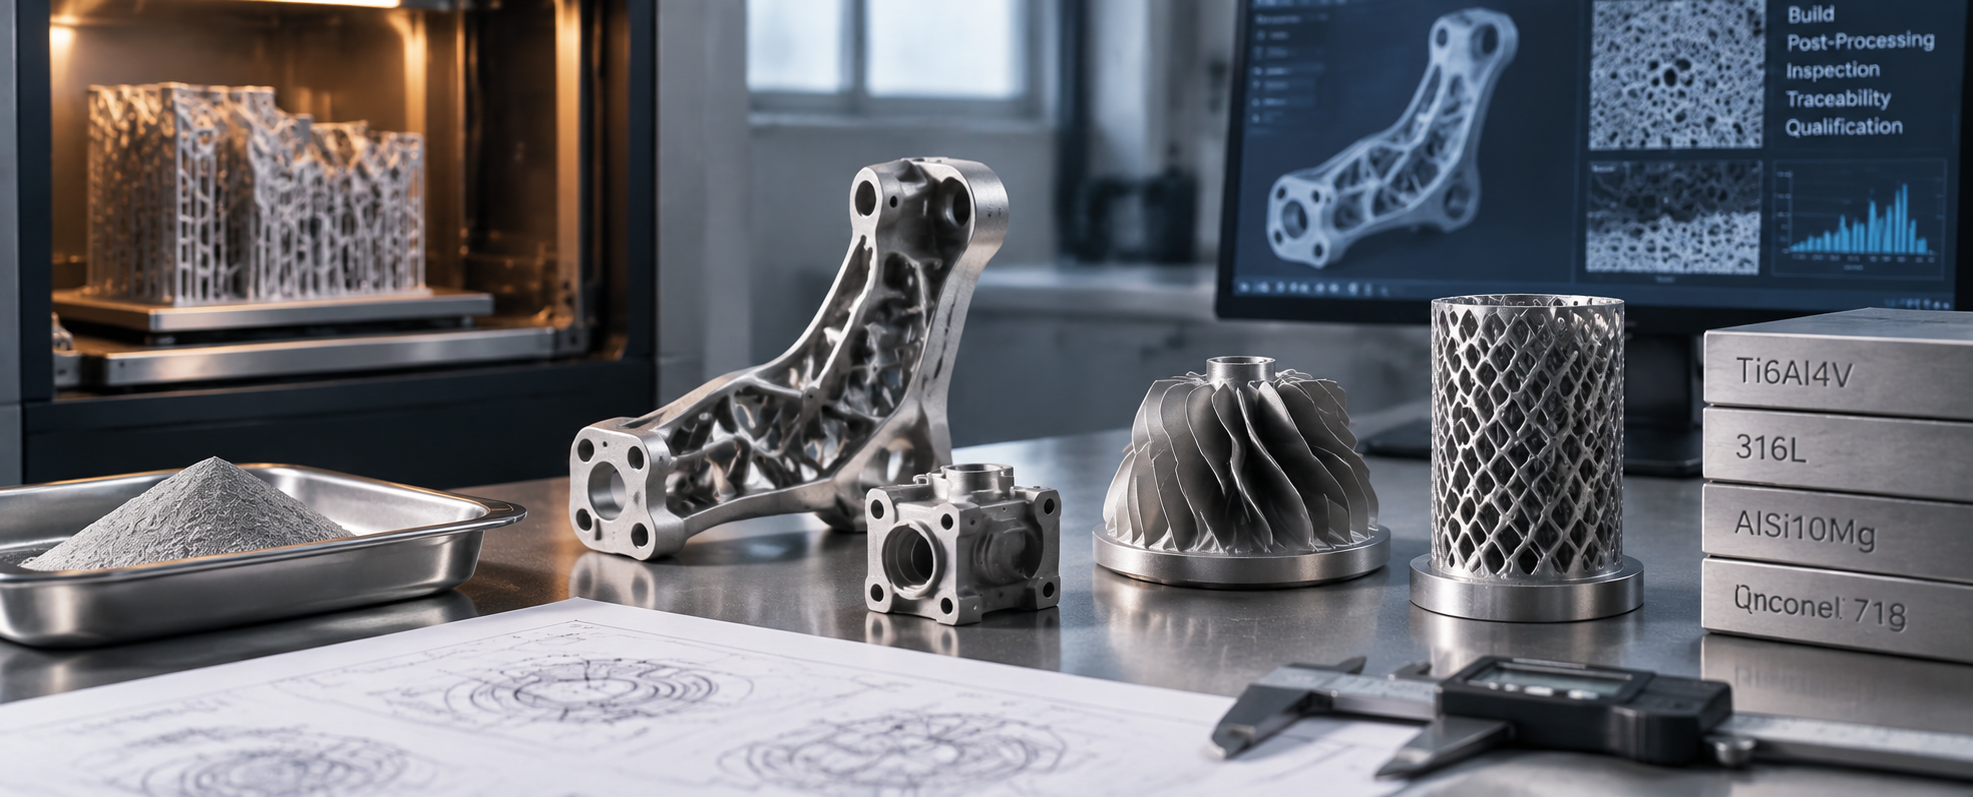
SLM is most compelling when a part’s value depends on geometry that is difficult, costly, or inefficient to create through subtractive manufacturing. In a hardware team’s early screening, lightweight ribs, lattice-like regions, internal channels, consolidated assemblies, and compact cooling paths are stronger signals than a simple desire to “print metal.” Powder bed fusion processes build parts layer by layer from metal powder, which can open design routes that are less practical when every surface must be reached by a cutting tool. That does not make every complex shape manufacturable, but it does shift the decision from a basic material question toward a geometry-and-function question. A useful first filter is to ask what the geometry is doing for the product. If a bracket only needs a flat plate with holes, machining or sheet fabrication may remain more economical. If the same bracket must reduce mass, route loads through organic forms, combine several bolted pieces, and fit into a restricted envelope, SLM 3D printing for lightweight structures becomes more relevant. Similarly, if a part uses internal channels to manage air, fluid, or heat, custom metal 3d printing may reduce assembly seams or secondary joining steps. The practical boundary is that channels still need depowdering access, overhangs may require support, and critical interfaces may need machining or other finishing after printing. This is why hardware teams should classify parts by functional pressure rather than by industry label alone. A robotics end-effector, heat sink, tooling insert, or aerospace-style bracket may all be possible candidates, but the reason differs in each case. One project may prioritize low mass at the end of an arm; another may need internal cooling near a heat source; another may need a short-run fixture that changes with product revisions. SLM deserves attention when the part’s geometry reduces system weight, integrates functions, shortens assembly, or enables performance features that would otherwise require several manufacturing steps.
A scenario map helps teams avoid two common mistakes: sending every metal component into SLM evaluation, or rejecting SLM because one simple machined part did not justify it. The better approach is to group the part by the engineering problem it solves, then decide whether a 3d printing metal service should be an early candidate, a secondary option, or a poor fit without redesign. These groupings are not automatic approvals; they are practical starting points for model review, material discussion, build orientation planning, support removal, post-processing, and cost comparison.
• Lightweight structural hardware: Brackets, mounts, ducting supports, and weight-optimized hardware can be good SLM candidates when reduced mass improves system performance or handling. The design still needs load-path review, material selection, and confirmation that critical mounting faces can be finished to the required fit.
• Internal channels and cooling paths: SLM 3D printing for internal channels is relevant when cooling, fluid routing, or compact airflow cannot be achieved easily with drilling, brazing, or multi-piece assemblies. Teams should confirm channel diameter, powder removal, inspection expectations, and whether the geometry can be cleaned after the build.
• Tooling fixtures and jigs: Custom fixtures, jigs, and automotive tooling inserts may benefit when low-volume production, fast iteration, or conformal features matter more than lowest unit cost. However, wear surfaces, threaded features, and precision locating points may still require machining or inserts after printing.
• Robotics end-effectors and heat sinks: End-effectors can benefit from reduced mass, integrated mounting, and complex gripping geometry, while heat sinks may use expanded surface area or internal paths. These applications need engineering confirmation around stiffness, thermal targets, surface condition, and post-processing access.
This mapping keeps the decision commercial as well as technical. A hardware team is not only asking whether a part can be made; it is asking whether the manufacturing route supports schedule, iteration, assembly reduction, and functional validation. For prototypes and low-volume functional parts, SLM may help teams test a metal design before investing in tooling or complex assemblies. For repeated production, teams should expect additional qualification work before treating repeatability as a production assumption. The part may move from “strong candidate” to “needs engineering confirmation” if it has very tight interfaces, inaccessible trapped powder regions, unsupported overhangs, or industry-specific documentation requirements. AIHFABS can fit into this evaluation as a project intake route rather than as a shortcut around engineering judgment. Its SLM service information identifies application directions such as aerospace brackets, automotive tooling inserts, medical instruments, robotics end-effectors, heat sinks, and industrial automation fixtures, along with geometry signals including lightweight structures, internal channels, consolidated assemblies, lattice structures, and internal cooling paths. Hardware teams using the platform should describe the application environment, key load or thermal function, critical interfaces, preferred material direction, quantity, and any finishing needs when they submit a CAD model for review.
Aerospace, automotive, and medical examples are useful because they show why SLM attracts attention: high-value parts often need weight reduction, functional integration, or geometry that traditional manufacturing struggles to produce efficiently. However, these sectors also create a language trap. A part that resembles an aerospace bracket is not automatically certified aerospace hardware. A medical instrument or patient-specific surgical guide direction does not mean every material, workflow, or use case is suitable for regulated clinical use. For hardware teams, the safe interpretation is that these sectors provide application clues, not proof of completed certified production. In aerospace-style applications, lightweight structural hardware and ducting are logical discussion points because every gram, interface, and assembly step can matter. Yet spaceflight and aviation programs typically require strict process control, documentation, inspection, and acceptance procedures. For an early prototype, SLM may help evaluate geometry and fit. For a flight or certified application, the team must treat the additive process, material batch, post-processing, inspection, and qualification route as separate project requirements. The same boundary applies in automotive contexts: tooling inserts, jigs, and low-volume performance parts may be reasonable candidates, while certified production parts require a more formal approval path. Medical language deserves the same restraint. Medical instruments and material-dependent patient-specific surgical guides may be discussed as SLM application directions, but they should not be expanded into implant manufacturing claims or general medical certification promises. Regulatory guidance for additively manufactured medical devices emphasizes design, manufacturing, material, and validation considerations, so teams should separate a functional manufacturing discussion from a regulated-use decision. If a project involves clinical use, patient specificity, sterilization, biocompatibility, traceability, or formal submissions, those requirements must be raised before treating the part as a normal industrial component. For everyday industrial automation, the decision boundary is often less regulatory but still practical. A fixture, end-effector, or heat sink may be a strong candidate when the geometry is performance-driven and the quantity is modest. It may be weaker if the part is a simple block, needs only standard drilled holes, or depends on ultra-smooth surfaces across inaccessible internal areas. The most productive next step is to classify the part by function, mark the surfaces that need secondary finishing, and submit the model with clear notes on load, heat, assembly, and operating environment. That gives a metal 3d printing service enough context to judge feasibility without turning typical applications into unsupported guarantees.
Metal 3D printing is most valuable when it solves a functional geometry problem, not when it is treated as a universal substitute for machining. Lightweight structures, internal channels, consolidated assemblies, tooling fixtures, robotics end-effectors, heat sinks, and low-volume functional parts can all be strong candidates when their geometry supports a real engineering goal. Hardware teams should group each part by the problem it solves, then confirm material, support removal, finishing, inspection, and application boundaries before moving forward. AIHFABS can be used as a practical SLM evaluation route by uploading the model and explaining the part’s operating environment, critical function, and key manufacturing expectations.
Q:Which industrial parts are good candidates for SLM metal 3D printing?
A:Good candidates include lightweight brackets, structural hardware, tooling inserts, jigs, robotics end-effectors, heat sinks, industrial automation fixtures, and low-volume functional metal parts where geometry creates value. Parts are stronger candidates when they need weight reduction, internal features, consolidated assemblies, or complex shapes that would be difficult or costly to machine from solid stock.
Q:Can a metal 3D printing service support lightweight structures and internal channels?
A:A metal 3D printing service using SLM can support lightweight structures, lattice-like forms, consolidated assemblies, and internal channels in suitable designs. The design still needs engineering review because trapped powder, channel access, overhang support, surface condition, and post-processing can affect whether the model is practical to build and finish.
Q:How should hardware teams treat aerospace or medical application examples in SLM evaluation?
A:Aerospace and medical examples should be treated as application directions, not automatic certification claims. Teams can use them to understand why SLM is considered for lightweight hardware, instruments, or material-dependent surgical guides, but certified aerospace, regulated medical, or patient-specific use requires separate verification, documentation, material review, and compliance assessment.
ADDITIVE MANUFACTURING REQUIREMENTS FOR SPACEFLIGHT SYSTEMS
3D Printing of Medical Devices
和这篇文章相关的工艺。打开规格,或把文件放到报价上。
CNC machining removes material from solid stock with computer-controlled mills, lathes, and multi-axis centers.
创建报价
CNC Milling Services use computer numerical control (CNC) mills to cut workpieces with rotating tools according to programmed toolpaths.
创建报价和这篇文章相邻的材料。先看卡片,再上传 CAD。
工艺、后处理和文件注意事项,来自车间,不是营销软文。
按主题查看公司、付款、物流和工艺说明。
Review AIH commitments to print quality, secure handling of your files, transparent pricing, and support for every 3D printing order.
Recommended answers about AIHFABS, technologies, materials, pricing, privacy, and file preparation.
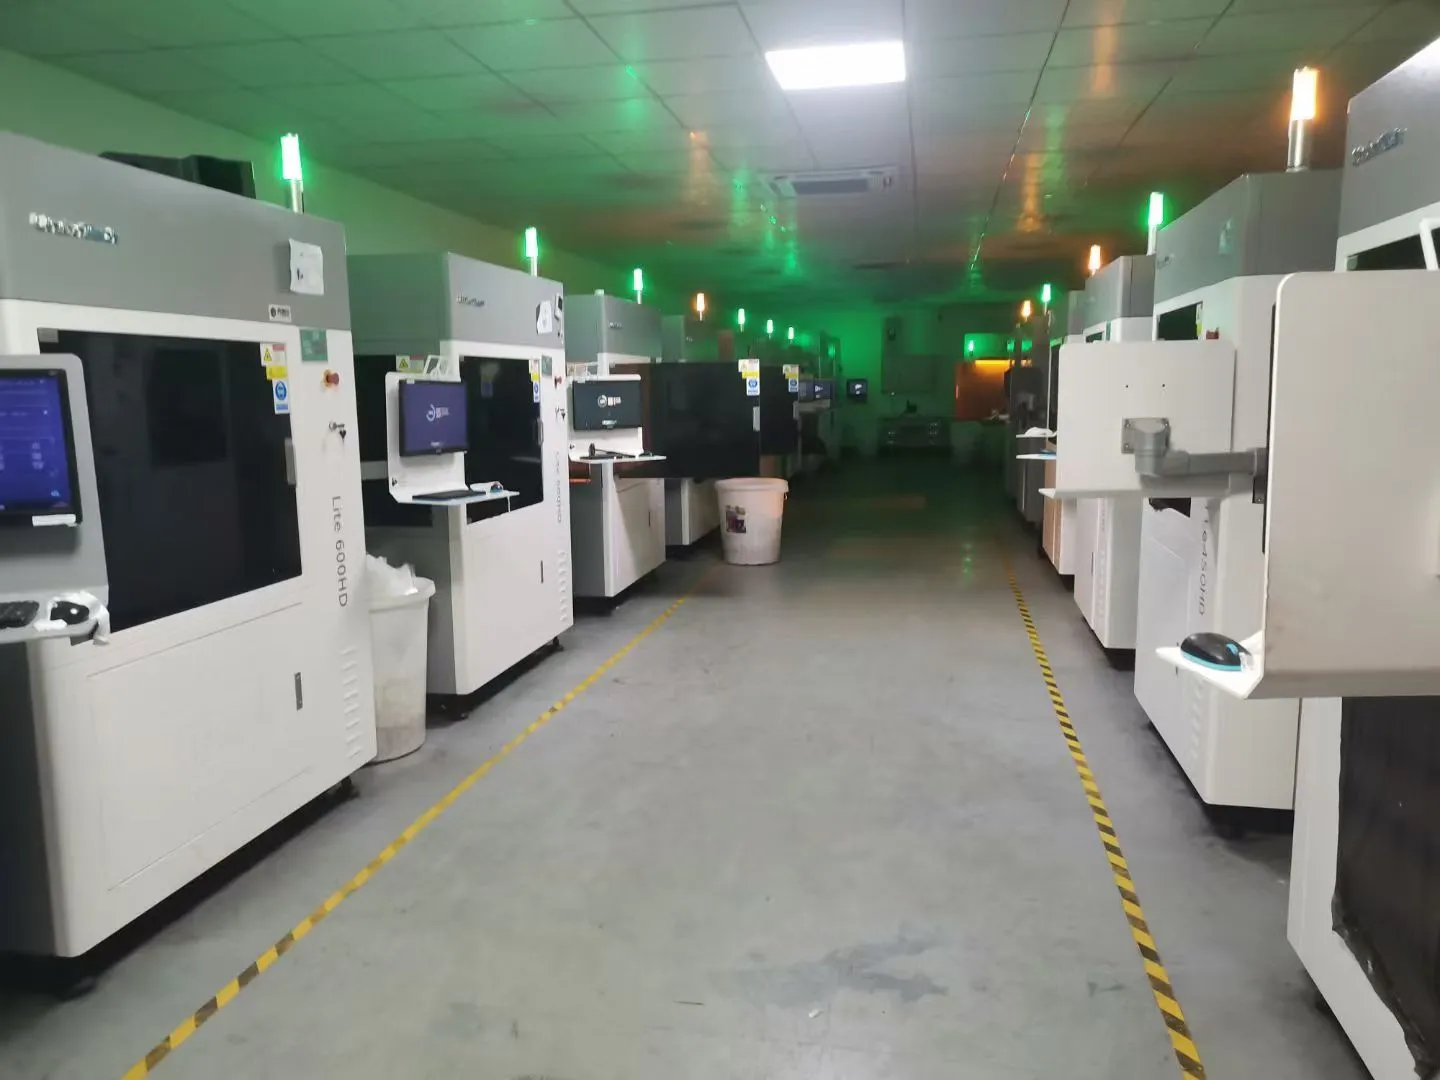
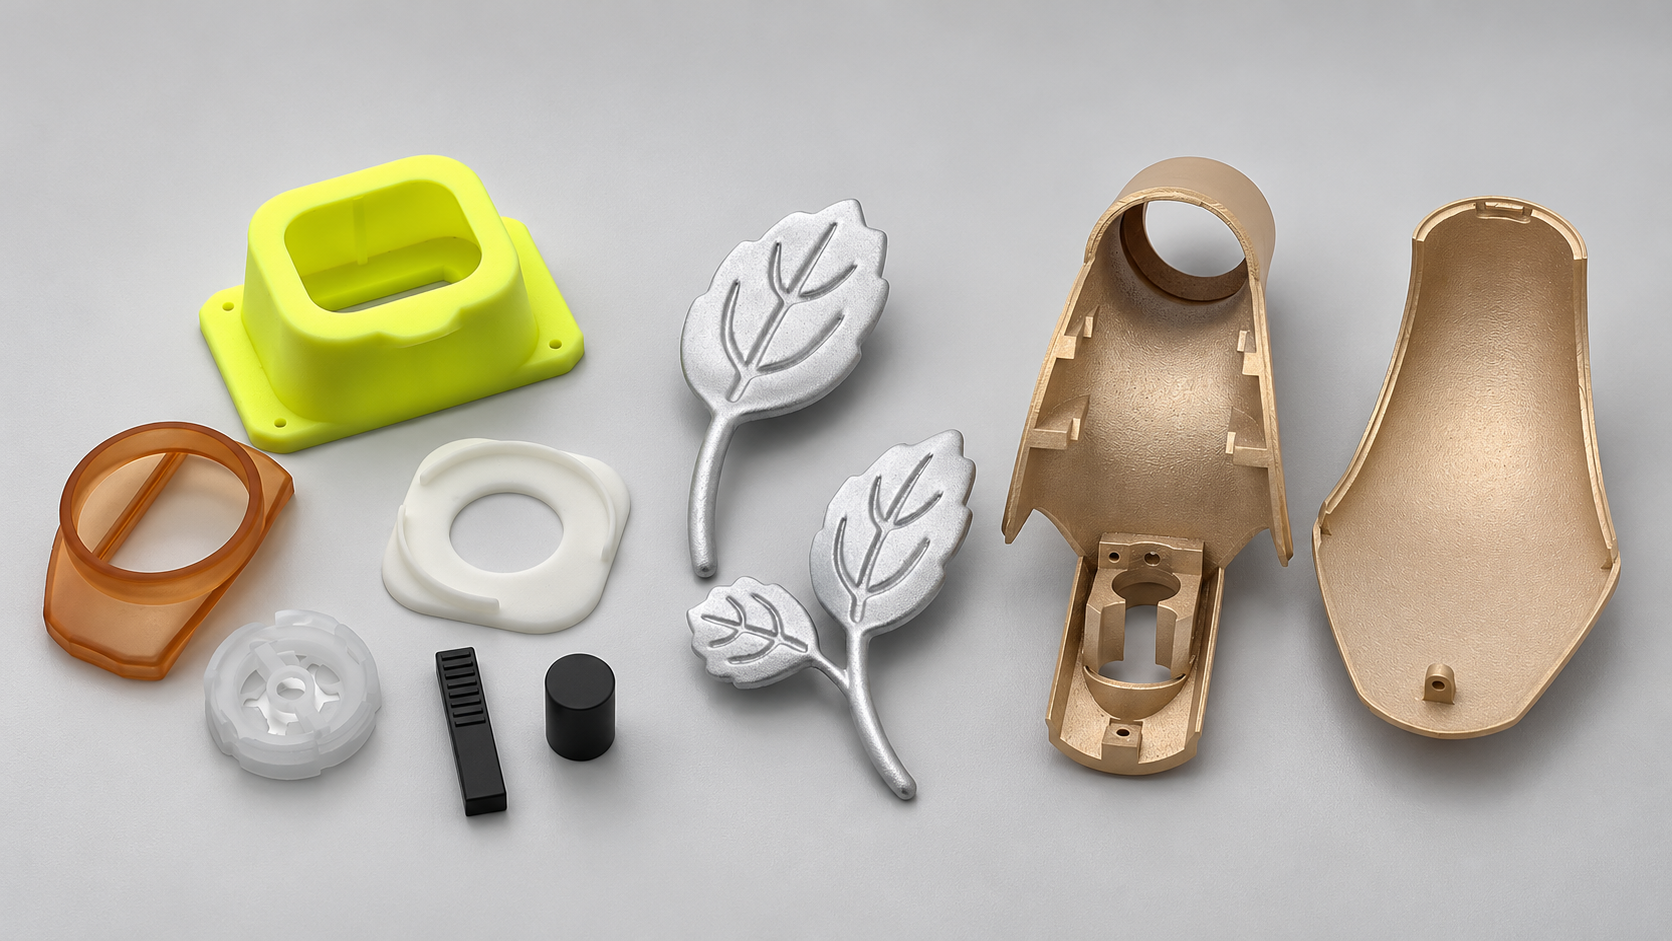
AIHFABS 根据 CAD 上传为定制 3D 打印和 CNC 加工报价。比较 SLA、SLS、MJF、SLM、FDM、DLP、铣削和车削,并可在同一订单中添加蒸汽抛光、染色、阳极氧化、抛光或粉末喷涂。
即时报价适合原型、治具、壳体和小批量。材料、工艺、数量和交期一起展示,减少工程变更后再发一轮供应商邮件。
材料、工艺、数量和交期一起展示,减少工程变更后再发一轮供应商邮件。
上传 STL、STEP 等常用 CAD 格式即可在线报价。
在同一零件上比较 3D 打印工艺和 CNC 选项。
选择聚合物或金属,需要时再添加 3D Plus 硬件后处理。
结算前查看价格和交期,特殊规格可申请人工报价。
若本页描述的是你想复现的工艺、行业或样品,请从上传流程开始,把工艺和后处理与图纸对齐。
我们使用 cookie 优化体验。继续使用即表示您同意我们的 隐私政策
接受
发表评论