3D Printing
Selective Laser Sintering (SLS)
AIHFABS SLS 3D printing services fuse engineering-grade SLS plastics into durable, self-supporting parts.
Create a quote
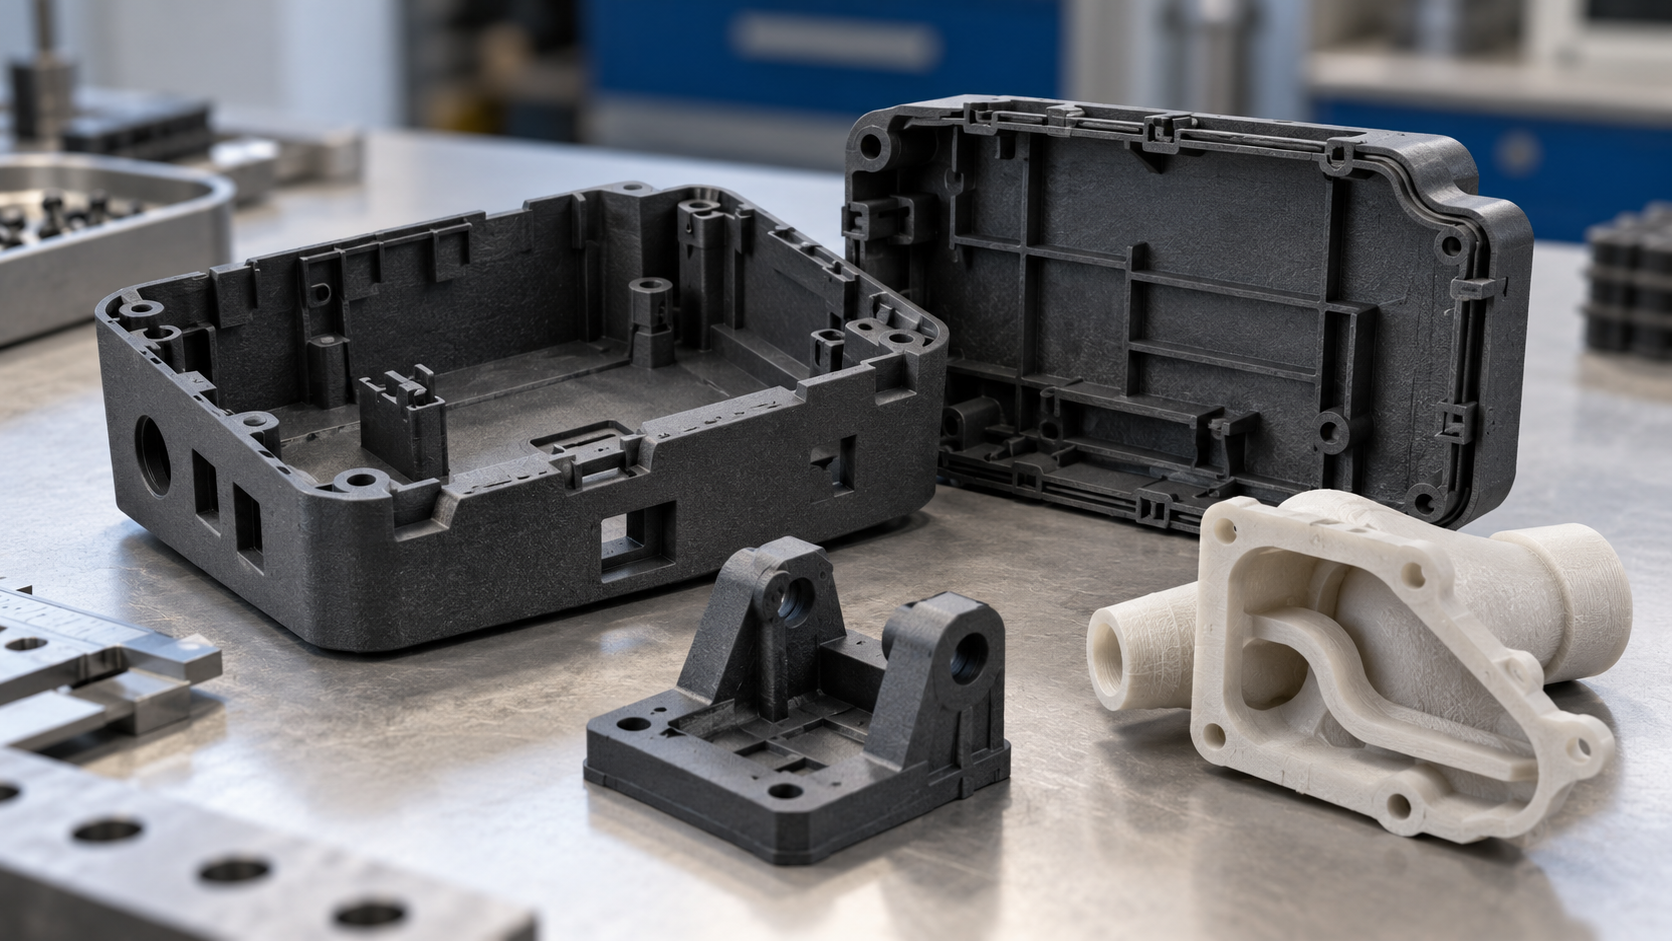
AIH frames SLS nylon printing around functional fit, material trade-offs, and the often overlooked costs of getting a part ready.
A nylon housing may look ready in CAD, yet its first assembly can reveal a tight clip, trapped powder, or a hole that needs a different finishing plan. Those are not minor print details. They decide whether a prototype helps a team learn or starts another round of rework.
AIH offers selective laser sintering for functional prototypes, jigs, and short-run parts in nylon and other polymers. This edited Q&A examines the design judgments behind that service. Anika Desai is a fictional Technical Director persona; the exchange is an editorial reconstruction grounded in AIH’s public SLS page, not a recorded interview or a claim that she works for the company.
Anika Desai, Technical Director: The first question is what must happen to the part after it arrives. If a technician will snap it over a connector, seat a board, and close a cover on the same shift, the important requirements are not only overall size. They include clip deflection, mating clearances, access to internal powder, and which surfaces must remain sharp. A fast build that cannot be assembled is a slow project. In a responsible SLS conversation, we would identify those interfaces in the drawing before promising a route. The uploaded file starts the discussion; it does not replace a functional specification.
Anika Desai, Technical Director: Loose powder supports most features, so there are usually no printed support trees to remove. That genuinely helps with ducts, enclosed paths, and densely nested batches. But powder still has to leave the finished geometry. Imagine a pneumatic test fixture with a curved internal passage: if the designer closes the only opening, the channel can be difficult to clean even though it printed without supports. We would ask for escape access, realistic cleaning paths, and a decision about whether the interior must be inspected. Design freedom is valuable only when the finished part can be used and verified.
Anika Desai, Technical Director: Because stiffness, impact behavior, and surface expectations pull in different directions. PA12 is a practical starting point for many housings and ducts; PA11 may deserve attention where impact and elongation carry more weight. Glass-filled nylon can make sense for a cover or jig that needs greater stiffness, but its lower elongation is a poor match for a feature expected to flex repeatedly. TPU changes the discussion again when flexibility is central. We would rather ask what the part does at the point of failure than let a material label settle the decision. A stiff sample can still be the wrong sample if the assembly depends on a forgiving snap.
Anika Desai, Technical Director: The quote may omit the work needed to make the part fit its actual job. Someone may need to revise a wall, check a drawing against the mating component, specify tapping, approve a surface treatment, or request a second build after assembly. Those are real engineering hours even when they do not appear in the unit price. Suppose a small production team needs a replacement jig before the next maintenance window: discovering after delivery that a bore needs post-machining can consume more time than the print itself. We try to put critical fit, finish, quantity, and schedule on the table together. The most useful price is the price of a usable part, not merely the first printed object.
Anika Desai, Technical Director: As a planning reference, not a blanket guarantee on every feature. The AIH page gives a typical as-sintered figure of ±0.3 mm or ±0.3%, whichever is greater, and explicitly says the planning values do not replace the live quote. Geometry, cooling, orientation, and finishing can affect an actual fit. For a bracket with a tight locating face, we would want a drawing that marks the critical dimensions and identifies whether a secondary machining step is acceptable. If every dimension is called critical, the design review loses its priorities. State which measurements actually control assembly, then confirm the achievable route for that specific part.
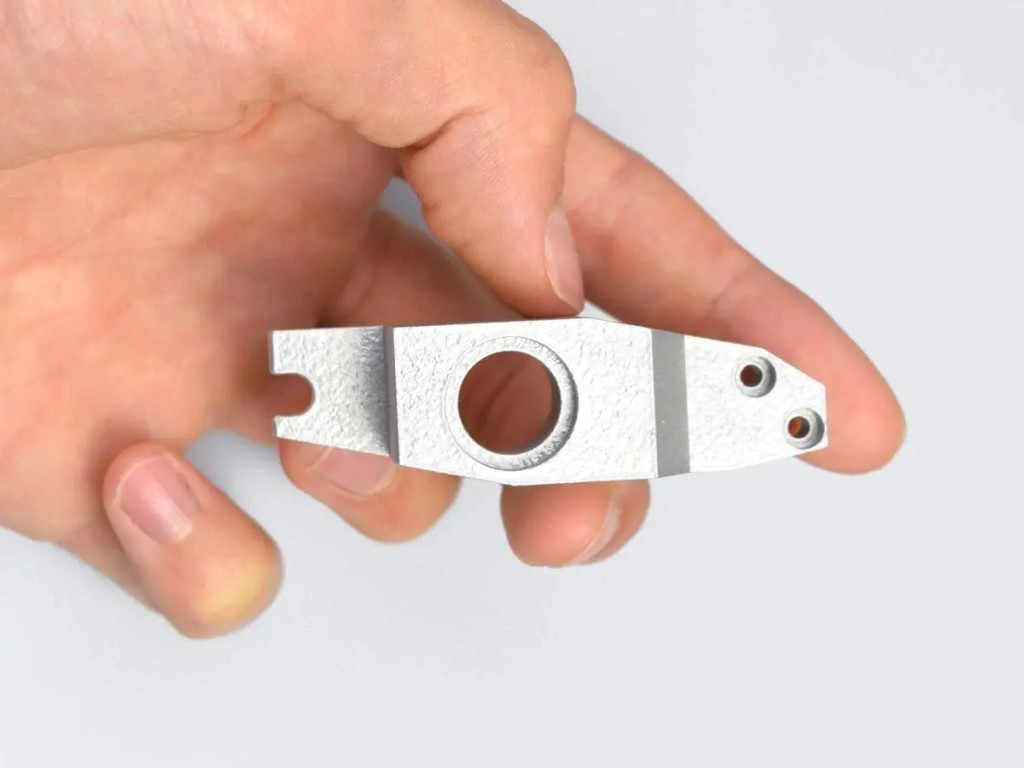
Anika Desai, Technical Director: Not necessarily. As-sintered nylon is typically matte and somewhat grainy; that can be appropriate for a workshop fixture but not for a visible face touched every day. Dyeing, tumbling, or vapor smoothing can change the appearance, and each treatment adds a process decision. The buyer should provide a reference for the surface they expect rather than assume that black means molded-looking. We also need to distinguish an aesthetic edge from a functional one: polishing can soften details that matter to fit. When the surface is part of the user experience, it belongs in the initial specification, not in an email after the part has been printed.
Anika Desai, Technical Director: A file can tell us a great deal about geometry, but it cannot tell us which trade-off the buyer is willing to make. A purchasing lead may see a nominal lead-time option while the engineer needs powder removal verified, a heat-exposed cover reviewed, and a particular bore tapped. The service page lists express timing from 48 hours and other standard tiers; those are routes to discuss, not a substitute for confirming the actual cake schedule and finishing scope. A clean quote should expose assumptions. If the assumptions are wrong, an instant number can create false confidence and transfer the cost of clarification to the shop floor.
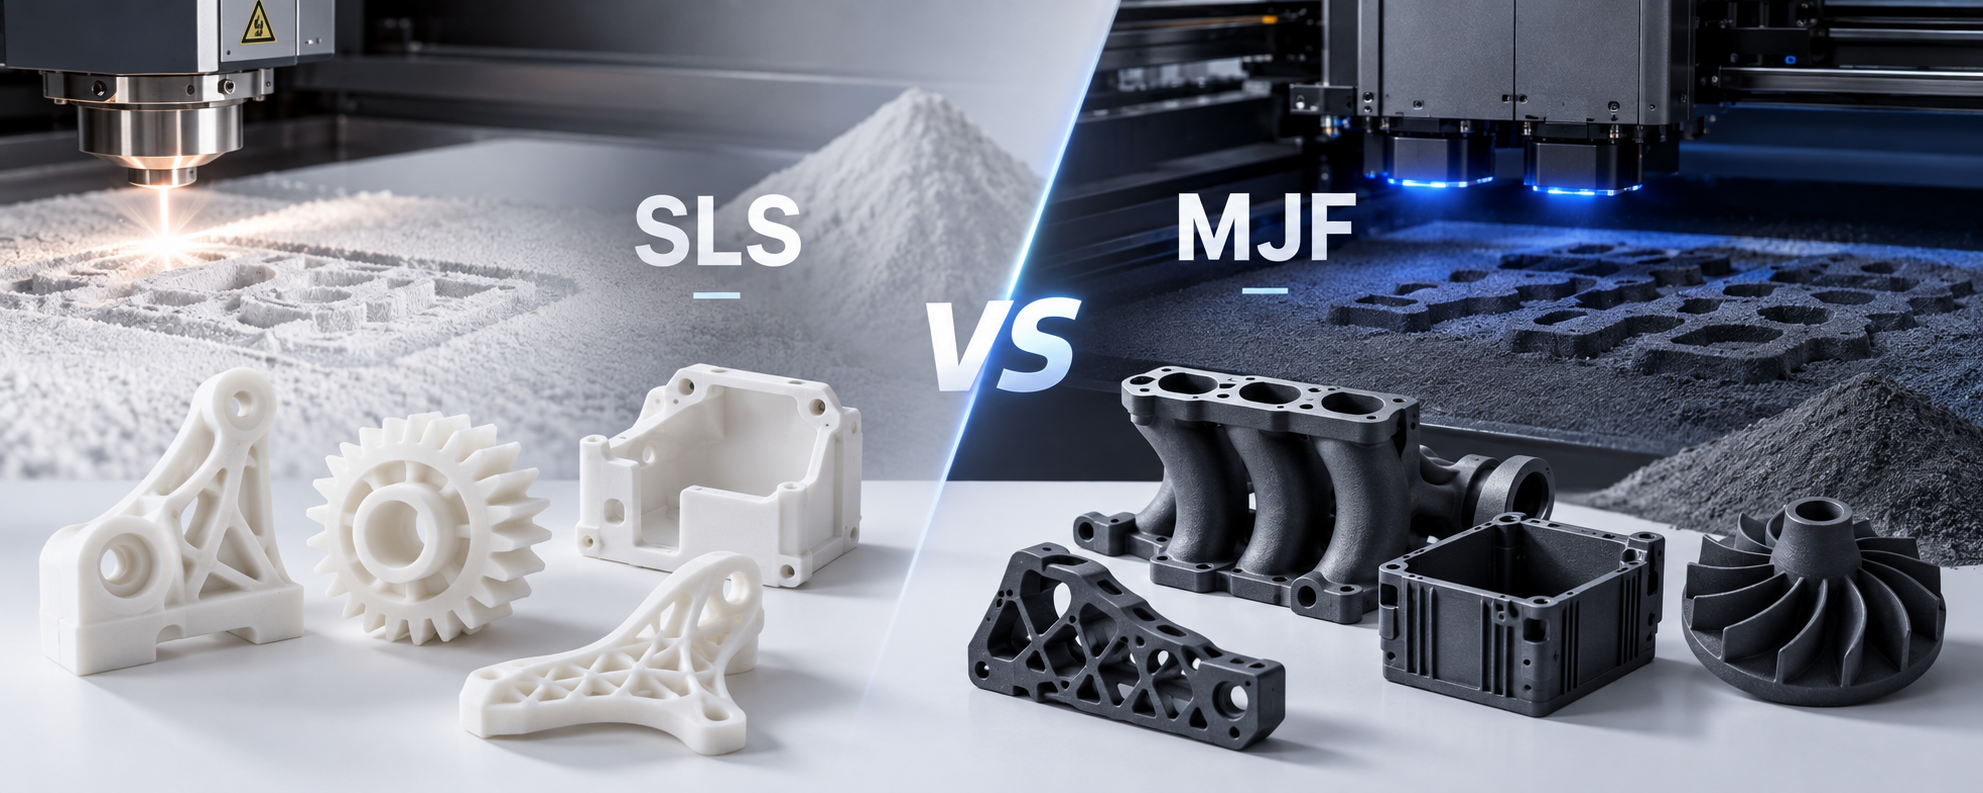
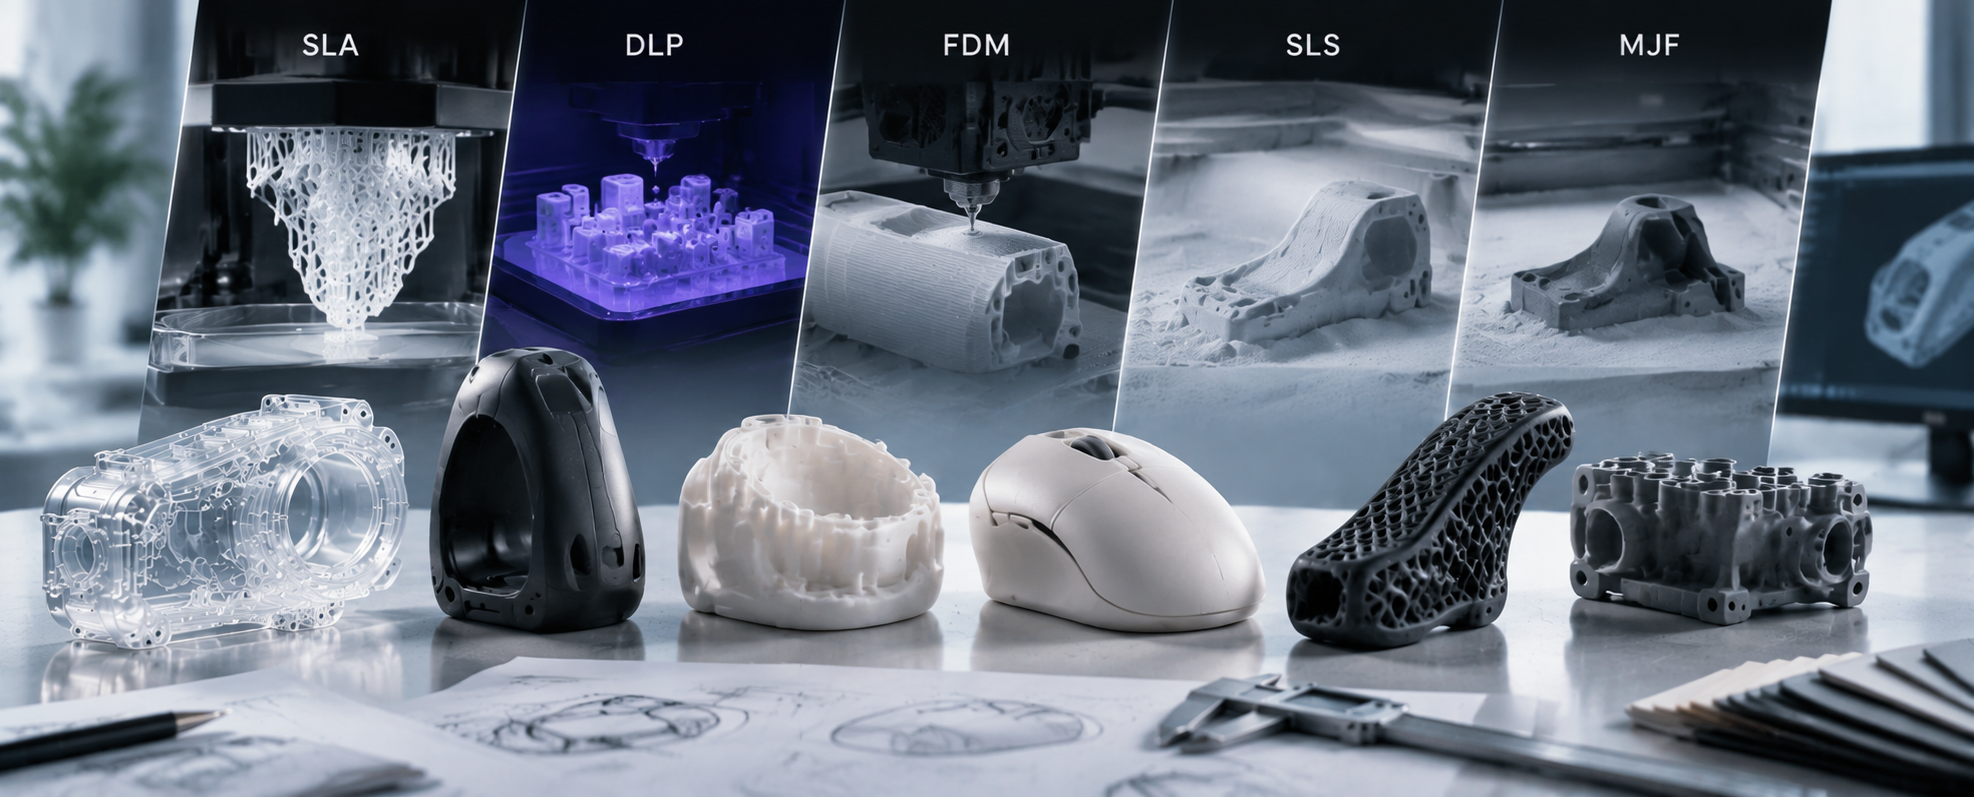
Anika Desai, Technical Director: If the requirement is a highly cosmetic resin-like surface, a different additive process may deserve a look. If a critical interface needs tighter precision, CNC or local machining may be the better route. For dense PA12 batches, MJF can be a sensible alternative; the AIH page itself invites comparison rather than claiming SLS always wins. What matters is the material grade, build size, geometry, finish, and quantity as a combined problem. We should not protect the process choice at the expense of the part. An honest manufacturing recommendation sometimes begins with a reason not to use the first method requested.
Anika Desai, Technical Director: Tell the supplier what must remain true after printing, cleaning, finishing, and assembly. A good drawing distinguishes a cosmetic face from a locating face, a flexible clip from a rigid rib, and an internal passage from an enclosed void. Then a material choice or finishing choice can be evaluated against the job rather than against a generic sample. We would rather challenge a file early than celebrate an impressive print that fails at the workbench. The strongest process decision is the one that makes the next engineering decision easier, with fewer surprises for the people who actually use the part.
Desai’s final point brings the conversation back to the workbench, where process claims meet assembly reality. The exchange closes on a simple principle: define the job of the finished part before treating print speed or material names as answers. That leaves a clearer basis for the final manufacturing decision.
A useful SLS decision starts with what the finished part must do, not with the ability to print it. AIH’s public guidance on materials, powder removal, tolerance, finishing, and alternative processes provides a starting vocabulary for that discussion. For buyers, the practical next step is to mark critical interfaces and performance needs on the drawing, then confirm the material, post-processing, and schedule against the actual build. That is how a quick quote can become an informed manufacturing choice rather than an attractive number with unresolved work behind it.
This post was reproduced from: Industry Savant — When Nylon Parts Have to Survive
A process that fits this note. Open the spec, or put the file on a quote.
AIHFABS SLS 3D printing services fuse engineering-grade SLS plastics into durable, self-supporting parts.
Create a quote
Large Part CNC Machining is a professional manufacturing service that uses large-scale, dedicated CNC machine tools to cut workpieces that exceed the size or weight capacity of conventional equipment.
Create a quoteMaterials that sit next to this article. Check the card, then upload CAD.
Process, finish, and file notes from the shop — not a marketing blog.
Company, payment, shipping, and process answers by topic.
Questions about 3D printing processes, materials, MOQ, samples, and custom projects.
Review AIH commitments to print quality, secure handling of your files, transparent pricing, and support for every 3D printing order.
AIHFABS quotes custom 3D printing and CNC machining from a CAD upload. Compare SLA, SLS, MJF, SLM, FDM, DLP, milling, and turning, then add finishing such as vapor smoothing, dyeing, anodizing, polishing, or powder coating in the same order.
Instant quoting is built for prototypes, jigs, housings, and small-batch production. You see material, process, quantity, and lead time together, which keeps engineering changes from turning into a new round of supplier emails.
You can review material, process, quantity, and lead time together, so engineering changes do not turn into another round of supplier emails.
Upload STL, STEP, and other common CAD formats for an online quote.
Compare 3D printing technologies and CNC options on the same part.
Select polymers or metals, then add 3D Plus hardware finishing when needed.
Review price and lead time before checkout, or request a manual quote for special specs.
If this page describes a process, industry, or sample part you want to reproduce, start from the upload flow and match technology plus finishing to your drawing.
We use cookies to personalize your experience. By using this site, you agree to our Privacy Policy
Accept
Leave A Comment