Lead Time
From 48 hours for standard resin jobs

3D Printing
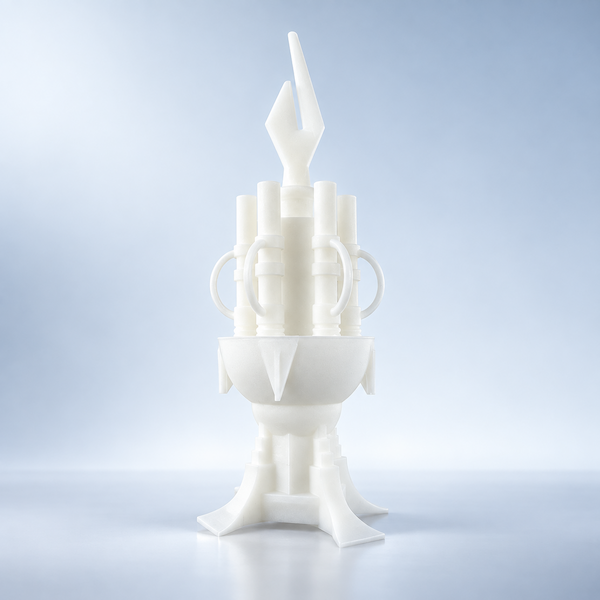
Ultra-smooth resin parts with fine feature resolution — show models, master patterns, and clear prototypes.
Stereolithography (SLA) cures liquid photopolymer with a precision UV laser, building parts layer by layer. SLA excels when surface quality, small features, and dimensional accuracy matter more than rugged thermoplastic performance. Plan around ±0.2 mm on well-supported features and from 48 hours on standard resin — the live quote after CAD upload is the source of truth.
Check SLA capabilities, pick a resin, then upload STL or STEP. Compare DLP or LCD for faster full-layer resin, SLS nylon for shop handling, and 3D Plus finishing for paint or clear coat.
Stereolithography draws each slice with a UV laser in a vat of liquid resin. The cured layer bonds to the one below, which is why SLA parts look closer to a molded show model than to a filament print.
AIHFABS uses SLA when edges, lettering, and smooth skins matter more than rugged nylon toughness. Supports touch the part, so cosmetic faces should be called out before we orient the build.
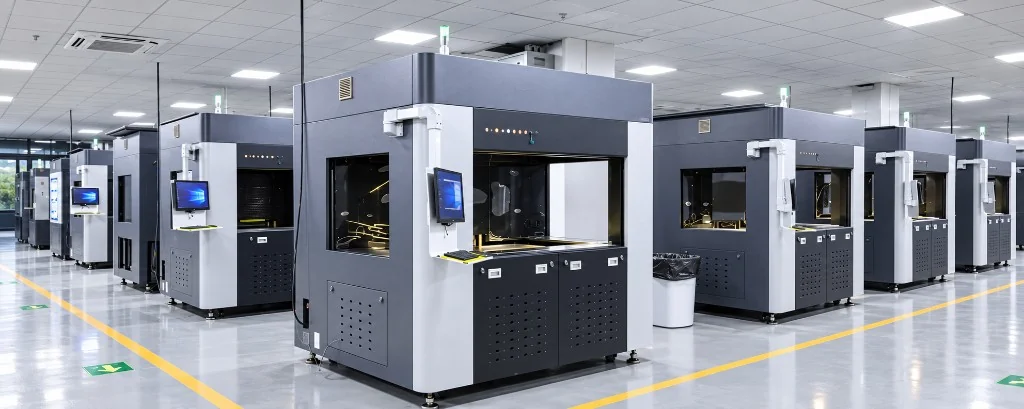
Fine layers and a large platform are available; the live quote still depends on orientation and resin.
From 48 hours for standard resin jobs
±0.2 mm on well-supported features
Platform up to 800 × 800 × 550 mm (job dependent)
Fine layers for smooth curvature; balanced modes for speed
Required; contact points can be placed on non-cosmetic faces
Standard, tough, high-temp, clear, flexible, and castable photopolymers. Catalog names open on the materials page.
Washed and UV post-cured is the default. Clear coat or paint is the usual visual upgrade.
Support nubs dressed off. Smooth, slightly glossy resin skin — the usual prototype deliverable.
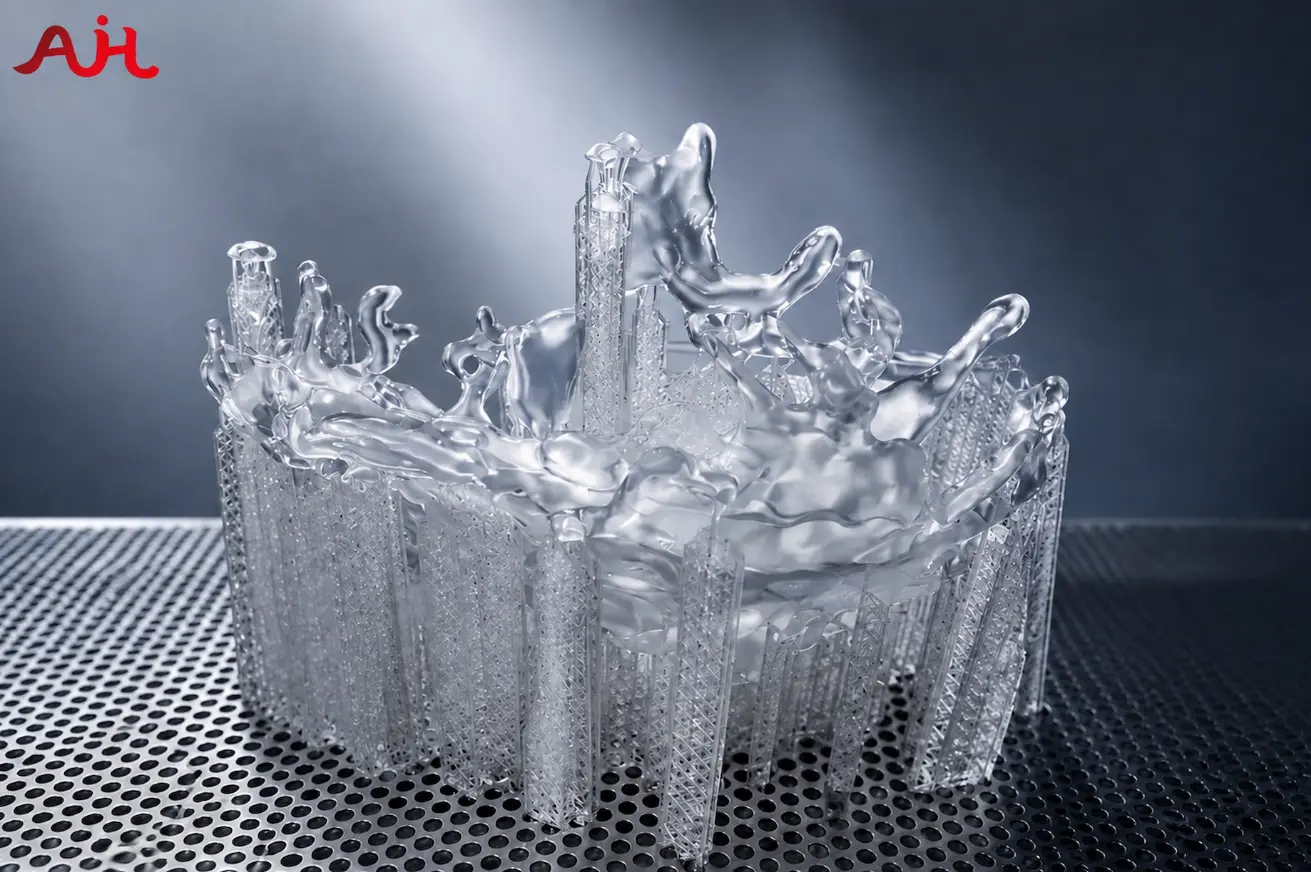
Clear or tinted coat on transparent grades to even the surface and protect edges.
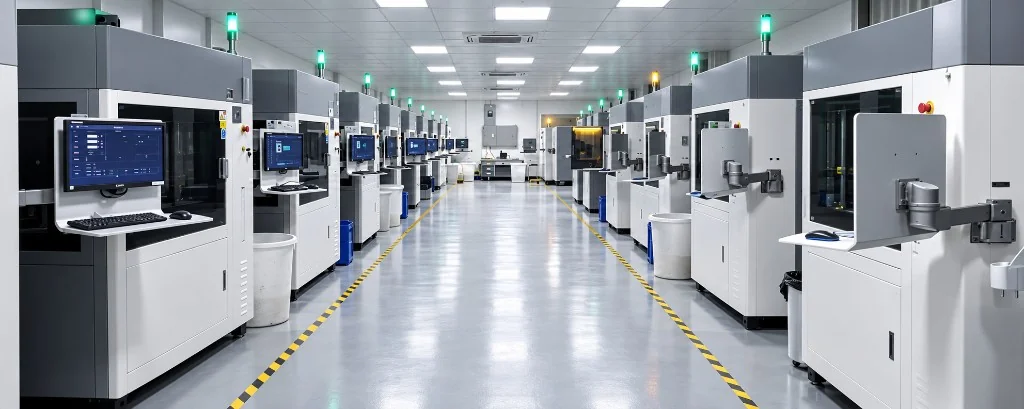
Primed and painted show models, or dyed accents, when the review needs a product-like color.
SLA is the laser-resin option. DLP and LCD expose a full layer at once; SLS/MJF skip supports on nylon.
| Process | Lead time | Tolerance | Pricing |
|---|---|---|---|
| Selective Laser Melting (SLM)Metal | From 5 business days (express options where available) | ±0.3 mm or ±0.3% (whichever is greater), tighter after machining | Instant quote · typical metal part from $90 |
| Stereolithography (SLA)Resin | Quoted with your CAD upload | Instant quote · typical resin part from $18 | |
| Digital Light Processing (DLP)Resin | From 48 hours | ±0.2 mm on supported geometry | Instant quote · typical resin batch from $20 |
| Liquid Crystal Display (LCD)Resin | From 48 hours | ±0.2 mm on supported geometry | Instant quote · typical resin part from $16 |
| Selective Laser Sintering (SLS)Plastic powder | From 48 hours express; 72 hours / 5 days standard tiers | ±0.3 mm or ±0.3% | Instant quote · typical nylon part from $28 |
| Multi Jet Fusion (MJF)Plastic powder | From 48 hours express; standard 72 hours / 5 days | ±0.3 mm or ±0.3% | Instant quote · typical PA12 part from $25 |
| Fused Deposition Modeling (FDM)Thermoplastic filament | From 24–48 hours depending on size | ±0.5 mm or ±0.5% on FDM-appropriate geometry | Instant quote · typical prototype from $12 |
The model is sliced and oriented to minimize support contact on cosmetic surfaces.
A UV laser draws each layer on the resin surface, curing it to the previous layer.
Supports stabilize islands and overhangs during the build, preferably on B-side faces.
Parts are washed, UV post-cured, and supports removed before optional clear coat or painting.
Orientation hides supports on B-side faces when you mark cosmetics. Drain holes are added or requested on hollow show parts.
Parts are washed, UV post-cured, and support-removed before any coat. Resin choice follows heat, clarity, and handling notes on the RFQ.
Resin has a minimum wall. Hollow parts need a way for liquid to leave.
| Feature | Recommended practice |
|---|---|
| Walls | Stay above the resin’s minimum wall so shells do not print incomplete or brittle. |
| Drain Holes | Add drains on hollow cosmetic parts so uncured resin can escape. |
| Cosmetic Faces | Mark A-sides so supports can sit on the back of the model. |
| Fine Text | Raised or engraved text should stay above the layer and laser spot size. |
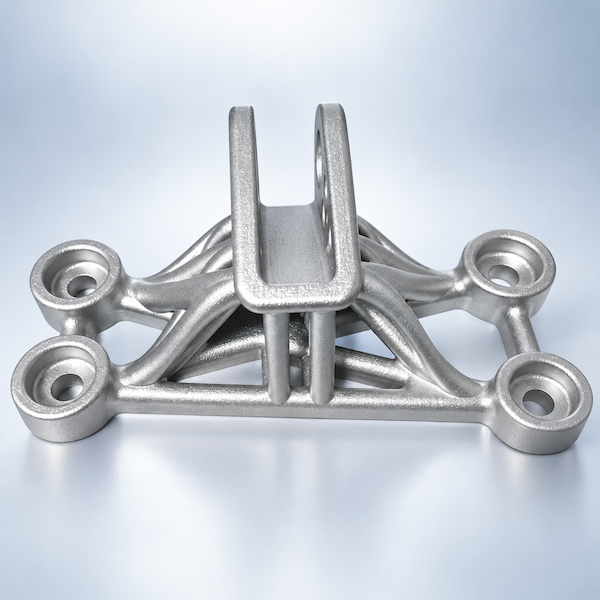
Selective Laser Melting (SLM) is a powder-bed metal additive process. A high-power laser scans each cross-section of your CAD model, melting metal powder that solidifies into a dense part.
Full process details
Digital Light Processing (DLP) solidifies an entire layer of photopolymer at once using a projected image.
Full process details
Liquid Crystal Display (LCD) printing — also called MSLA — cures a full layer of photopolymer at once.
Full process detailsWhen surface quality, small text, or a show-model finish matters more than impact toughness or raw cost.
Yes, on clear and translucent resins. A clear coat is usually needed for a lens-like look.
About ±0.2 mm on well-supported features. Large spans and thin unsupported walls wander more.
Yes. We place them on non-cosmetic faces when you mark the show side.
Standard resin jobs often leave from 48 hours after the file is approved.
AIHFABS quotes custom 3D printing and CNC machining from a CAD upload. Compare SLA, SLS, MJF, SLM, FDM, DLP, milling, and turning, then add finishing such as vapor smoothing, dyeing, anodizing, polishing, or powder coating in the same order.
Instant quoting is built for prototypes, jigs, housings, and small-batch production. You see material, process, quantity, and lead time together, which keeps engineering changes from turning into a new round of supplier emails.
You can review material, process, quantity, and lead time together, so engineering changes do not turn into another round of supplier emails.
Upload STL, STEP, and other common CAD formats for an online quote.
Compare 3D printing technologies and CNC options on the same part.
Select polymers or metals, then add 3D Plus hardware finishing when needed.
Review price and lead time before checkout, or request a manual quote for special specs.
If this page describes a process, industry, or sample part you want to reproduce, start from the upload flow and match technology plus finishing to your drawing.
We use cookies to personalize your experience. By using this site, you agree to our Privacy Policy
Accept