
CNC Machining
CNC Machining Services
CNC machining removes material from solid stock with computer-controlled mills, lathes, and multi-axis centers.
Create a quote
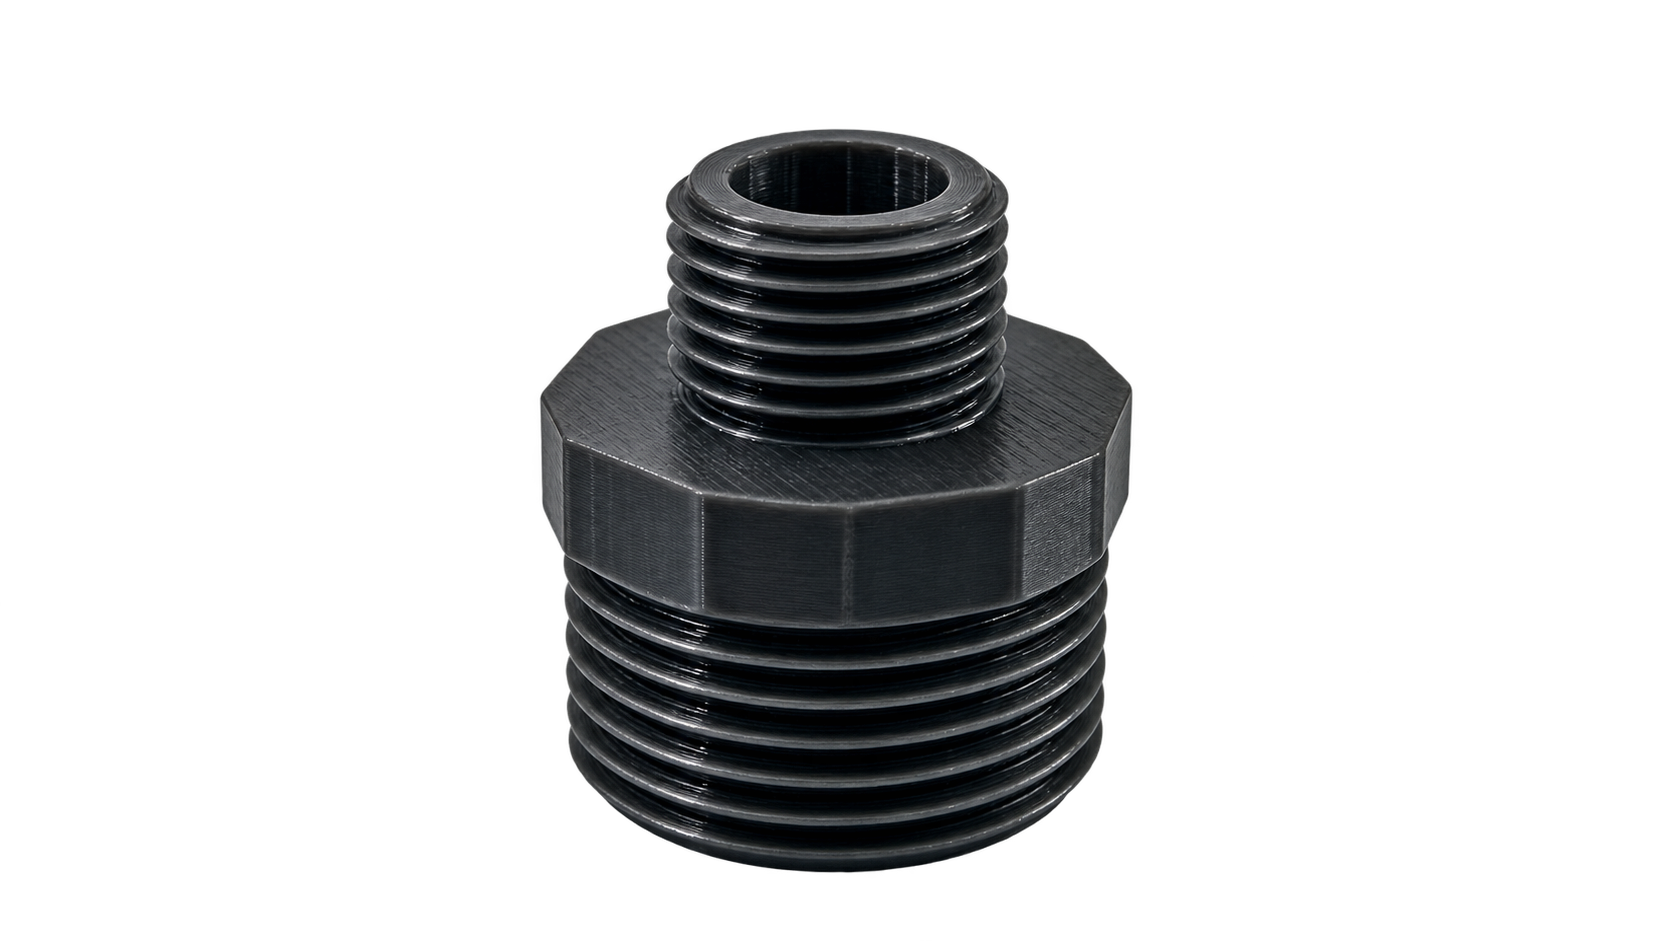
This case study demonstrates the successful application of FDM 3D printing with ABS for rapid production of functional fluid connectors. Through DFM strategies—including optimized support structures, heated bed enclosure, and acetone vapor smoothing— the project achieved a 70% reduction in prototyping costs, 60% faster production compared to CNC machining, and ±0.1mm thread accuracy for pressure-resistant connectors. The study addresses ABS-specific challenges such as warping and post-processing
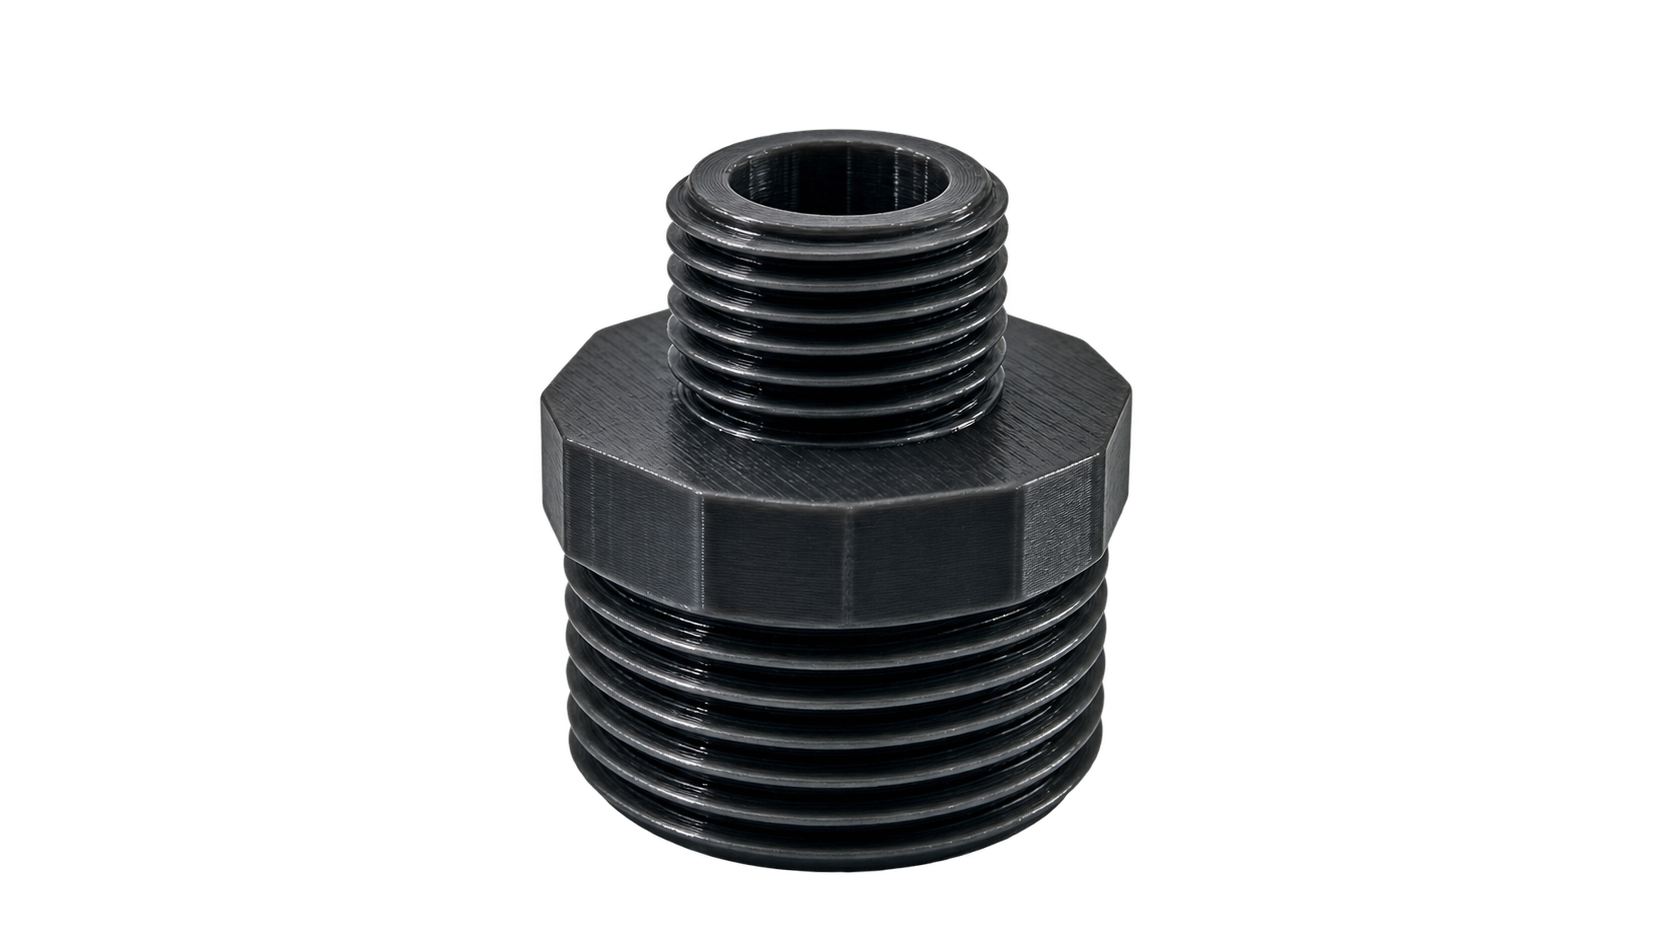
A industrial equipment manufacturer needed to prototype high-strength fluid connectors for a new hydraulic system. Traditional CNC machining was too expensive ($50–$80 per unit) and slow (2-week lead time) for iterative testing. The team required a solution that could produce durable, pressure-resistant connectors quickly, at low cost, and with minimal post-processing—while meeting strict mechanical performance standards.
The team adopted acrylonitrile butadiene styrene (ABS) via FDM 3D printing for its toughness, heat resistance, and ability to withstand mechanical stress. Key steps included:
1. Design for Manufacturability (DFM): Engineers redesigned connector geometries to minimize overhangs (e.g., thread profiles, hexagonal grips) and used sparse support structures only for critical overhangs. This reduced material waste and post-processing time by 40%.
2. Rapid Prototyping Workflow: Desktop FDM printers produced batches of connectors in 6–8 hours per batch—60% faster than CNC machining. Layer heights of 0.15–0.2mm ensured smooth thread surfaces for leak-proof sealing.
3. Cost Efficiency: ABS filament costs ~$25/kg, and print times were optimized via 20% infill density. Per-unit cost dropped to $3–$5, compared to $50–$80 for CNC-machined metal prototypes.
ABS is prone to warping during printing, which risked dimensional inaccuracies in thread profiles. Solutions included:
• Heated Bed & Enclosure: Using a 100°C heated bed and enclosed print chamber reduced warping by 80%, ensuring ±0.1mm thread accuracy.
• Support Removal: Customized deburring tools and acetone vapor smoothing (for critical surfaces) minimized post-processing time while maintaining thread integrity.
• Material Validation: Testing ABS+ (a reinforced variant) for high-pressure applications confirmed it could withstand 150 PSI without deformation.
• Speed: Prototype turnaround time reduced from 2 weeks to 48 hours, enabling same-day design revisions.
• Cost Savings: Annual prototyping costs dropped by 70% ($24,000 → $7,200) due to cheaper materials and faster production.
• Performance: Connectors passed 100-hour pressure tests (150 PSI) with zero leaks, meeting client specifications for functional testing.
Title: “Strong, Fast, Affordable: ABS 3D Printing for Functional Prototypes”
• Durability: ABS withstands mechanical stress, heat (up to 100°C), and pressure (150+ PSI).
• Cost: Low material costs ($25/kg ABS) and efficient printing reduce per-unit expenses to $3–$5.
• Precision: Achieve ±0.1mm accuracy for critical features (e.g., threads, seals).
• Versatility: Ideal for fluid systems, automotive parts, and industrial fixtures.
• Superior toughness vs. PLA: Perfect for functional prototypes requiring strength.
• DFM-friendly: Optimize supports and geometries to minimize warping and post-processing.
• Heat resistance: Suitable for high-temperature environments (e.g., engine components).
Our DFM guidelines ensure smooth, functional surfaces:
• Use heated beds (100°C) and enclosures to prevent warping.
• Print with 0.15–0.2mm layers for smooth thread finishes.
• Leverage acetone vapor smoothing for critical sealing surfaces.
3D printing and CNC on the same quote. Open a process, then upload CAD.
CNC machining removes material from solid stock with computer-controlled mills, lathes, and multi-axis centers.
Create a quote
CNC Milling Services use computer numerical control (CNC) mills to cut workpieces with rotating tools according to programmed toolpaths.
Create a quote
CNC Turning Services use computer numerical control lathes to remove material while the workpiece rotates at high speed and the cutting tool feeds along a set path.
Create a quote
CNC Routing Services use computer numerical control (CNC) routers with high-speed rotating bits to cut, engrave, drill, and shape materials.
Create a quoteResins, nylons, metals, and more. Each card jumps to the catalog row.
Process, finish, and file notes from the shop — not a marketing blog.
Company, payment, shipping, and process answers by topic.
Recommended answers about AIHFABS, technologies, materials, pricing, privacy, and file preparation.
Questions about 3D printing processes, materials, MOQ, samples, and custom projects.
Production lead times, shipping options, and order tracking.
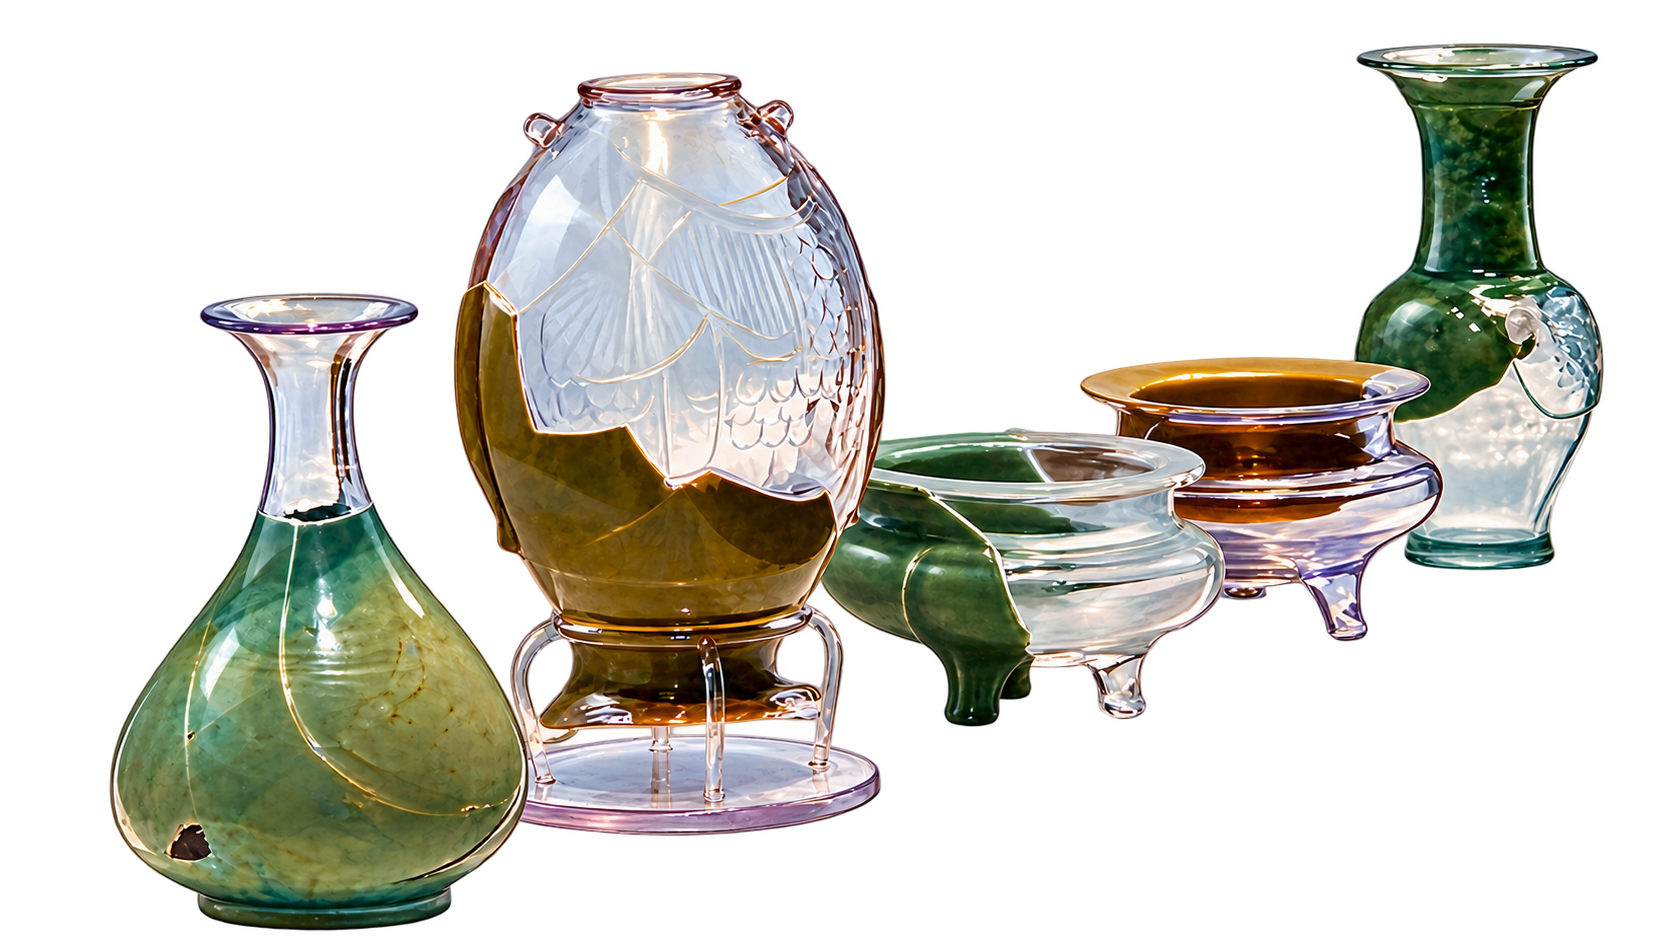
This case study highlights the innovative application of SLA stereolithography with Premium Clear Resin for the restoration and replication of fragmented historical artifacts in museum collections. Leveraging the material’s exceptional transparency, ultra-smooth surface finish, and high detail resolution, the project enabled conservators to recreate missing components of fragile antique glassware and ceramic pieces with optical-grade clarity. The approach demonstrates how clear resin 3D printing
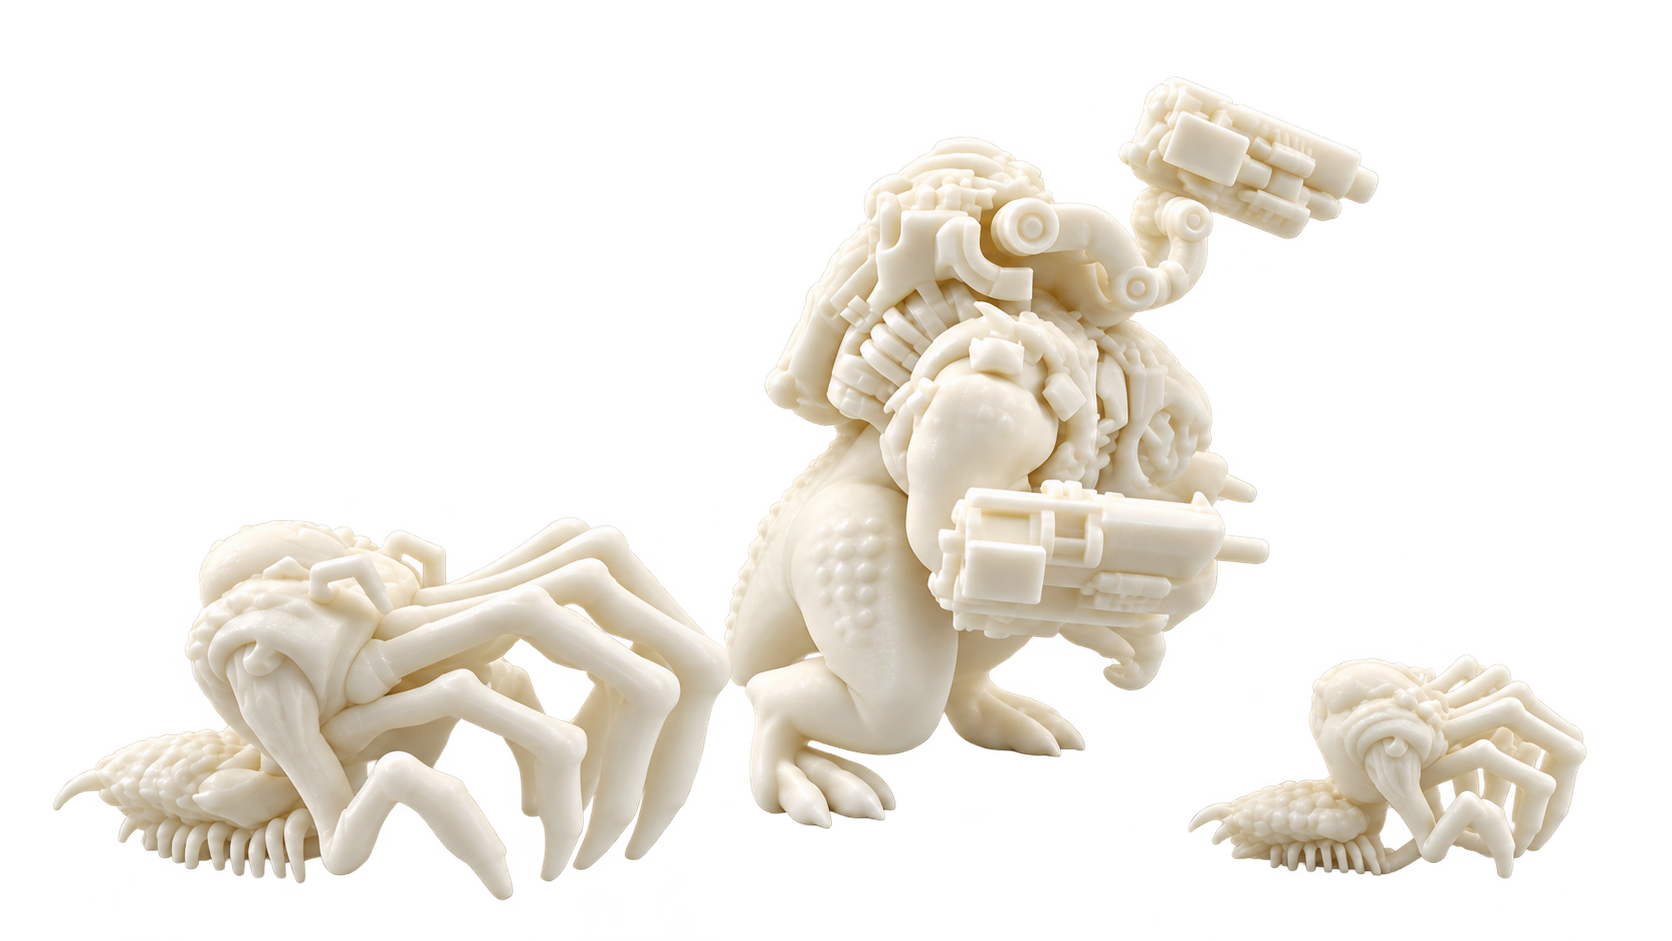
This case study highlights the successful application of SLA stereolithography with white resin for producing high-detail decorative display models. Leveraging the material's ultra-smooth surface finish, zero visible support marks, and cost-effective pricing, the project delivered presentation-grade figurines with exceptional dimensional accuracy and rapid turnaround. The approach demonstrates why white resin remains the premier choice for visual and collectible parts where surface quality and a
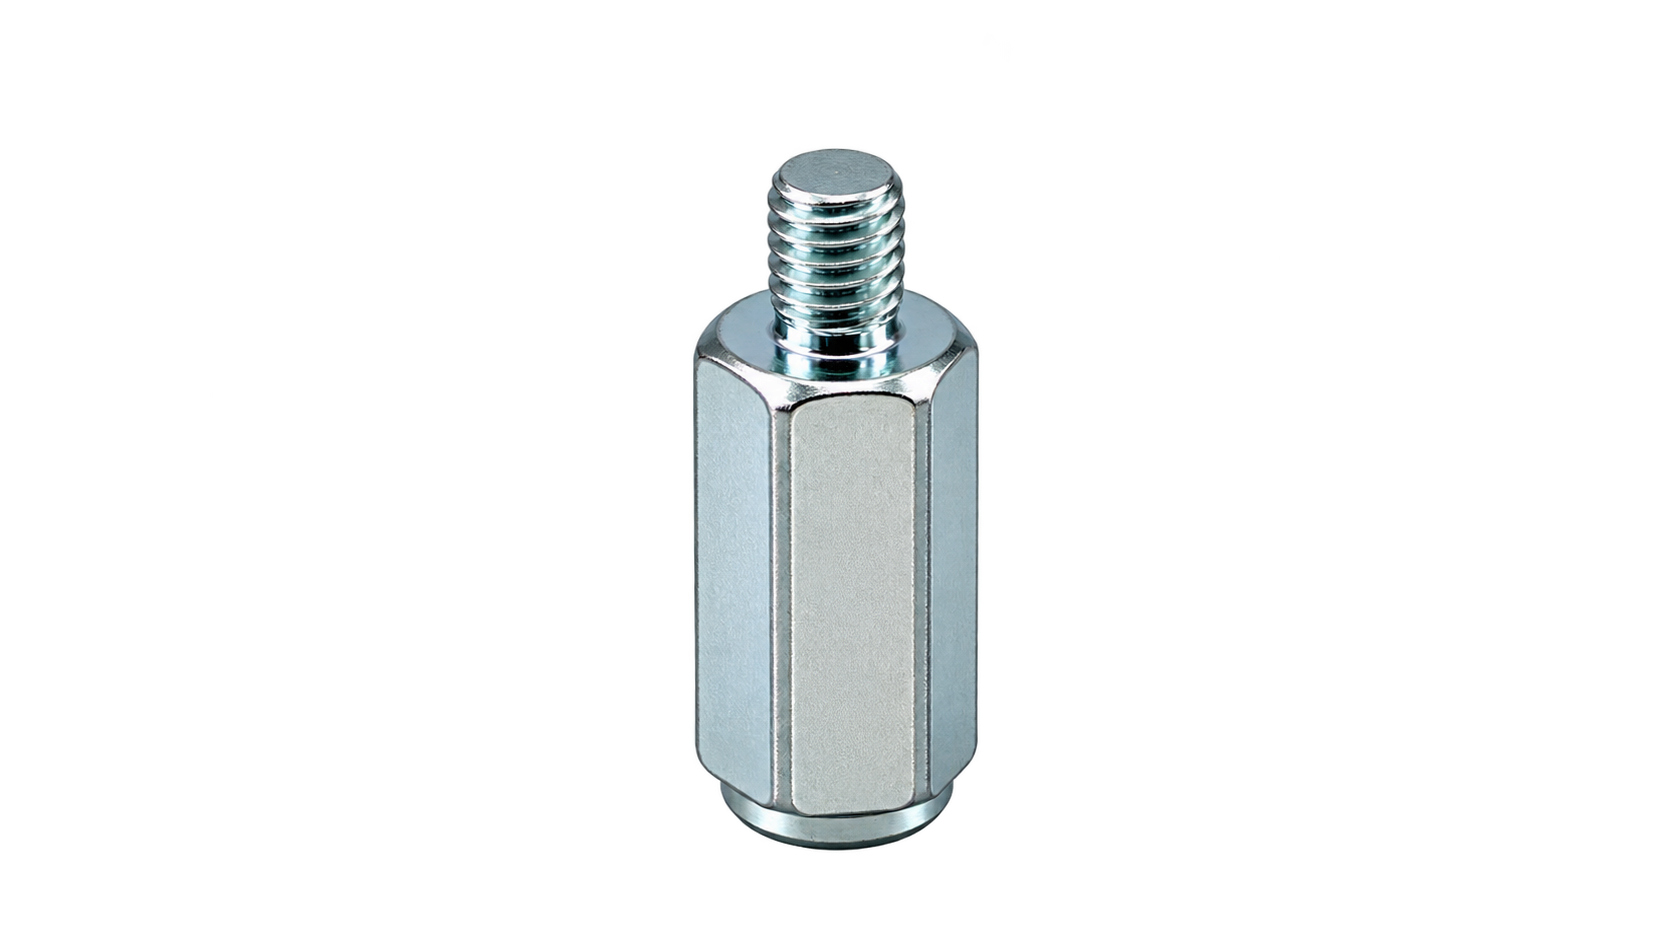
This case study demonstrates the successful application of SLM metal 3D printing with metal materials for rapid production of high-strength functional metal bolts. Through DFM strategies — including optimized build orientation, strategic support design, and post-processing workflows — the project achieved a 55% reduction in prototyping costs, 60% faster production compared to CNC machining, and ±0.3mm dimensional accuracy for precision-threaded metal fasteners. The study addresses SLM-specific c
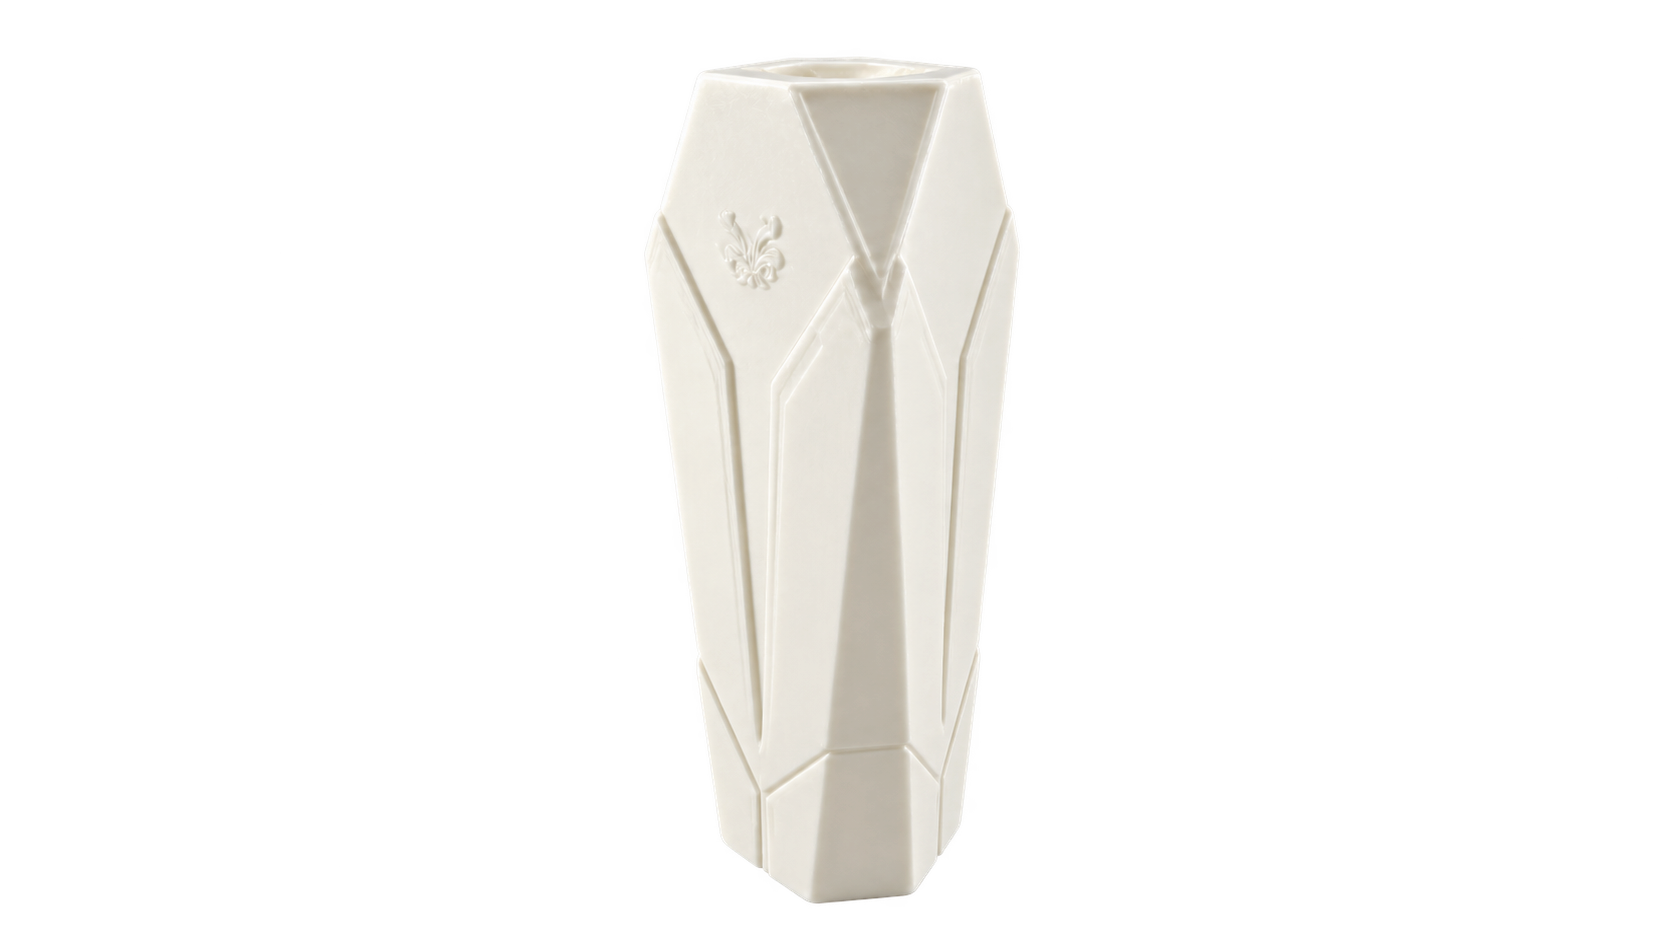
This case study demonstrates the successful application of FDM 3D printing with PLA for rapid production of Mandel bricks — popular game props beloved by children. Through DFM strategies including optimized support structures, safe non-toxic material selection, and colorful post-processing, the project achieved significant cost reduction compared to traditional manufacturing, fast turnaround for custom designs, and child-safe, smooth-finish products. The study addresses PLA-specific consideratio
We use cookies to personalize your experience. By using this site, you agree to our Privacy Policy
Accept