

Silicone Mold Vacuum Casting
Detailed polyurethane replicas for development and small batches.
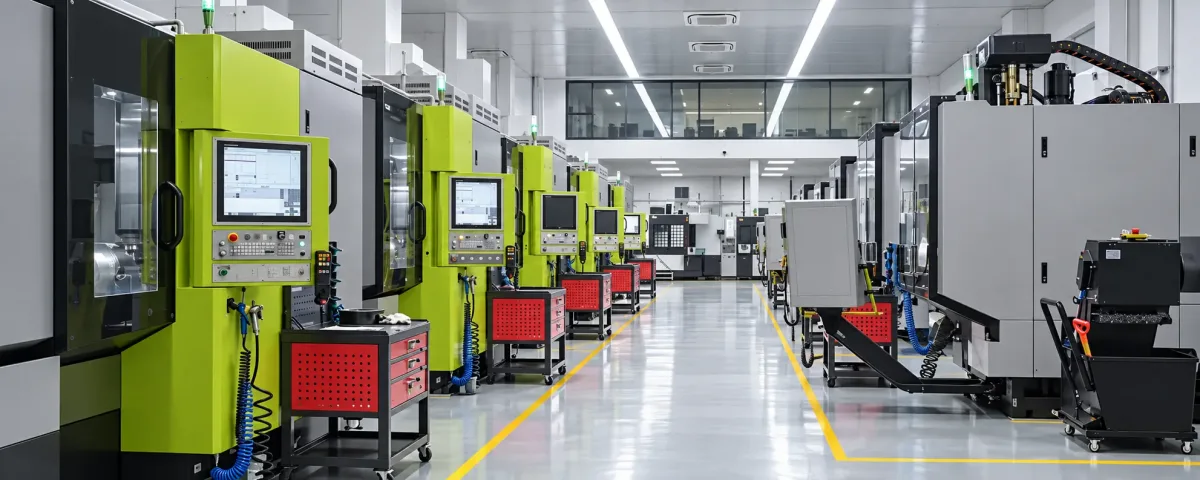
A finished master defines the surface and geometry of a flexible silicone mold. Mixed resin is introduced under vacuum to reduce trapped air, then cured and demolded. Silicone is the tooling material; the finished part is usually polyurethane unless another casting system is agreed. This process supports appearance models and assembly trials before committing to production tooling.
How it works
Approve the master pattern and define mold split lines.
Make silicone tooling with suitable gates and vents.
Cast the chosen resin under controlled vacuum and curing conditions.
Demold, trim and inspect representative samples.
Materials
Confirm material grade, critical dimensions, quantity and inspection requirements before production.
Silicone makes the mold. The finished replica is normally polyurethane (PU) resin, formulated to resemble selected properties of engineering plastics or elastomers. These are candidate resin families, not a promise that every formulation is available. Confirm the actual product data sheet and sample requirements before ordering.
MaterialsDesign guidelines
Define cosmetic faces and acceptable gate and parting-line marks.
Check resin data for temperature, UV exposure and load; appearance alone does not prove functional equivalence.
Agree mold life and batch consistency because flexible tooling wears with use.
Specifications
- Tolerance
- Agreed after drawing review
- Lead time
- Quoted after geometry and tooling review
Advantages
- Geometry and process review before tooling
- Sample approval before repeat manufacture
Applications
- Prototype enclosures and covers
- Assembly and product development
Silicone molds wear with repeated use. Approve a sample and agree the expected mold life before ordering a batch.
Related services
Materials by industry
Review application requirements before choosing a grade or manufacturing route.

Aerospace
TitaniumHigh specific strength for brackets and interfaces; review fatigue, build orientation, heat treatment and traceability before flight use.

Medical devices
Stainless steelInstrument hardware and fixtures; select grade against corrosion, sterilization cycles and passivation requirements.

Automotive
AluminumLightweight housings and development brackets; assess vibration, thermal expansion and threaded joint durability.

Robotics
Nylon PA12Grippers and cable guides; evaluate creep, moisture and repeated flexing.

Communication
CopperThermal and electrical interfaces; review oxidation protection and contact resistance.

Electronics
ABSPrototype housings; ordinary ABS does not establish ESD protection or a flammability rating.

Energy
CopperConductive and thermal parts; specify contact geometry, plating and temperature rise criteria.

Semiconductor
PEEKInsulating fixture components; verify outgassing, chemical compatibility and particle generation for the process.

Consumer goods
ABSAppearance prototypes and housings; approve texture, color and assembly before tooling.